
Kaizen Success Stories
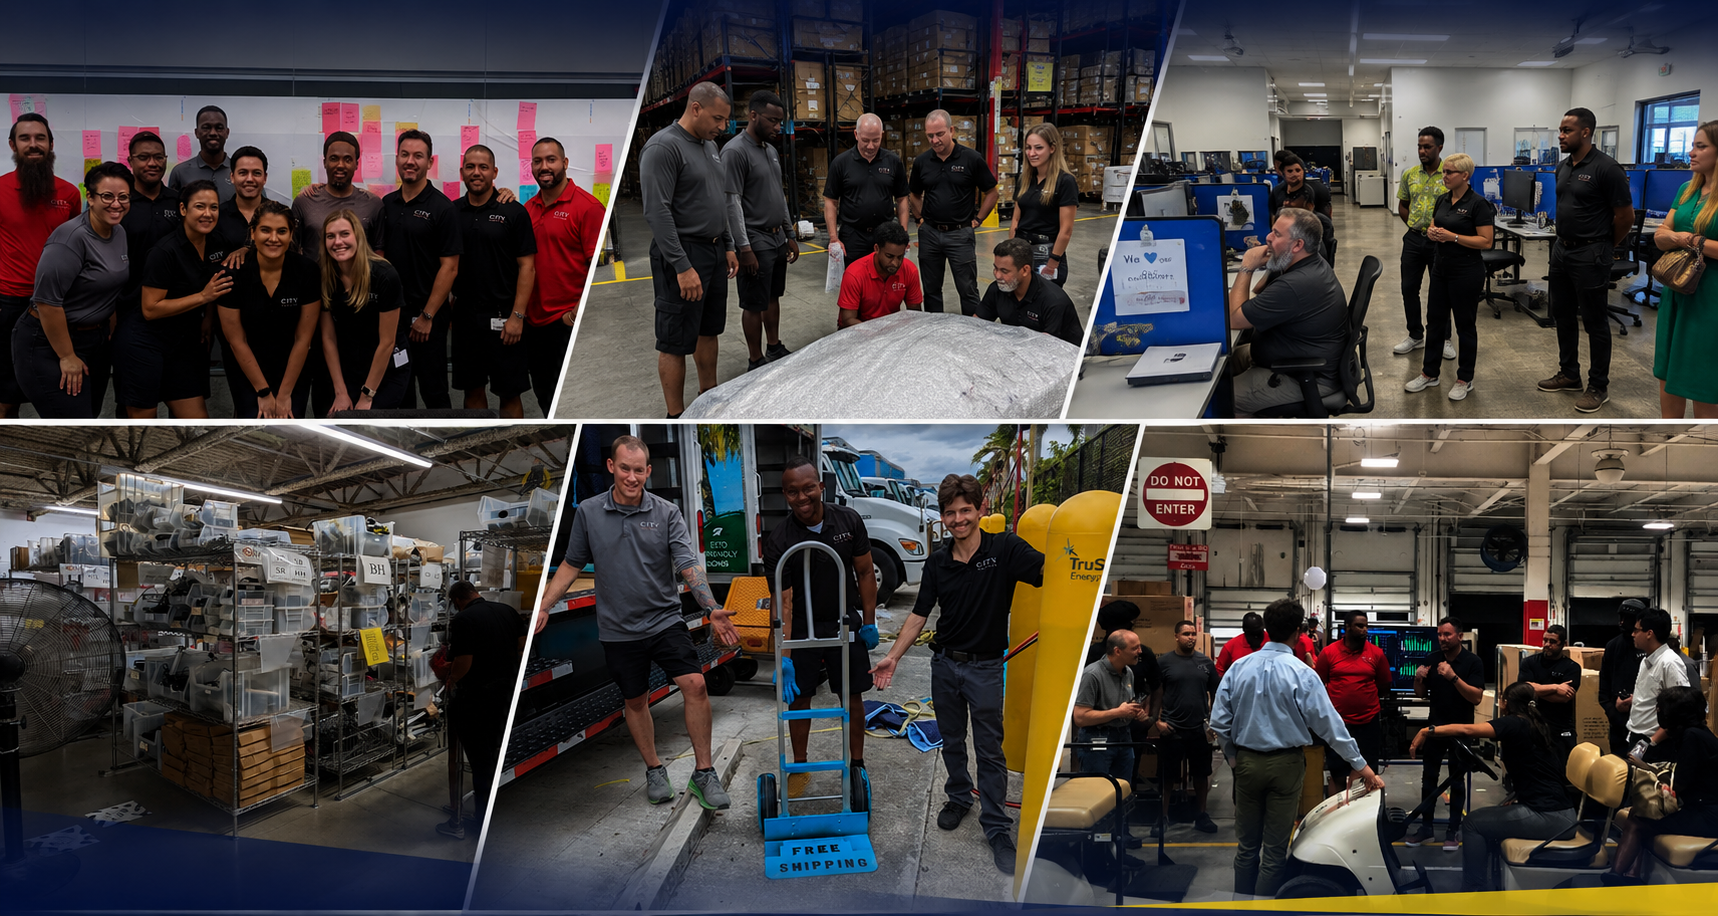
Real Manufacturing Results. One Kaizen at a Time
Explore real-world Kaizen success stories showing how manufacturing teams solved critical problems, improved performance, and created sustainable results.

Little Things Mean A Lot
A global consumer goods manufacturer was experiencing high levels of downtime, jams, and long changeovers on a critical production line. They invited Process Improvement Partners to their plant to observe and discuss the problem and identify opportunities for improvement. After reviewing performance, we took a walk to the line. The line was running, and after a description of line components, it became apparent there were quick opportunities to improve performance of the line. The techniques we would use were quite basic: leveling, squaring, aligning, and centering of products with the process. It seemed so simple, and the customers were skeptical. We suggested a five-day Kaizen to improve line reliability, scheduled for January 2019.

Where Is It?
In 2010, the company I used to work for decided to go Lean. They brought in consultants, who taught tools and techniques to employees all over the world. One tool I learned from them was 3P - Production Preparation Process. This technique maximizes creativity of a team by driving their thinking way beyond their comfort level.

Lead from the Front – The Story of the Pink Tools
A large, multi-national company started their Lean journey in 2010. The company brought in consultants, who facilitated and guided Kaizen events and coached leaders at every manufacturing site around the world. One of their plants, in central Ohio, had a strong culture of employee engagement and was expected to lead the other plants in positive outcomes resulting from the Kaizen events. Early on, they weren’t able to identify an internal leader of their continuous improvement journey, so I was asked to act as the interim “Lean Champion” for the plant.

Even the Most Organized Person Can Improve
A global ceilings manufacturer wanted to improve the safety and productivity of its testing facility. Over the years, many capabilities had been added to the facility without regard to the needs of the technicians who worked there. Because of this and the lack of a managing system to ensure the organization and productivity of the facility, the technicians took it upon themselves to hold an annual “cleanup week” at the end of the year. All technicians would stop their project work and devote their time to go through equipment, materials, and spaces and clean out any clutter they felt they could get rid of.

A Tasty Breakthrough
A North American ceilings manufacturer was closing a plant that produced a product no other plant in the division could manufacture, due to specialized, but obsolete technology. They had a customer who was buying millions of square feet of this product annually. They knew they had to come up with an alternative the customer would approve of and keep buying after the old plant was closed.

Top 5 Continuous Improvement Books
I have read many books on Lean, Six Sigma, and other Continuous Improvement methods over the years. Some inspired me, some frustrated me, and all made me think. The following 5 (and two honorable mentions) are my all-time favorites.

PIP Visits Dogfish Head Brewery
One of the benefits of being in business for yourself is to decide what’s most important to you and then prioritize your time to let you do what you are most passionate about.

From Russia with Love: The Spirit of Kaizen Lives in All of Us
A Russian ceilings manufacturing plant asked me to help them facilitate their strategic road map in 2017. This was an activity they did annually since the plant opened in 2015. I had been to Russia one time before, during construction of the plant, so I had some experience travelling there and working with the people. This time, I would be coaching their continuous improvement leader in how to organize and facilitate this important session.

PIP Helps Team in York, PA Improve Reliability of Critical Operation
Many consultants train and teach. I like to demonstrate and verify with teams that they truly understand the techniques for improvement that I am sharing with them. Most importantly, I want them to be able to take this work and transfer it to other parts of the factory without my assistance.

Listen To Your People, People
A Research and Development team wanted to create a three-year strategic plan. Their goal was to reduce the time it takes from a new product idea to launch of the new product. Many of the team members believed “you can’t schedule invention.” Working with the team leader, the Research and Development Director, we decided to focus on the work leading up to and supporting the invention, even if we couldn’t specify when an invention would occur. We agreed to use Value Stream Mapping as the approach to help the team accomplish their goals.

350 Business Owners
An engineered flooring plant in Kentucky was losing money. They knew their product yields were deteriorating and didn’t know what to do about it. Process Improvement Partners was invited for a site visit. After reviewing performance and discussing the issues with plant leaders in a meeting room, we took a Gemba Walk to see what was actually happening.

Owning Their Solution in the Weld Shop
I have conducted many workplace organization Kaizens (5S) over the years. The results have always been dramatic. All of the teams were made up of production operators or office workers, with some mechanics assisting the team. The production operators or office workers owned the areas needing organization and the mechanics were able to do some of the more complex tasks needed during the Kaizen. All of the teams, that is, until I met my Weld Shop team. Five mechanics and an engineer, who underestimated what we could accomplish.

Go See for Yourself – The Best Selling Tool There Is
In 2006, our Kaizen team was working on improving changeover time for a painting operation. After reviewing changeover reduction techniques with the team, we took a walk to the line to observe a changeover. The team watched the paint technician clean the front of the paint booth with water for approximately 10 minutes. After that, he walked behind the booth for a few minutes and then came back to work on the front of the paint booth. None of the team members had followed him to see what he had been doing in the back of the booth.

Sometimes It’s a Financial Question
A global ceilings manufacturer was building a plant in China. Things were going pretty well until they realized they were going to be two months late starting up. The team wasn’t sure what they could do to get back on schedule, so I was invited to join them and use Lean thinking to help solve the problem.

Breaking Through - The Edge
In 2005, I was asked to help a team reduce the changeover time of a painting operation at a ceiling tile manufacturing plant in Oregon. The approach I used was SMED – Single Minute Exchange of Die. The goal was to reduce the existing changeover time by 50% or more, while improving the safety of the work.

Improving Changeover Time in 4 Simple Steps
Have you ever watched an auto race? If so, you probably noticed what happens when a car enters Pit Row and is tended to by a whole team of people trying to get it back on the track as fast as possible. If you wondered how they knew what to do and how they didn’t get in each other’s way, the answer is SMED.

The Pursuit of Creativity
In my years of running Kaizen events, I never saw anything as powerful as a creativity approach called 3P – Production Preparation Process. The goal is to eliminate waste in the design of a new or existing process or product in the maximum way possible, unlocking the creativity of the team in ways most of them have not experienced. In 2016 I was fortunate enough to experience this approach through the eyes of the man who invented it, Chihiro Nakao.

A Simple Way to Think about a Problem You Want to Solve
Many years ago, I was having difficulty getting my mind straight about a problem that I wanted to solve. A co-worker of mine introduced me to a thing he called a “Task Cycle”. Once I understood it, I had a simple way to go about solving problems and executing tasks.

What Happens in a Cost Reduction Session?
Most companies want to reduce costs in their operations. There are many ways to do this. Some companies choose to reduce their workforce, others decide to sell off under performing businesses. Companies that use this approach are just avoiding the problems and inefficiencies of their business practices and are not targeting the root cause of their problems.

Who is Your Customer?
We are all customers. We want what we want, when we want it, at the level of quality we expect, in the proper quantity. We are the final say as to whether a business will thrive, survive, flounder, or die. The business must deliver to our expectations, or we will not continue to purchase products or services that they offer.