
Kaizen Success Stories
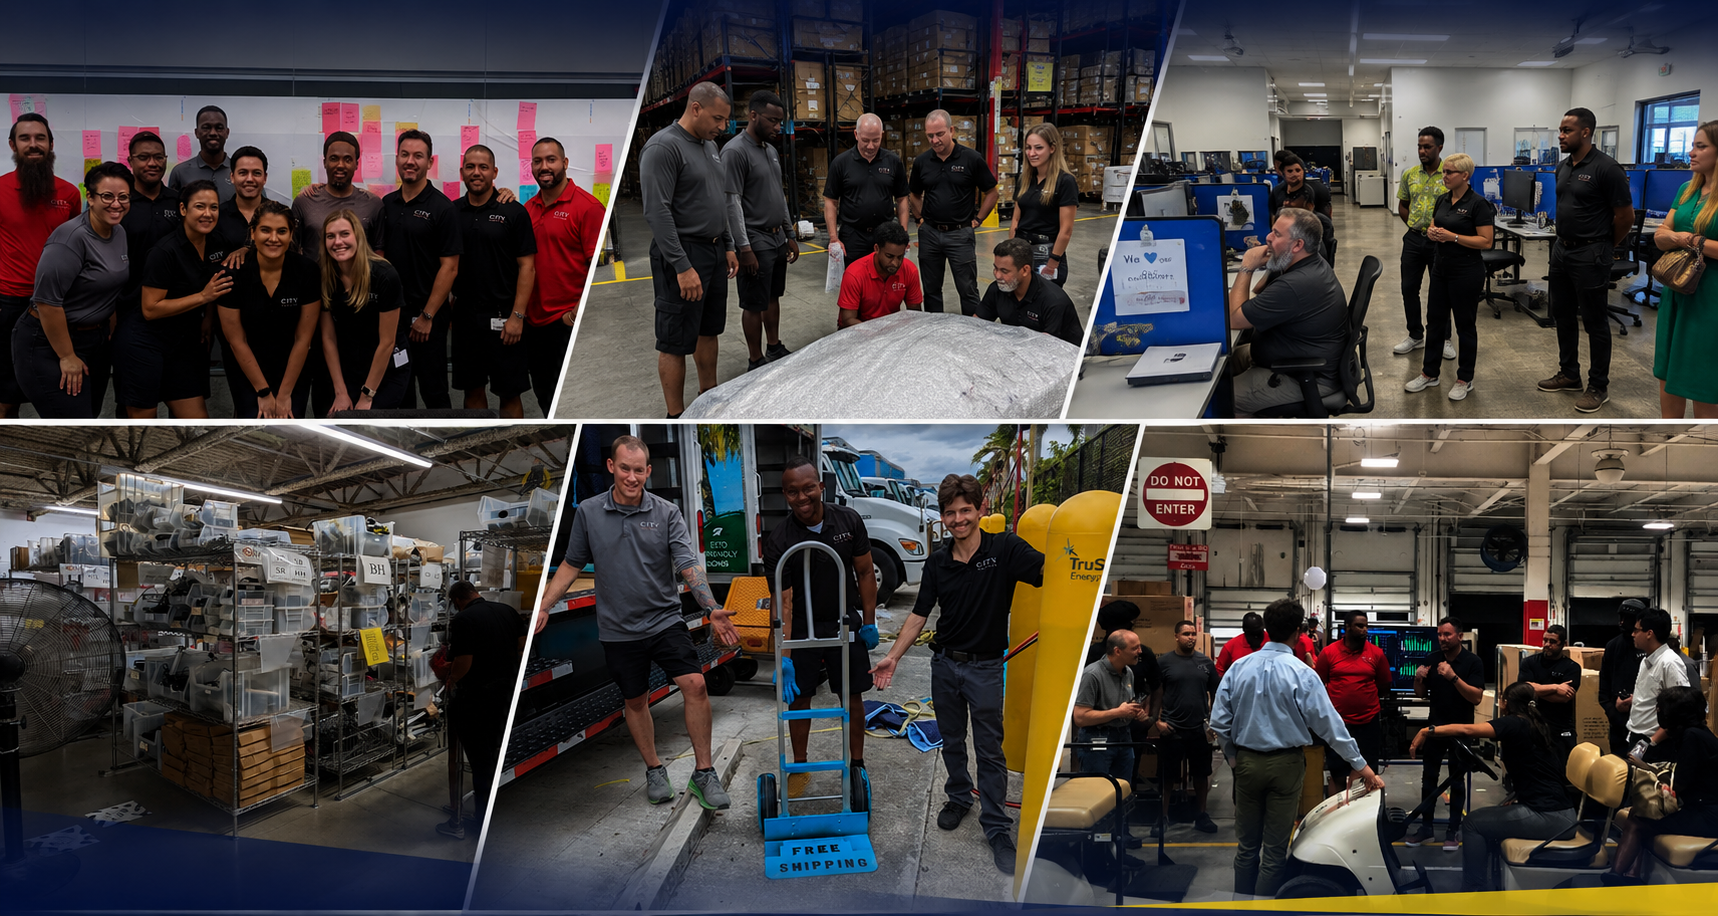
Real Manufacturing Results. One Kaizen at a Time
Explore real-world Kaizen success stories showing how manufacturing teams solved critical problems, improved performance, and created sustainable results.
My First True Gemba Walk
I started my career as an industrial engineer for Thomasville Furniture in North Carolina. My initial responsibilities included warehouse barcoding support and veneer plant projects. For the warehouse, I had to learn how barcodes were used to inventory, ship, and receive finished furniture from the various plants in the network. In the veneer plant, I was to conduct time and work studies and also identify improvement projects.
I started my career as an industrial engineer for Thomasville Furniture in North Carolina. My initial responsibilities included warehouse barcoding support and veneer plant projects. For the warehouse, I had to learn how barcodes were used to inventory, ship, and receive finished furniture from the various plants in the network. In the veneer plant, I was to conduct time and work studies and also identify improvement projects.
Time and work studies consisted of walking around with a stopwatch and a clip board and verifying a number of things: how long it takes to complete a task, how often people were working and how often they were not working. I was told to take a random tour of the plant daily and spend no more than 30 minutes conducting my studies. Holding the clip board and stopwatch can be viewed in a negative light by those you are timing and studying. I was getting some challenging comments when I walked around the plant to do my work.
I realized people at the plant didn’t understand what I was doing, and that it wasn’t designed to hurt them personally. I was helping the company determine capacity and plan appropriately for seasonal changes in demand.
One morning, I asked my manager if I could take more time during my time and work studies to better understand what I was measuring and to get to know the employees better. He agreed and I happily set out to visit the veneer plant.
I started in the matching department. This is where sliced wood with similar wood grain patterns is taped to another piece of sliced wood, to make a desired visual effect. As I started my study , one of the workers made a personal comment about me. I swallowed my pride and walked up to her and introduced myself. This caught her off guard. I then explained to her what I was doing. She told me no one had ever explained time and work studies to her. She assumed I was an “investor” and was trying to decide whether or not to buy the plant and shut it down.
I assured her I was there to do a job just like her and we started talking about why both our jobs mattered. Hers was to ensure the customers got what they paid for and mine was to ensure customers would never have to wait for the furniture they bought.
Now she was sharing her concerns and problems in her department. She also encouraged others to share their issues. I realized I had a great opportunity to learn what was really going on and to identify future critical work opportunities to share with my manager.
I had to balance the fact that my time and work studies were going to take much longer than 30 minutes with the fact that the ideas and improvements coming from the discussions would pay for the extra time. It didn’t take long to find a bunch of ideas and projects from these discussions that more than made up for the additional investment of time.
Even though I didn’t know it at the time, I was conducting a Gemba walk and learning about the processes with the people who do the work. I have used this approach in all of my work to this day and now teach others to take the time to truly understand processes with the people that do the work. Invest the time and the rewards will more than pay for themselves.
When Someone Knows You Better than you Know Yourself
I met Cody at a conference in December. We got along so well he invited me to visit his new company in Florida. Before the conference was over, he asked for six copies of my book, “The Wheel of Sustainability.” He wanted a copy for every member of his leadership team. Cody told me he was going to require them to read it before my visit. I was happy to share my books, as no one had shown so much interest in them before. I never could have imagined the level of interest and enthusiasm of one person in particular.
I met Cody at a conference in December. We got along so well he invited me to visit his new company in Florida. Before the conference was over, he asked for six copies of my book, “The Wheel of Sustainability.” He wanted a copy for every member of his leadership team. Cody told me he was going to require them to read it before my visit. I was happy to share my books, as no one had shown so much interest in them before. I never could have imagined the level of interest and enthusiasm of one person in particular.
In January, I flew to Florida to visit Cody and his team for the day. I was met outside their new corporate building with a bear hug. Cody led me into a conference room and introduced me to his leadership team. I sat down and noticed 4 skeptical looking, “grumpy old men” sitting across the table. Cody sat on my side of the table, and in front of him was my book, with many pages dog-eared.
I introduced myself and shared my interest in the work they were doing in their new company. After a few minutes, one of the men across the table asked me a terse question. I interpreted it to mean, “Who are you and why are you here? We have more important things to do today.” I answered I might be able to help them on their journey as a start-up.
After a few more minutes of shallow questioning, the COO talked about a specific problem they were having. The CIO entered the conversation and after a few minutes, I shared a view of how I might go about solving the problem with a team. Cody then said, “That’s from page 144 of your book, isn’t it Adam?” I was shocked he knew the book well enough to cite the page number. He proceeded to show me it was indeed on page 144. Was this a coincidence?
The conversation started to get more engaging and now it was clear the leadership team was warming up to me and my approach. We started talking about another critical issue they were facing, and I shared my experience in helping other teams in similar circumstances. Cody interjected, “That’s right off page 198, isn’t it Adam?” I said, “I’m not really sure, but I think it’s in my book somewhere.” Cody showed me it was on page 198 and said, “Don’t you know what pages you put your wisdom in?” I replied, “Cody, I was so happy to finish the book I haven’t opened it since. You know my book better than I do!”
Now the room was on my side, we were talking about issues and I was demonstrating ways to help them they could use immediately. After about two hours, the meeting concluded and Cody walked me around the rest of the corporate facility, sharing his vision of what he hoped the company could become. I was inspired.
At dinner, Cody and his team agreed we should figure out a way I could be a part of their start-up journey. I was fortunate enough to be able to assist them for a while and now have the additional opportunity to work with Cody as a partner in my business. It turns out that no matter the circumstances, you should treasure those in your network who are there to support you and understand you better than you might understand yourself.
The Bottleneck
I met Andrew Koenig, the CEO of CITY Furniture, at a virtual Lean conference during the pandemic. We immediately hit it off, and he invited me to help strengthen the Kaizen culture at his company.
For two years, I facilitated Kaizen events on a monthly basis. It never ceased to amaze me at the number of improvements and breakthroughs that could be accomplished in a company that has been living Lean and continuous improvement for many years. More than that, the energy of team members was inspiring and infectious. I was warmly greeted by associates on every trip and many of them proudly showed off prior improvements and how they were sustaining the gains from our Kaizen events.
I met Andrew Koenig, the CEO of CITY Furniture, at a virtual Lean conference during the pandemic. We immediately hit it off, and he invited me to help strengthen the Kaizen culture at his company.
For two years, I facilitated Kaizen events on a monthly basis. It never ceased to amaze me at the number of improvements and breakthroughs that could be accomplished in a company that has been living Lean and continuous improvement for many years. More than that, the energy of team members was inspiring and infectious. I was warmly greeted by associates on every trip and many of them proudly showed off prior improvements and how they were sustaining the gains from our Kaizen events.
Late in the first year of my support, I met with the COO, Will Conway, during our monthly review. He always told me I was too expensive, but what he told me next stopped me in my tracks.
“Adam,” he said, “I love the results your teams have been getting. The engagement and excitement is amazing. We want more of this, but we can’t afford to bring you here more often. You’re the bottleneck. Can you help us figure out a way to expand this work?”
This would be a challenge. I had more than 30 years of experience facilitating teams. I honed my craft through many experiments and mistakes. I get feedback about how my teams accomplish results more quickly than many of the other consultants I have followed. Somehow, I would have to put together all of my experience into a training program.
I said, “Will, this is quite a task you’re asking of me. But I feel it’s something I must take on. I owe it to you, your teams, and quite frankly to me. If I can somehow figure out how to upskill other facilitators, I will have something I can transfer to others so my approach can live on after I have stopped working. Challenge accepted!”
Over the next few weeks, I developed my Kaizen Facilitator Certification Program. It consists of these elements:
- Kaizen Facilitation Prep Course
- Participate as a Kaizen team member
- Participate as a Kaizen team leader
- Co-facilitate a Kaizen with me as the Lead Facilitator
- Lead facilitate a Kaizen with me as the co-facilitator
I developed reviews for the candidates, to ensure that they were ready to move on to the next (or final) step. The ultimate goal would be to solo-facilitate a Kaizen event. I knew no matter how much training and support I gave, the candidates would still make mistakes. As long as they showed the desire and drive to learn from them and demonstrated the principles of facilitation, I was willing to move them to the next phase. I knew I couldn’t “rubber-stamp” anyone’s certification. This would damage their results and my reputation.
Will chose four high-potential candidates from across the company. All except one had been at least team members in prior Kaizens with me. The other candidate had facilitated Kaizen events prior to joining CITY Furniture, so everyone agreed she could skip the Kaizen team member and team leader steps.
During the three-day Kaizen Facilitation Prep Course, I demonstrated the principles and techniques of facilitation. I had each candidate practice everything I taught. Then, I sent them out to meet with sponsors to develop charters for upcoming Kaizens. Following this, they developed Kaizen event plans and learned specific tools to utilize, such as Value Stream Mapping and The Wheel of Sustainability. At the end of the course, we celebrated, and I was hopeful they were all prepared for their next steps.
Over the next eight months, I facilitated Kaizen events with each of the candidates separately and was impressed by how much they learned and incorporated into their approach to facilitation. I was thrilled when some of the candidates went “off-script” and created their own approach to what I taught them. Their confidence was growing and at the end of each review, we talked through what they learned and what they thought they could do better next time. Every one of them was ready to take the next step.
I held separate reviews with Will, so that he could ask me the more challenging questions about each candidate. He agreed all of them were ready to solo facilitate.
And that’s what they’ve been doing. I don’t get to facilitate any more CITY Furniture events. I have eliminated the “bottleneck” and worked myself out of a job, which also frees up my capacity to pursue new challenges. From time to time, I get a text or an email showing me some of the breakthroughs they have made since I have left. It makes me feel good that I have been able to help them grow their capability and capacity. I feel even better knowing the program I developed can be used to help others and that things are no longer dependent on me.
Surviving a Brutal Work Environment
I have experienced two mergers/joint ventures in my corporate career at Armstrong. The first one was a ceiling grid venture between Worthington Industries and Armstrong. It was extremely positive and productive and is still doing well to this day. The second one was a ceramic tile venture between Armstrong’s American Olean Tile and Dal-Tile, based out of Dallas Texas. This one didn’t go nearly as well. I learned many lessons from the Dal-Tile experience, mainly about my ability to survive.
I have experienced two mergers/joint ventures in my corporate career at Armstrong. The first one was a ceiling grid venture between Worthington Industries and Armstrong. It was extremely positive and productive and is still doing well to this day. The second one was a ceramic tile venture between Armstrong’s American Olean Tile and Dal-Tile, based out of Dallas Texas. This one didn’t go nearly as well. I learned many lessons from the Dal-Tile experience, mainly about my ability to survive.
When the “merger” was announced, I investigated other opportunities for my career, including a chance to go back to Thomasville Furniture as an assistant plant manager in Winston Salem, and an offer to do work at Armstrong’s corporate center. My recent experience with the Worthington and Armstrong joint venture was positive and I learned a lot at the beginning of the venture, so I thought I would see a similar approach to this combination of companies. Boy was I wrong.
Our Plant manager left us without saying a word. We only found out a week or so later he had gone to the Dal-Tile headquarters to prepare for the merger through a mysterious sounding voicemail. On the official first day of the merger, executives came to our plant and told the acting plant manager he had to fire five staff members by the end of the day.
I was the industrial engineering manager at the plant, and the only way I survived was that I was named as a supervisor. Dal-Tile only staffed their plants with plant managers, supervisors, and ceramics engineers. Any other staff was excess in their view.
I took the supervisory role because I was promised a job at the corporate headquarters in Dallas Texas. My favorite manager from American Olean would be my manager in Dal-Tile corporate. Even though things were challenging at the plant, I had something exciting to look forward to.
When I got to Dallas Texas, I found out we were in charge of assuring environmental, health, safety, and mining compliance across the entire company. There was a department responsible for this already. But they weren’t very helpful to the manufacturing and mining sites. The VP of operations put us in the middle of the plants and them.
We tried to work with the existing EHS and mining group, but they went to great lengths to avoid us. One time, my manager and I walked over to their offices to meet with them impromptu. Instead of meeting with us, they locked their offices and refused to talk with us. What a culture!
Another thing Dal-Tile was proud of was their firing practices. The employee manual started off with a paragraph explaining that Texas was an “at-will” state, which meant they could fire you at any moment, with or without justification. This was on the first page of the manual! I met many people who had been fired and then re-hired and then fired again. Amazing.
I knew the only way I was going to survive this brutal culture was to make myself as valuable and helpful as possible. I took every assignment, put in outrageous hours, and traveled at the drop of a hat, to support any of our twelve manufacturing facilities and multiple mining sites.
I had good relationships with the plant staff. Once they got to know me, they trusted me. They didn’t trust the EHS and mining group, that was for sure. They knew when I arrived, I would be there to help. Nothing more and nothing less.
I had many amazing experiences I would never have had in a more positive working environment. But, after 18 months, I was free to return to Armstrong (there was an agreement that we were off limits for that period of time). I made a few calls and was able to join the corporate group in Lancaster, working for the same manager I followed to Texas. He had left a month or so earlier and was able to convince his manager to hire me.
When I returned to Armstrong, I realized most people wouldn’t believe how we were treated at Dal-Tile. They never experienced a brutal corporate culture. So, I kept the stories to myself or commiserated with those few who survived their time in Dallas Texas and returned to Armstrong like me. Very few made it through unscathed. Those that did had some scars from the battles we fought but were also proud that we made it.
To this day, Dal-Tile is my example of “if you think your job is bad, check this out.” No one should be treated the way we were. Because of this, I really appreciate what I have and my determination to survive.
You’re Not in Kansas Anymore
I worked as a supervisor in a small ceiling grid plant for Armstrong in Franklin Park Illinois. In my first year there, Armstrong and Worthington Industries created a joint venture to leverage each other’s strengths and grow the business. I was offered the role of industrial engineering manager at the plant in Sparrows Point Maryland. The plant in Franklin Park was going to be closed.
I worked as a supervisor in a small ceiling grid plant for Armstrong in Franklin Park Illinois. In my first year there, Armstrong and Worthington Industries created a joint venture to leverage each other’s strengths and grow the business. I was offered the role of industrial engineering manager at the plant in Sparrows Point Maryland. The plant in Franklin Park was going to be closed.
After helping to shut down the plant, I moved my family to Baltimore and started my new role. I quickly realized how much more Worthington understood grid manufacturing. They provided the steel and the science of roll-forming was clearly followed by them. They were quickly helping us improve performance.
I was invited to the corporate headquarters in Malvern Pennsylvania, to meet with various executives in the new venture. Malvern was a manufacturing site for Worthington, and they oversaw the day-to-day operations.
I always thought Armstrong was a conservative company with very simple and powerful values. Mostly guided by the Golden Rule, people were treated with respect and all rules were followed, to the letter. I even joked we were run by the Amish, who have a very simple, but hard-working life. Great people with an amazing work ethic. We were so strict and inflexible at Armstrong. It seemed like fun was missing. Or if not missing, it was well-hidden.
I arrived early in the morning and met with the president of the new venture. He was very passionate about the possibilities for the business and had laid out an agenda for my day. First up was the VP of manufacturing, quality, and then the VP of engineering.
When I met Bill, the VP of engineering, he told me a little about himself. He didn’t have a degree in engineering but had a lot of experience. This would never have been allowed at Armstrong. He also told me he’d rather go to lunch to get to know me. How could I say no?
We went to a local pizza joint, and he ordered a pitcher of beer. I told him I don’t drink during the workday and he told me, “That’s alright, it’s not for you!” I was surprised because I had never seen anyone at Armstrong drink during work hours. But I was also intrigued by the looser approach to work. I drank my Coke and Bill proceeded to finish the pitcher. I definitely got to know him better and we shared many stories and laughed a lot.
The rest of the day was a blur, but I got the same positive vibe from others I met as I did from Bill. Over the next two years, I got the opportunity to participate in many fun activities with other colleagues from the venture. They had the best parties and gatherings. We played hard and worked hard, and the venture became the number one grid manufacturer in the world.
Do Your Due Diligence
Midway through my corporate career, I was a senior industrial engineer at Armstrong World Industries. I spent most of my time providing support to our many manufacturing facilities all over the world. I have always been fascinated by manufacturing and it never ceases to amaze me how good (and bad) decisions can immediately impact performance.
Midway through my corporate career, I was a senior industrial engineer at Armstrong World Industries. I spent most of my time providing support to our many manufacturing facilities all over the world. I have always been fascinated by manufacturing and it never ceases to amaze me how good (and bad) decisions can immediately impact performance.
I thought I would someday be a plant manager and told my manager I wanted the opportunity to take the next step to get me there, as a business unit manager. I thought all my continuous improvement experience would serve me well and I would make more good decisions than bad ones.
One day, the week before Easter, my manager informed me that the plant manager at the Lancaster flooring plant wanted to talk to me about a position in his plant. I was excited for two reasons. One was my opportunity to learn manufacturing from the inside. The other was it would be a two-grade promotion. More money was never a bad thing, or so I thought!
I met Rob, the plant manager, on the Friday before Easter weekend. The plant wasn’t running, but he gave me a short tour of the areas I would be responsible for. All of the hourly workers were gone and I never met anyone on the staff. I thought it was odd, but I was enamored with the idea of the next step towards plant manager.
At the end of the tour, Rob offered me the job and told me that he wanted my answer by the end of the weekend. Even though I knew my answer, I told him I would talk things over with my family and get back with him on Monday morning.
I really didn’t think too much about it. I knew I was going to take the job. My wife was supportive and knew this new role would keep me home more. But the hours were going to be long. It was a tradeoff, but it seemed like the right choice to make. I did mention it was odd that I hadn’t met anyone during the tour, but tried not to read too much into it.
On Monday, I called Rob and told him I would take the job. My manager and I agreed on a transition plan, as I had some projects to wrap up or hand over to others. For the next four weeks, I tried to do both jobs, spending half of my time at my new factory, watching the staff conduct business.
One week before I started my new job full-time, Rob was promoted and left the plant. His replacement wouldn’t arrive for six more weeks. In addition, my counterpart in the factory who ran a different business had a three-week National Guard deployment. I would essentially be on my own, learning as I went.
I had a staff, but they didn’t know me. I also had the vice president of manufacturing to discuss issues with, should things get out of hand. I really didn’t want to have to use his support, but there were a few times that I had to. There were some union/management issues to be resolved and I didn’t have the historical perspective to help me out. So, I swallowed my pride and met with the VP. He was very helpful and supportive. He understood my lack of experience.
For the next few weeks, I barely survived. Finally, my counterpart came back and helped me deal with some issues and then our new plant manager arrived. Things got better, but they were tough. This plant had been in decline for many years and the management and union relationship was strained, to say the least. I did my best to improve things throughout my two years as business unit manager.
Would I have chosen a different path if I had known what was in front of me? Maybe. More likely, I would have tried to gain perspective on what I was agreeing to well before accepting the job. It would have eliminated some of my early bad decisions. It was an amazing learning experience. I like to think I gained twenty years of experience during my time on the job.
Living in the Moment
During my career, I have been fortunate to have worked all over the world. I was brought up as a “tourist.” Whenever I traveled with my family, we would do everything possible to see the sights and learn the history of the region we were visiting. Because of this, I naturally enjoyed my business travel and did my best to explore and experience the culture of any location I visited.
During my career, I have been fortunate to have worked all over the world. I was brought up as a “tourist.” Whenever I traveled with my family, we would do everything possible to see the sights and learn the history of the region we were visiting. Because of this, I naturally enjoyed my business travel and did my best to explore and experience the culture of any location I visited.
I was scheduled to assist Tim, a project manager on a critical project in Munster, Germany. We were evaluating the ramifications of expanding the plant and I was asked to utilize discrete event simulation modeling (explaining that is another story) to evaluate the capacity gain and future bottlenecks in the process.
I scheduled a two-week visit to the plant and had the weekend to explore the region. On my own, this would have been interesting, but with Tim, it turned into an all-out adventure. On Saturday, we took a cruise down the river and learned about the historical battles between the German and French armies. Castles would be destroyed, rebuilt, taken over, and then destroyed again.
On Sunday, we traveled to Belgium. Using the GPS (this was many years ago), we set out to find a museum to learn about the Battle of the Bulge. After being redirected into a few fields, we finally found the museum and learned history from a different perspective than what we had been taught in the United States.
After touring the museum, Tim mentioned that Nürburgring, a famous Formula 1 track, was in the vicinity. I knew he was a big Formula 1 fan, so I quickly agreed to go with him to the track. We got to the track and parked the rental car. Since we didn’t have tickets, Tim was happy to just look at it from the outside.
I saw people walking in and suggested we join them inside. If we acted as if we belonged there, what was the worst that could happen? We joined the crowd and since no one was checking tickets, we made our way in. We climbed into the stands and watched as cars were “practicing” on the track.
Tim was in heaven. You could see he had ticked off a “bucket list” item. I enjoyed watching him as he was deep in his element. The sounds, smells, and experience filled him with joy. There was an infield section where cars were being maintained and tested. Tim looked longingly at the action, and I suddenly knew what I had to do.
I got up and said, “Follow me.” I started down the stands and Tim came along, saying, "There’s no way they’re going to let us go there.” I said, “What are they going to do, kick us out of the country?” Seemed unlikely, so we headed down and walked onto the infield, looking like we belonged there.
We spent the next two hours looking at cars and talking with drivers and mechanics. It was an amazing experience for Tim and me. I just enjoyed seeing Tim in his element, talking about cars, racing, and any other topics that I probably didn’t understand.
There’s a lot of similarities to what I do today as a consultant and my adventure with Tim. I venture out into the unknown, acting like I belong. I definitely enjoy living in the moment with my Kaizen teams and feeling pride when they win.
Getting More Than They Bargained For
My first Kaizen event with a new client in Oregon came as result of my site visit the month before. We were going to apply 5S to an area of their plant that was well behind budget. During my visit, I noticed that although prior efforts had been made to improve organization, they hadn’t stuck. With the appropriate use of Lean principles and the Wheel of Sustainability, I felt I could help them get back on track.
My first Kaizen event with a new client in Oregon came as result of my site visit the month before. We were going to apply 5S to an area of their plant that was well behind budget. During my visit, I noticed that although prior efforts had been made to improve organization, they hadn’t stuck. With the appropriate use of Lean principles and the Wheel of Sustainability, I felt I could help them get back on track.
After a few hours of training on Day 1, we took a Gemba walk into the space we were going to work on. There were several workstations with their own tools, tooling, and instructions. They were cluttered and disorganized. There was no indication of what was necessary and what was obsolete. There was a large central storage area, filled with heavy tooling for all the presses used at the workstations. One of our team members was responsible for the area and he admitted many items were no longer in use and were in the way of tooling that was current and needed.
Other areas were similar. Whenever someone needed tooling, materials, or supplies, they would have to wade through obsolete items to find them. That’s when it struck me – our 5S efforts could be used to make a direct impact on the productivity of the area. I proposed an experiment – perform a changeover on one of the presses and find out how much time, energy, and searching was required. Then, once we completed our major 5S work, we could compare “before and after” results.
I taught the team how to use spaghetti diagrams to follow the travel of the person doing the work. It would show the back-and-forth motions we could try to eliminate later. One of our team members volunteered to do the changeover. She had to search for materials, move things out of the way, and dig through clutter to do her work. Forty-five minutes later, she was finished. She looked frustrated. I asked if it was always this way. She said this was normal. Team members held up their diagrams and sure enough, they looked like spaghetti. We could make it much easier to do this work once we eliminated most of the “spaghetti” by applying 5S to the area.
I asked the team to write down their ideas to remove clutter (sort), optimize placement and create visuals (set in order), and to repair and clean equipment (shine). With almost 100 ideas on post-its, we prioritized our work. The team broke up into 3 sub-teams and worked on their critical projects.
After Day 3, there was an amazing transformation. All areas looked organized, well-labeled, and less cluttered. Over 30% of the tooling in the central storage area was identified as obsolete and was inventoried and relocated off-site.
On the morning of fourth day, we conducted another changeover with our original volunteer. She was able to complete the work in less than half the original time. She actually was able to slow down and take her time to do the work in a confident way. She didn’t have to move anything out of her way, sort through obsolete items, or search for what she needed. She took far fewer trips between her workstation and the central storage area. Our spaghetti diagrams looked much cleaner than on the first day.
My team was elated. But we were far from done. Now it was time to implement the Wheel of Sustainability to ensure their great results lived on. We named two Area Owners and built a board to post expectations, audits, and results.
We practiced the audits and checklists, and everyone agreed they could handle the tasks on a daily and weekly basis. They also felt that by doing these tasks, it would make work easier for everyone throughout the day and sustain the high performance we had demonstrated.
Following up with the team months later, they admitted they had a slow start, but after a few weeks, performance had reached budget levels. They are fully committed to continuing their great work in other areas.
Five Tips for Effective Meetings
Have you ever had a meeting where it seems like nothing was accomplished? Is every meeting this way for you? Do your meetings start late? I have facilitated hundreds of meetings and Kaizen events and have learned over the years these five key tips to an effective meeting.
Have you ever had a meeting where it seems like nothing was accomplished? Is every meeting this way for you? Do your meetings start late? I have facilitated hundreds of meetings and Kaizen events and have learned over the years these five key tips to an effective meeting.
1. Define the purpose.
2. Create a clear agenda.
3. Facilitate the meeting.
4. Set expectations.
5. Hold accountability for actions.
Define the purpose of the meeting.
Why are we meeting in the first place? What are the expectations for the team members in the meeting? Why are they there? If everyone knows why they’re there and what’s expected of them, they will more likely prepare and engage in the meeting. It also makes it easier to choose team members for the meeting. Simply put, if someone is not aligned with the purpose, they shouldn’t be invited.
Create a clear agenda.
The path from the beginning of the meeting to the end should be mapped out. How do we get to a decision as a team? What information will be shared? Who is expected to share it? What preparation should happen prior to the meeting? Does the agenda lead us to our purpose? Taking the time to create an agenda helps to remove any of the excess or unnecessary parts of the meeting, resulting in shorter, more focused meetings.
Facilitate the meeting.
Don’t leave things to chance. Someone should run and manage the meeting. This person can help the team stay on track, not wandering “into the weeds.” It’s best to use a facilitator who isn’t deeply invested in the topic being covered, but that may not be practical. Facilitation is a skill that’s highly valued, so rotating this responsibility will help team development.
Set expectations.
Start and end on time – that’s the first expectation of any effective meeting. It seems so simple, but we let things get in the way of being punctual. Other expectations should be shared as ground rules for the team. Examples include: One voice at time, be open to others’ views, work collaboratively, no calls or texting during the meeting, and others the team may develop. If anyone breaks a ground rule, the facilitator should call them out immediately and correct their behavior. The sooner this is done, the more serious the rest of the team will take these expectations. Following ground rules is a sign of respect for the team and the topic being discussed.
Hold accountability for actions.
Every meeting should have an outcome. Sometimes it’s the sharing of critical information. Other times, there are action items that must be completed. Team members should know what they’re accountable for and be responsible to meet their obligations. Therefore, assignments should be listed visually, with owners and due dates. Updates should be a part of the meeting agenda. Don’t wait until an assignment is due. You want to make sure the assignment owner has a chance to complete his/her task(s). If they’re on track, thank them. If not on track, provide help.
These tips work. It takes a while for the team members to get used to them. But once they do, your meetings will be more productive, effective, and engaging.
Leadership Commitment in a Most Challenging Situation
Last year, Dave, a network connection, reached out to me to see if I could help him in his continuous improvement journey. His wife had worked with me at Armstrong, and one evening he was talking with her about some of his frustrations at work. She said, “If you want to get the right help, call Adam. He is tenacious and won’t let you or your team fail.”
Last year, Dave, a network connection, reached out to me to see if I could help him in his continuous improvement journey. His wife had worked with me at Armstrong, and one evening he was talking with her about some of his frustrations at work. She said, “If you want to get the right help, call Adam. He is tenacious and won’t let you or your team fail.”
Dave invited me to his factory, which was quite large and had several furnaces that smelted and poured molten metal into ingots for high value customers. They had a problem with tools and equipment going missing, which led to significant productivity losses. He wanted to reinitiate and strengthen their 5S program. I knew I could help, and wrote a proposal for the work, which was approved quickly.
We scheduled the Kaizen event for eight weeks from my initial visit. This would allow Dave to prepare leadership and gather the proper team for the Kaizen. We had already chartered and scoped the event to cover one of the furnaces. Our idea was that our improvements could be replicated to the other furnaces in the facility.
In the meantime, I spent a day at the facility getting required safety training and preparing Dave for the event. We picked a conference room and identified the supplies necessary during the week.
Three days before the Kaizen event, Dave called to tell me he had contracted COVID. I asked him if he wanted to postpone the Kaizen. He told me no and if I could pick up the supplies from his home (in his driveway), one of the team members would fill in as team leader until he could participate at the facility. He would use Zoom to attend and participate on the first day of the Kaizen. His five-day isolation period would then end, and he could attend in person on the second day, but would have to wear a mask.
I wasn’t sure what to make of this. All my Kaizen events (up to that time) were in-person, and I didn’t really know how engaged Dave could be attending virtually. But I was willing to give it a try and make the best of it.
On the Sunday before kick-off, I met Lisa, who was going to fill in for Dave as team leader. She helped me prepare the meeting room. We talked about how we could engage all team members, including Dave on the first day of the Kaizen. We set up a laptop for Dave that we could point toward the team and the screen, so that he could engage with the team and keep up with the discussions. Luckily, he and I had spent time in the workspace, so he had a list of ideas to share during that portion of the Kaizen.
At kick-off on Monday, we introduced everyone and shared Dave’s story and said we were going to make the best of a difficult situation. For Dave’s part, he stayed on Zoom the entire time, engaging and speaking with the group at appropriate moments. When we went out to the facility floor, Dave waited for us to text him that we were returning to the meeting room. The team had many ideas and Dave was able to share his as well. When we prioritized the many ideas into a vital few, Dave was able to participate as if he were in the room. We took the laptop over to the list of ideas and Lisa voted on Dave’s behalf.
Now it was time to work on the high priority projects. Dave couldn’t really do that, so he signed off until we met to wrap up for the day. He listened intently to the team’s progress and gave them encouragement and told them he couldn’t wait to come in the next day and help them in their work.
The second day, Dave showed up with a facemask and kept his distance from the team members. He jumped on one of the project teams and was able to participate in the improvement work. Throughout the week, the team felt more comfortable letting Dave engage in the work and by the end of the week, he was able to help complete many critical tasks.
At the end of the week, the team had made significant improvements to their furnace area. We did a quick estimate on the impact on productivity and changeovers and felt we had made a huge impact on both. Time would tell, of course. For his part, Dave earned the respect of the team and had his first true win in his position as Continuous Improvement Manager. I was impressed by his dedication and commitment and was thankful we didn’t have to postpone or cancel this Kaizen event. I also learned it was possible to engage remote team members in Kaizen events.

A Picture is Worth More than a Thousand Words – It’s Priceless
Earlier this year, I received an email from someone I never met, asking about my approach to 5S – organizing a workspace to improve safety and productivity. He heard about me from another location in his company, who I helped six months earlier. Later that week, we were in a Zoom meeting, and he invited me to his factory in Oregon to see if I could help jump-start their 5S efforts.
Earlier this year, I received an email from someone I never met, asking about my approach to 5S – organizing a workspace to improve safety and productivity. He heard about me from another location in his company, who I helped six months earlier. Later that week, we were in a Zoom meeting, and he invited me to his factory in Oregon to see if I could help jump-start their 5S efforts.
Three weeks later, I was on a plane, heading to the west coast. I arrived early in the afternoon and met with Ben, my sponsor. We took a tour of the factory and strategized about my approach with the leadership team the next day. I saw many places where 5S and other Lean tools could help them out. People in the factory were engaged and appeared ready to take a first step on their continuous improvement journey.
That evening at dinner, Ben told me about past continuous improvement efforts. There weren’t many success stories shared. I was told one consultant had visited and said he couldn’t help them. I couldn’t understand how that was possible.
The next morning, Ben and I walked around the factory again. It helped ground me and remind me of the complexity of their processes. A little later, I attended the morning leadership walk around the factory. Although there were a dozen staff members attending, only one or two were engaged at any time. I took a risk and gave Roy, the facility manager, some feedback about how he might engage his staff more effectively. He took my feedback in stride (he didn’t kick me out of the plant, so that was a good sign).
After the leadership walk, Ben and I talked about what I had seen, and we prepared for the leadership review at lunch. We created a list of the top three areas that could use my help. There were unlimited opportunities for improvement at the facility.
At lunch, we crammed into a small conference room. There may have been a dozen people seated around a table designed for six. I introduced myself and thanked them for giving me the opportunity to visit and learn about their processes. I spoke about what I saw and where I thought I could help. I wasn’t getting much engagement from the leadership team and realized my words weren’t connecting with them. With a less than successful history of continuous improvement efforts at their factory, they were naturally skeptical.
That’s when it hit me – talk about the successful Kaizen event from their sister facility. I started describing the work I did with the team. We were able to reduce a critical changeover by many hours, leading to substantial savings for the company. The leadership team started asking some questions. Then, I asked Ben if he had the report out from the Kaizen. He projected it on the screen. Now the questions were flowing. People were amazed at the “before” and “after” photos. How did we do this? Is it still working? How might we apply a similar approach locally?
Next, Roy asked where I would start. I reviewed the three areas Ben and I had prioritized. Roy said those were good choices, but he preferred to start at the beginning of the process, where quality would be most affected. I was happy to oblige, as it was much more important to gain alignment than to worry about where to start. Ben agreed and now we were talking about when we could kick-off the first Kaizen event.
I said I would charter the event with Ben, and then we could review it for approval. From there, I would write a proposal and then, once receiving a purchase order, the work could begin. I normally like to think for 24 hours before writing my proposal. But speed was critical. After chartering with Ben, I found a quiet office to write my proposal for the Kaizen. Then, Ben and I met with Roy and we were met with enthusiastic approval. I left the facility with a purchase order. The following month, I ran their first “successful” Kaizen event. But that’s another story for another day.
Go With Your Gut
I love giving out little trinkets. It’s fun to see people’s reactions to the things I hand out – coins, ninjas, books. This story is about ninjas.
I love giving out little trinkets. It’s fun to see people’s reactions to the things I hand out – coins, ninjas, books. This story is about ninjas.
I consider myself a Kaizen Ninja. Many years ago in Japan, Ninjas came out of the shadows to deal with a situation (usually violently), and then return to their home base, unseen. I’m not violent, but when I facilitate, I want the team to solve their problem and own their solution. It can’t be my idea. Don’t get me wrong, with over 350 Kaizen events under my belt over these many years, I have seen so many problem-solving techniques and ideas it’s almost impossible not to have a solution to offer to my team members.
Instead of telling, I influence team members to come up with ideas and solutions that may elude them otherwise. Sometimes, I must be direct, but most times, I can guide them from the side to a solution. Thus, I am a Kaizen Ninja.
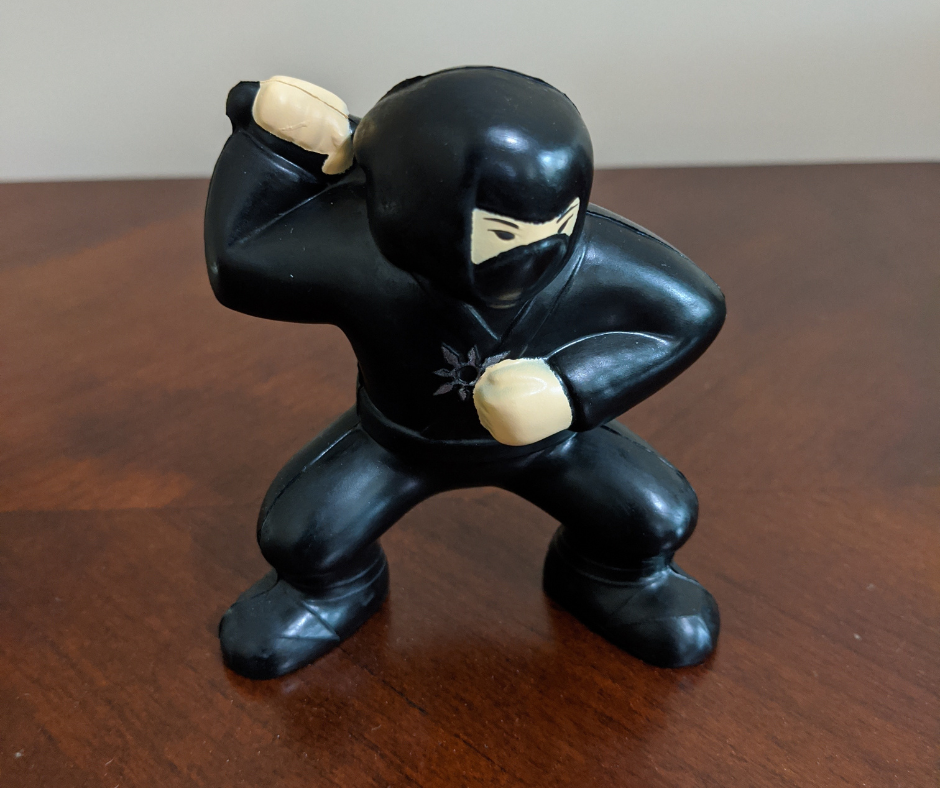
I signed up to be a sponsor for the BTOES2021 (Business Transformation and Operational Excellence Summit) conference in Orlando, Florida. As part of my sponsorship, I was scheduled to run several workshops and was given a small booth on the conference floor. I had to decide what to bring with me. I was going to be doing a book signing, so that was an obvious choice – bring a bunch of books. Others had books, so what else could I bring? Working with a local promotional item company, we came up with a ninja stress-reliever. I ordered 200 and planned on bringing all of them to the conference.
Two months later, during a meeting with my marketing mentor, a retired marketing executive with Armstrong World Industries, I reviewed my plans for the conference. After talking about how to maximize the value of my time at the conference, I showed her a ninja. She wasn’t impressed. She told me, “Adam, people don’t really use the swag they pick up at conferences. They take it to be nice, and then they get back to their hotel rooms and throw everything away.” She liked some of my other ideas – sticky notes with ninjas imprinted on them, and my books too.
I was floored. I had just spent hundreds of dollars on my ninjas. I was committed to the idea. I knew she was probably right, but I was determined to make the best of my decision. I decided to go with a ninja theme and see if I could attract attention and make many connections during the conference.
I arrived at the conference and found my booth. There was a lot more space than I realized to place items. After putting books on the table, I started lining up ninjas. Sixty of them were set up like a little army of process improvers. I also had ninja-themed signage for my book signing, workshops, and roundtables I would be hosting.
Once the conference opened, people started milling around the booths. The first few asked me sheepishly about my ninjas and I told them about my talents as a “Kaizen Ninja.” They seemed amused. By the middle of the conference, ninjas were being shared with almost every attendee. They were a hit! I almost ran out. I realized it wasn’t the item attracting people, it was the backstory and the energy I was bringing to it. While most booths were very dry and professional, I was having fun and people seemed to appreciate my approach.
After the conference, with newfound confidence, I started bringing ninjas to all my Kaizen events. I would make team members earn them. By the end of the week, every team member had received at least one. Walking around offices, I found about half of all ninjas given out were displayed on desks. This continues to validate my choice of giveaways.
I reviewed the “ninja-effect” with my marketing mentor, and she said she was happy to be wrong about my ninjas. I was just happy that my investment didn’t go to waste and that people enjoyed having a “ninja-moment” with me.
Carrying a Heavy Weight on My Shoulders
When you are in the heat of battle, you don’t realize the toll it’s taking on your health. I was the business unit manager for a vinyl flooring operation for Armstrong World Industries for two years. During that time, we were in a continual state of downsizing. This didn’t help the relationship with our union. It seemed like everything we tried to do to improve safety, cost, quality, or customer service was met with resistance.
When you are in the heat of battle, you don’t realize the toll it’s taking on your health. I was the business unit manager for a vinyl flooring operation for Armstrong World Industries for two years. During that time, we were in a continual state of downsizing. This didn’t help the relationship with our union. It seemed like everything we tried to do to improve safety, cost, quality, or customer service was met with resistance.
Because our business was shrinking, we were under constant pressure to reduce costs. It wasn’t unusual for upper management to threaten your job or to be told if you couldn’t get it done, someone else would be happy to take your place.
I decided the best course of action was to open a dialogue with our shop steward, lay out the situation, and work together to make the best decisions for our employees. For the first few months, he spoke with me, but little changed in our relationship. I was as transparent with him as possible, explaining the business environment and the reasons for the changes we were making. He didn’t trust me. Apparently, prior managers had burned him a few times and he wasn’t willing to forgive and forget what had happened.
We got to a point where traditional operating schedules weren’t practical for the amount of production we were required to make. We needed to make sure everyone had equal opportunity to work full-time, but providing a 40-hour workweek required us to rotate some of our established crews and revise our overtime policies.
I knew I couldn’t do this on my own. It was going to be complicated and if anyone made errors in assigning overtime, we’d be open to employee grievances and back pay. We couldn’t afford that. I called a meeting with the shop steward and my staff. I laid out the situation and my desire to be equitable for all remaining employees (we had to lay off some of our employees, which didn’t improve people’s moods).
In the past, when everyone worked a traditional schedule, overtime was offered by seniority. If the most senior employee didn’t want overtime, the next most-senior employee was offered the opportunity. This continued until someone accepted the overtime assignment. In our new schedule, it wasn’t going to be obvious who should be offered the overtime.
The group argued for a while, and I realized it would be too easy to make a mistake offering overtime unless we came up with a set of rules we all agreed to. I said I’d take a crack at it, and we could meet again to review my efforts.
After much deliberation and advice from others, I developed a table showing the various schedules and twelve situations where overtime might be required. The idea was to check each situation in order and once you found the correct situation, it told you how to assign overtime.
It was complicated, but the team only found a few flaws that would leave us open to grievances. Once corrected, everyone agreed that if we followed it, it would be a fair approach to assigning overtime. Besides, it was so complicated most people wouldn’t understand it well enough to file grievances.
Once our shop steward saw I was fully including him in our processes and wasn’t trying to take advantage of anyone, our relationship changed. Not outwardly to the rest of the employees, as he still had to play the role of “management buster.” But we collaborated often on critical issues.
Five days after I transferred back to a corporate role, I was cutting my lawn. My neighbor came over and stopped me to say, “You look different.” I never realized that all the stress of my job was easily seen by everyone but me.

The Littlest Negotiator
There is always a compromise that can be made. You just must know what you want and figure out how it will benefit both parties. I have been negotiating since as far back as I remember. Sometimes it was bedtime, eating my dinner, or putting off homework to go outside and play. Parents don’t typically cherish those negotiations and kids rarely win (at least I didn’t most of the time).
There is always a compromise that can be made. You just must know what you want and figure out how it will benefit both parties. I have been negotiating since as far back as I remember. Sometimes it was bedtime, eating my dinner, or putting off homework to go outside and play. Parents don’t typically cherish those negotiations and kids rarely win (at least I didn’t most of the time).
I started collecting coins and baseball cards when I was three years old. Early on, I was able to convince other collectors (kids) that what I was offering was more enticing (or valuable) for them than what I was asking for in return. I don’t think it was always true, but it seemed to me both sides were getting what they wanted (or at least thought they wanted).
My uncle Morrie ran Zerns Farmers’ Market in eastern Pennsylvania. We used to visit him and my Aunt Adeline on their “gentleman’s farm” every summer. Uncle Morrie was a shrewd businessman, and he loved to tell stories of the amazing deals he made throughout his career. I was intrigued, and by the time I was eight, I was asking him questions that led him to think that there might be a little entrepreneur he could develop.
He was particularly interested in my love of coins. He didn’t think there was money to be made in baseball cards. This was the 1970s, after all. He told me there were three coin dealers at the farmers’ market and suggested I try to get something I wanted from them at a reduced price. “Never pay full price,” he told me.
He took me to the market and walked with me to the first coin dealer. I had ten dollars to spend. Uncle Morrie asked, “Do you see anything you like?” I told him I did, but I couldn’t afford it. It was priced at fifteen dollars. He said to the dealer, “My name is Morris Lipton, and I run this farmers’ market. I’d like to introduce you to my nephew, Adam.”
The coin dealer told me I could have the coin I coveted for ten dollars. I couldn’t believe it – he took five dollars off of the price. On subsequent trips, Uncle Morrie would walk with me to the coin dealers and encourage me to ask for a better price. I didn’t always get my price, but more often than not, I did. This built my confidence, and I learned how to determine a price that suited me, ask respectfully for it, be willing to hear the word “no,” and know when to walk away from a deal that didn’t suit me.
Eventually, I went to the various coin and baseball card dealers without Uncle Morrie by my side. I think some of them recognized me. But others were willing to negotiate with a child who was confident, respectful, and informed.
To this day, I use the same principles in all my dealings with vendors, suppliers, and customers. I understand when somebody wants to negotiate with me on my services as well. These principles have served me well and I believe they can help you too. Be willing to ask. You are more likely to get what you want if you do.

Go to the Source to Get the Correct Information
I was working at the American Olean ceramic tile facility in Olean, New York as the Industrial Engineering manager when we merged with Dal-Tile. I was offered a position as an industrial engineer at the corporate offices in Dallas, Texas. I was very impressed with the manager who I was going to report to, so I took the opportunity and moved my family south.
I was working at the American Olean ceramic tile facility in Olean, New York as the Industrial Engineering manager when we merged with Dal-Tile. I was offered a position as an industrial engineer at the corporate offices in Dallas, Texas. I was very impressed with the manager who I was going to report to, so I took the opportunity and moved my family south.
When I arrived, I learned our mission was to improve factory environmental, health and safety (EHS) compliance across twelve facilities in the United States. Although there was an EHS department, they weren’t hands-on or helpful for the facility managers. My manager and I would function as internal consultants and help improve the approach, relationships, and overall performance.
I had no prior experience in EHS and attended many workshops and training sessions with the EPA, OSHA, and other agencies. We took tours of every plant and identified areas where we could help. Our focus was on annual safety training and environmental and safety reporting.
Over time, we built strong relationships with plant management at all locations, and they came to trust our work and invited us to help frequently. So much so, I got assigned the submission of the annual environmental reports for all facilities.
There were twelve reports that were all due at the same time. There were different requirements based on the state the facility was located in. Reading through all twelve documents, I noticed many similarities and some critical differences. With one month to go, I created a plan to complete all reports properly and on time. I would be signing each report and would be legally bound for completeness and correctness for the next seven years. I wasn’t willing to take any chances.
The first step I identified was to understand each form. Although I thought I knew what most of the questions meant, I decided it would be better to confirm my interpretations. The best way I knew was to call the state agencies and ask for assistance.
I started making calls, and invariably, was not able to reach a live person most of the time. I left many messages at most agencies. I put a sticky note on each report I had a question on and waited (and waited) for my calls to be returned.
When a call finally came, the first thing I did was ask the person what state they were calling from. Then, I pulled out the report for that state. Looking at the sticky note, I knew what I had to confirm. From there, getting the information was simple. Most state workers were happy to help me fill out their form, beyond my first question(s). They had a vested interest in completeness and accuracy and weren’t used to people asking for help. They were more familiar with fixing problems after it was too late.
I learned that these agencies work for us, the public. But some people don’t see it that way and think they’ll get in trouble for asking questions. I’m convinced it’s the best way to get these critical tasks done and avoid errors. I was able to complete all twelve reports on time, to the best of my ability and knowledge, and sign each document. Many years later, I am confident I provided the proper information to every agency. I also feel better knowing that the seven-year statute of limitations has expired.
Perfection Isn’t Always a Good Idea
In the 1980’s, Thomasville Furniture was the market leader in high-end furniture. They were extremely focused on process improvement in all areas of the business. I worked on a staff of industrial engineers. Each of us supported one or more of the many manufacturing facilities. We were tasked with finding ways to improve safety, quality, productivity, and customer service.
In the 1980’s, Thomasville Furniture was the market leader in high-end furniture. They were extremely focused on process improvement in all areas of the business. I worked on a staff of industrial engineers. Each of us supported one or more of the many manufacturing facilities. We were tasked with finding ways to improve safety, quality, productivity, and customer service.
One of my colleagues worked at the plant that made tables and chairs. They took great pride in the finish of their tabletops. To achieve the desired look, many workers used powered sanding and rubbing devices. It was an extremely labor-intensive process. We had many muscle strains as a result from all the hand sanding and rubbing to get the desired look.
We heard about companies using robots to reduce labor intensity and safety risk. It seemed like an opportunity for us. If we could figure out how to get robots to sand and rub each tabletop, we could realize significant labor cost reduction and eliminate one of our top safety risks.
My colleague, Frank, connected with a robot supplier who brought in some of his robots for a 30-day “test drive.” The first few weeks were spent teaching the robots how to find the surface and perimeter of the table, apply the proper pressure, and cover the entire surface of the table consistently.
Eventually, they were able to achieve their objectives. The robot was able to sand and achieve a rubbed finish on the tabletops, without human intervention. The tabletops looked great. We were ready to roll out robots to take over the sanding and rubbing process.
Before fully committing to the robots, they decided to show the results to a focus group, to get their reactions to the results. The feedback was surprising. Initially, the group loved the finish and look of the tables. In fact, they said the finish was better than anything they had ever seen. But, after more review and conversation, there was something that bothered them. A series of questions drew out the issue: the tops were too perfect. There was no variation across the surface. We had lost the “handmade” look and feel of the furniture. Instead, the lack of variation made the tables look mechanically made, plastic, or unreal.
We couldn’t give up the thing that made Thomasville Furniture a market leader. Frank and his team went back to the robot vendor to see if he could program variability into the process. After many attempts, they gave up. The technology at the time wouldn’t allow the robots to randomize the pressures applied across the tabletops.
The team removed the robots and returned to the time-tested approach to hand sand and finish tables. Over time, robot technology improved, but it was never given another chance at Thomasville Furniture. Instead, we worked on ways to simplify and reduce the safety risk of hand finishing tables.
All Night Long
Admit it. After reading the title of this story, some of you are hearing the famous Lionel Richie song in your head. This story isn’t about that, but rather it concerns a challenging Kaizen event I recently facilitated for CITY Furniture. The business problem we were trying to solve was a series of computer programs that ran after all showrooms closed each evening. There was a period of time where no revenue could be generated through their e-commerce website, until all programs completed their reconciliations. Our goal was to cut the time by 75%, so that we could free up overnight revenue generation.
Admit it. After reading the title of this story, some of you are hearing the famous Lionel Richie song in your head. This story isn’t about that, but rather it concerns a challenging Kaizen event I recently facilitated for CITY Furniture. The business problem we were trying to solve was a series of computer programs that ran after all showrooms closed each evening. There was a period of time where no revenue could be generated through their e-commerce website, until all programs completed their reconciliations. Our goal was to cut the time by 75%, so that we could free up overnight revenue generation.
I’m an early riser and am typically in bed by 10 pm each evening. My wife says I take my “pre-sleep” nap from 8 pm to 10 pm. This Kaizen event would be held overnight, as our Gemba (the work that we needed to see) happened between 9 pm and 1:30 am. I wasn’t sure how I’d be able to make it through the night.
I met with the team leader to prepare weeks before the kick-off. We agreed to start the Kaizen event at 7 pm Sunday and work through the night for four out of five days. Then, we’d take one day off to adjust our sleep schedule and rotate to day shift. Report out was scheduled for 3 pm on Friday.
I normally fly in to Ft. Lauderdale on the Sunday before the Kaizen starts. Due to starting on Sunday, I knew I couldn’t take any chances and had to figure out how to get proper sleep prior to the event. I flew in on Saturday, got some dinner, and went directly to sleep. I woke up in the middle of the night. Somehow, I was able to go back to sleep.
After Sunday breakfast, I did some work, and took a short nap. At 5 pm, I met my team leader. We set up the meeting room and discussed the Kaizen plan. She was excited to tackle this critical business problem and had assembled a diverse team of highly skilled programmers and managers. They arrived at 6:30 pm for dinner. Afterwards, we kicked off the Kaizen. Our sponsor, the chief information officer (CIO), demonstrated his leadership commitment by staying overnight with the team and participating as a full team member.
After getting to know each other and reviewing Lean topics, we walked downstairs to watch a showroom close. We saw so much waiting and paperwork being generated. We knew there was opportunity for improvement. Then, we walked back upstairs to the meeting room and proceeded to watch the computer programs do their thing. It may have been the longest four and a half hours of my life.
The team was enthralled by what they saw and wrote many ideas on Post-its™. It looked like a lot of gibberish to me. I kept telling myself all that mattered was team members seeing waste and opportunities. I had to stay awake at all costs. It would look bad for the facilitator to fall asleep during the Kaizen!
Mercifully, the Gemba walk through the computer programs ended and I stayed awake. Ninety-two minutes became our baseline for the program reconciliations that kept the e-commerce revenue from being generated. Now it was time to Value Stream map the process, identify pain points, waste, and finally, the ideas to reduce the time it took to complete the reconciliations.
The team generated many ideas and picked three they believed would drive the time down significantly and could be completed during the week. We adjourned at 4:30 am Monday morning and agreed to reconvene at 8:30 pm Monday evening.
I went back to the hotel, surprised I didn’t feel sleepy, but that was due to adrenaline. Four hours later, I woke up. I decided to exercise and work on other projects. Then, I took an afternoon nap. Returning on Monday evening, team members were excited to work on their projects. They broke out into three sub-teams and got to their work, which was all on the computer. I felt useless, but they were fully engaged. From time to time, we’d reconvene and share project status and problem solve. On Tuesday morning, the team decided they didn’t need to work through the night anymore and that we’d take a 27-hour break, reconvening at 8 am on Wednesday morning.
Now it was time to reestablish my normal sleep pattern at the hotel. I slept almost as soon as my head hit the pillow at 6 am. I woke up at 10 am. Now what was I going to do? I got up, showered, exercised, and ate lunch. Then, I worked on other things for a few hours. I decided I should stay awake until at least 9 pm. Time went by slowly, but I made it. I went to bed, and woke up around 4 am. That had to be good enough.
Everyone seemed happier to be working in the daytime. Team members felt they were making programming changes that could be implemented by the end of the day. They installed the changes to see how the system would react on Wednesday night. On Thursday morning, we learned the program ran faster than ever previously recorded. Our 92-minute process was now taking 57 minutes, a significant impact to the system. They had more changes in mind that would reduce time, but those would have to wait for the weeks following the Kaizen event.
The report out was well attended, and our sponsor remarked the initial results had saved the company considerable money. The team has implemented a follow-up process, with meetings every two weeks. The time continues to come down and our sponsor is now ready to tackle another critical business problem in his department.
The Sexiest Man in Pensacola
Armstrong World Industries kicked off their Lean journey in 2010. They put a lot of effort into building a culture of Kaizen across their 22 manufacturing locations worldwide. I was sent to many facilities to assist.
Armstrong World Industries kicked off their Lean journey in 2010. They put a lot of effort into building a culture of Kaizen across their 22 manufacturing locations worldwide. I was sent to many facilities to assist.
In 2011, I facilitated a Kaizen event in Pensacola Florida. I don’t recall the topic but I definitely remember the team and the feeling of camaraderie. I followed standard work to guide the team through the week, culminating in a report out to management on Friday afternoon.
Armstrong required every team member to present at the report out. Our teams were comprised of a diverse group of individuals, including hourly production, maintenance, and management personnel. Some team members had never presented to a group, so we practiced our presentations prior to the final report out. We wanted to make things as comfortable as possible.
Most people tend to “fumble” through what their presentation on the first practice run. Then, on the second run, things get easier. By the third practice, they sound confident in telling their story. I was about to find out how their confidence would manifest itself.
During our first practice run, the third presenter said, “my name is Tyler Dare and I’m the sexiest man in Pensacola!” The rest of the team roared with laughter. Everyone else practiced what they were going to say without funny comments. I figured that Tyler was trying to loosen up the team. I felt sure he wouldn’t actually say that in the final presentation.
On our second practice, Tyler reiterated how sexy he was. Then, another presenter said, “I’m Kevin Jones, and I don’t care what Tyler thinks, I’m the sexiest man in Pensacola.” By the third round, everyone was cutting up. I didn’t know what to expect for the final report out. I was just hoping I wouldn’t be fired for having an “out of control” team.
We entered the main conference room. There were at least 25 people waiting for our presentation. In those days, representatives from Armstrong locations around the world called in to hear the presentation. This was before video conferencing was a standard form of communication.
The report out started, and sure enough, Tyler stepped up and said, “My name is Tyler Dare, and I’m the sexiest man in Pensacola.” The audience laughed and clapped. What could I do? Nothing; just enjoy the show! The rest of the team presented their results. They were met with applause. After asking for questions from the audience, a voice on the phone said, “My name is Paul Meyers, and I’m the CEO of Armstrong World Industries. I just have one question. Is Tyler Dare really the sexiest man in Pensacola?”
I almost passed out. There was more laughter, clapping, and congratulations. The team owned their results and had a blast presenting it to their sponsors. From then on, I made sure any team I facilitated had fun presenting their results. If they were nervous, I’d share the story of Tyler Dare, the sexiest man in Pensacola.
My First Process Improvement Project
I graduated from Virginia Tech and went to work as a corporate industrial engineer for Thomasville Furniture in North Carolina. Harriet was my first mentor. She was working on a project to improve the productivity of one of our bedroom furniture manufacturing facilities.
I graduated from Virginia Tech and went to work as a corporate industrial engineer for Thomasville Furniture in North Carolina. Harriet was my first mentor. She was working on a project to improve the productivity of one of our bedroom furniture manufacturing facilities.
I was totally inexperienced supporting manufacturing operations, but Harriet could tell I was curious and interested in helping her in any way she needed support. After a few trips to the plant, she decided to use my help organizing a wood drying and storage facility that supplied the vital materials to the plant. The wood was received from an outside source and had to be dried for a few days before the plant could process it into bed rails, canopies, dresser drawers, and other furniture components.
It must have been over 100 degrees when we took our first walk through the Butler Building (the storage facility). Inside was a massive amount of wood stacked up all over the dirt floor. There didn’t seem to be any organization to it. Two workers were sitting on a stack of wood talking about the latest NASCAR race.
I told Harriet I wanted to spend time in the building and convinced her to let me go “solo” for the rest of the week. The next morning, I showed up at 7 am. The two workers, Sam and Joe, were surprised to see me. I was an engineer who was willing to hang out with them. More than that, I was a “Damn Yankee” from up North (their words, not mine).
I got to know Sam and Joe and followed them around as they did their jobs. Whenever they got a call on their walkie-talkie, they’d jump on their forklifts and dig out requested loads of wood and bring them to the main plant. They dealt with two key problems:
1. The forklifts would dig ruts into the dirt floor, making it difficult and dangerous to maneuver through the building.
2. Different species of wood were stored in the same aisles of the building, forcing the workers to move big stacks of wood to get to what they needed. Oftentimes, it would take many minutes to find the stack of wood they were looking for. Sometimes, the stack would fall over and they’d have to pick everything up and restack it.
At the end of the week, I reviewed my findings with Sam, Joe, and Harriet. They confirmed these two issues were hampering their work and reducing their productivity. Together, we came up with a plan to pave the floor and organize the wood by species.
Within a month, we reorganized the building and paved it. We put up signs on the walls indicating storage locations. I visited the building many times to verify it was helping Joe and Sam do their job more safely and productively.
A month after we paved the floor, I stopped by and asked Joe and Sam if things were still working the way they wanted. They were proud to show me they had made a few improvements of their own that made things even easier. It was a win. Then, they told me that even though I was a “Yankee,” I wasn’t a “Damn Yankee” anymore. Now I was a “Good Yankee.”
The First Area Owner at the Furniture Company – the Story of Abraham
I was facilitating a Kaizen event for a large furniture retailer in Florida. They offer many services that set them apart from their competitors. They have a nice sales and service advantage and impressive customer loyalty. The Kaizen topic we were working on was the use of replacement parts in their process. Our goal was to reduce the amount of replacement parts needed.
I was facilitating a Kaizen event for a large furniture retailer in Florida. They offer many services that set them apart from their competitors. They have a nice sales and service advantage and impressive customer loyalty. The Kaizen topic we were working on was the use of replacement parts in their process. Our goal was to reduce the amount of replacement parts needed.
After Lean training on Day 1, we went out into the Gemba (a Japanese term, meaning the place where the work is done) and saw many areas where parts could be misplaced or lost. There was an area where parts were stored for the entire distribution center. It looked as if it had been hit by a tornado. There was so much clutter that the team knew it would be a high priority project for the Kaizen week. The number of parts and clutter was overwhelming. Would they be willing to put in the effort and time it would take to get things organized?
Three very ambitious team members picked the parts storage area as their project. Abraham, who normally worked in the area, said that they had been working on it for years. He didn’t think they’d be able to do anything to correct the situation, especially in a week. As facilitator, I had to rely on my team. They decided it was so important that they would go for it.
The three team members got help from people outside of the team. By the end of the week, the parts storage area looked like it was brand new. Everything was organized, clutter was removed (at least 75% of what had been stored there), and there were barcode labels on every bin to help manage the parts inventory. They worked many hours beyond the scheduled team hours and refused to stop until they were done.
On the morning of the third day, when we realized that it might be possible to organize the parts storage area, I reviewed “area ownership” with the team. I told them that at my prior company we had area owners who managed things and held people accountable to always do the right thing. Leadership “had their backs” and it made things safer and more productive. I also told them that it took a while to train leadership to behave that way, but once they saw the value of area ownership, they got on board.
Abraham raised his hand and said, “I want to be our first Area Owner.” I was stunned. Here was someone who had been skeptical on the first day and now he was courageous enough to step up and try something new. We were excited for him. The rest of the week we did everything possible to get the area into the best possible shape and designed our system to sustain it, using the Wheel of Sustainability.
The report out at the end of the week was well attended. When we took the leadership team into the parts storage area, you could hear a pin drop – they were blown away. Then, something magical happened. Abraham told them that he was the Area Owner and he needed their help and support to keep the area in its optimal condition. He shared his expectations for himself and for leadership. He showed them how he wanted to be audited on a weekly basis. I was proud of him and the rest of the team.
The area has been working as well as or better than the Kaizen team left it.I now use it as an example of what can be achieved in a short period of time and how well it can be sustained. Many newer Kaizen team members take a tour through the space and when Abraham is there (which is most of the time) he shares his story and tells them how important it is to meet his expectations. He is a model for what’s possible when you take ownership and care about your customers.