
Kaizen Success Stories
Real Manufacturing Results. One Kaizen at a Time
Explore real-world Kaizen success stories showing how manufacturing teams solved critical problems, improved performance, and created sustainable results.
Thomasville’s Frame Nailers – Taking a good idea and expanding its reach
As a young engineer at Thomasville Furniture, I was given project assignments at the discretion of my manager. He gave me ample opportunities to try out different ideas and supported my efforts. I spent many hours in our manufacturing facilities and was fascinated by the complexity of the manufacturing processes. Many of these processes were extremely labor-intensive and required great skill to accomplish. One such task was the assembly of the base frames of case goods, such as night stands, dressers, and other cabinet style products. These frames were the support structure of the furniture and had to be strong and sturdy to hold up to the years of abuse that furniture sees in its lifetime.
As a young engineer at Thomasville Furniture, I was given project assignments at the discretion of my manager. He gave me ample opportunities to try out different ideas and supported my efforts. I spent many hours in our manufacturing facilities and was fascinated by the complexity of the manufacturing processes. Many of these processes were extremely labor-intensive and required great skill to accomplish. One such task was the assembly of the base frames of case goods, such as night stands, dressers, and other cabinet style products. These frames were the support structure of the furniture and had to be strong and sturdy to hold up to the years of abuse that furniture sees in its lifetime.
The process to put together a base frame starts with the cutting of the four individual frame components to the appropriate length. Then, each end of the component is cut with a miter saw at a very specific angle, 44.5 degrees. I asked a skilled saw operator why he wasn’t cutting a standard 45-degree miter. He informed me that the extra half degree allowed for the special nail, glue, and growth that typically occurs in wood when exposed to moisture.
After cutting the miter, a notch was cut at a perpendicular angle to the miter in the center of the ends of the wood. This allowed for a special joining nail to be applied to both ends of the wood. The placement of this notch was critical as well, as any deviation from the center would make the nail noticeable to the customer. Once these cuts were made, the components were brought to the assembly department. Once there, employees would apply glue to the mitered ends, nail the components together, and remove any excess glue. Then, after all components were dry, they were transferred to another department whose responsibility was to put wood putty into any gaps that might be visible in the joined mitered ends. In all, this process took 6 days from original cuts to final putty and cleanup of the frames. As many as 6 people touched the components during this process. The more I watched this process, the more I thought, “There has to be a better way to do this.”
A Simple, But Powerful Discovery
A few months later, all of the engineers at Thomasville Furniture traveled to the International Woodworking Show in Atlanta. This was my first time travelling for the company and I welcomed the opportunity to see all of the interesting machines at the show and tour Atlanta a bit. Each engineer was to look for equipment at the show that might help the plant to which he or she was assigned. The exhibition hall was gigantic and the three days we were there wasn’t enough to properly see everything. Most people liked to look at the biggest, shiniest, most complicated machines that were being displayed. I, however, was fascinated by something I saw at a little booth in an out of the way spot in the exhibition hall.
In the booth was a series of small picture frame nailing machines. They were simple little machines that seemed to be quite efficient at their task. The representative showed me how they worked. Basically, you bring two mitered ends of picture frames together in a jig that positioned them precisely, push a foot pedal, and a pressure plate came down to hold the mitered ends tightly together. Then, a corrugated nail came up from a coil below the machine and was driven into the mitered ends. He handed the assembly to me and told me to try to pull it apart. I couldn’t. Then I noticed how tight the joint was on the assembly. There was no gap, which meant that no wood putty would need to be applied.
I asked the representative if he had a machine that was designed for larger mitered components. He didn’t, but said that he thought he could modify and strengthen one of the machines to drive nails into larger pieces of wood. I asked him how soon he could have a prototype machine. He thought he could have one ready in 4 to 6 weeks. That was all the time I needed to convince one of our plants to try out this new approach. Although I saw many other interesting machines, nothing intrigued me as much as these frame nailers, as most Thomasville plants would have a use for a heavier duty model.
Being Open to a New Process
When I returned from Atlanta, I asked my supervisor which plant he recommended we test the prototype frame nailer. My thought was that if we could convince a plant to try it out, they would get an opportunity to provide input to the design and functionality of the new machine. They would also have the fastest opportunity to streamline their operation. We agreed that the case goods plant 3 miles from the corporate center was the best place to start. We called a meeting with the plant management and gained their support for this work.
Approximately 6 weeks later, a larger version of the picture frame nailer that I had seen in Atlanta arrived at the plant. Two days later, the sales technician joined to show us how to use the prototype equipment. Plant management joined us and watched as the technician joined two large mitered parts with little difficulty. It happened so fast that they wanted to see another demonstration. This time the parts didn’t go together as well as expected. It turns out that there wasn’t enough air pressure applied, and when it was quickly corrected, every part came together precisely and tightly. Everyone was amazed how easy it was and also how tight the mitered joint appeared.
A Solution With Many Applications
Soon, they realized the best benefit of all. There would be no need for applying putty to the mitered joints, as they held together so well, with no gap apparent. This was a breakthrough. But, it was also just the beginning. Then, the technician was asked if this equipment could also create a “Butt Joint.” This is an assembly of two pieces of wood that are joined at perpendicular angles, rather than at a 45 degree angle. These “Butt Joints” we used as intermediate assemblies in case goods and were also quite labor intensive. The technician thought it would be possible, but it would probably need a special jig to hold the pieces in place while the nail was delivered.
Because we were in a furniture factory, we were able to quickly create a prototype jig to try it out. Lo and behold, the two pieces of wood were joined together just as tightly as the mitered pieces. This would save more effort, labor, and time. After identifying a few more modifications, we realized that we had something that we could use in the multiple plants at Thomasville Furniture. We quickly ordered a first unit and set about determining how many others we would potentially need.
For the next six months or so, I was able to replace the old-style miter cutting and joining processes all over the company with the new frame nailing technology. I even was able to find a few more uses for the equipment, which led to more sales for the technician.
I learned a valuable lesson from this work. Sometimes you have a problem that needs a solution, other times you have a solution to a problem you don’t realize you have. You just have to be willing to look for that problem and apply the solution.
A Little Dab Will Do Ya
In 1991, I was offered a line supervisor position at Armstrong’s ceiling grid factory in Franklin Park Illinois. I had been working as a staff Industrial Engineer at Thomasville Furniture in Thomasville North Carolina, so the position would be my first operations supervisory role.
In 1991, I was offered a line supervisor position at Armstrong’s ceiling grid factory in Franklin Park Illinois. I had been working as a staff Industrial Engineer at Thomasville Furniture in Thomasville North Carolina, so the position would be my first operations supervisory role.
I spent my first few months at the plant learning everything I could about the manufacture of ceiling grid and the approach I would take to supervising my small crew of factory workers. The only way I knew to learn was to spend as much time as possible on the factory floor, observing, asking questions, and trying to help where I could.
The factory had eleven separate operating lines and each of them made a variety of products. Each line consisted of an unwind station for coils of steel, roll-formers that bent the coil of steel into the shape of the ceiling grid, and a punch press which stamped out the holes and end details for each piece of grid. Finally, there was a packaging station that assisted the operators as they put the finished pieces in a box.
The lines operated fairly well, with limited downtime, until it was time to change over from one product type to the next. If the shape of the grid was changing, rolls on the roll-former would be switched out. If the size or shape of the product were changing, dies in the press would need to be moved or switched out. The process of changing over was long and drawn out and we never started right up after the changeover. I wanted to know more about this, but typically the highest skilled employees did the changeover and didn’t want to be bothered by my questions.
An Observation In Need of a Solution
After a few months of observing things, I decided that I needed to help somehow. I really wasn’t sure what I could do to help. I decided I would first try to better understand press die setup, as it looked more straight-forward than roll former setup. Spending many hours observing what was happening, I noticed that once the dies were placed in the proper location, they were then tightened using bolts. Then, a bar of grid would be stamped and checked for proper placement of holes, end details, and overall length. Tolerances were tight, so the dies would have to be placed accurately.
Every time this was done, the measurements required that the setup operator make adjustments to the location of the dies. I didn’t understand why this was. Why couldn’t he just find the optimal position, tighten the dies, and be ready to run on the first try? He told me that the dies always moved a bit when tightened and he had to tap them to their final position with a mallet. If things went well, he could do this on one additional attempt. If things went poorly, it could take many attempts which added up to many hours of downtime. I thought to myself, “There must be a way to get the dies set properly on the first try.” I didn’t know what to do. Luckily for me, I was about to take a trip that would change the way I thought about this problem.
I was asked to travel to the new headquarters of our joint venture with Worthington Steel in Malvern Pennsylvania. I like to read bit on airplanes so I looked at the bookshelf in the supervisor’s office and saw a book called, “A Revolution in Manufacturing: The SMED System,” written by Shigeo Shingo. I asked the other supervisor if he had read it and if I could borrow it. He told me that Armstrong bought the book for all of their manufacturing sites in the late 1980’s, but he had never read it. He told me I could take it and keep it if I wanted. So, I took this book with me on the airplane and started reading it.
New Way of Thinking Inspired by Socks
It was like a whole new world had opened up to me. Shigeo Shingo developed a changeover reduction process that is used by companies the world over and even is used during pit-stops at auto races. This was just what I needed. But, where to begin? A story in the book about golf told me what to try first. In the story, Mr. Shingo talks about playing golf and getting blisters on his feet at the end of the day. He loved golf, but didn’t love the blisters that came as a result and decided he must reason out how to eliminate them. He used his problem-solving skills and figured out that the blisters came from the rubbing of his socks on his feet when he was swinging the golf clubs. Why were the socks rubbing on his feet? Because there was less friction between the socks and his sweaty feet than there was between the socks and his shoes, which he had put on quite tightly. How would he resolve this? He figured out that by adding another pair of socks on his feet, he could keep the least friction between the two socks and therefore they would rub against each other, rather than rubbing on his feet. Problem solved; blisters eliminated!
So how does this apply to changeover reduction, you may ask? Now that he saw how reducing friction was beneficial, he decided to apply the same idea to press die setup. He also had a problem with dies moving once they were tightened down. He originally had a bolt and one washer that he used to tighten down dies on a smooth press surface. He noticed that the die would move on the smooth press surface when the bolt was tightened securely. Much like the socks, he decided to add an extra washer to the bolt and put a dab of oil between the two washers, guaranteeing that they would have the least friction of any component in the setup. He tried his idea out and it worked. And now, I had something I could try back at the plant when I returned.
Results Even Skeptics Could Not Ignore
When I got back to my plant, I was excited to share what I had learned with my setup operators. I explained what I had read and they were not impressed. “How do sweaty socks help improve changeover time?” they asked. I said I thought we should try an experiment to see if what I read really did work. One of the operators grudgingly agreed to give it a try. I wanted to make sure that we had real data for our experiment, so I asked him to set up a die in position as he normally would. In this case, we set up dial indicators on two corners of the die. They would be used to show us how much the die moved when tightened to the press. We zeroed out the dial indicators just before he made the final tightening of the bolts on the die. One corner mover .007” and the other moved 010”. That might not seem like a lot of movement, but it is more than we could tolerate and would require him to move the die with a mallet, just as he always had to do.
Now it was time to try the new way. We added a washer to each bolt on the die and put a dab of oil between the two washers on each bolt. We zeroed out the dial indicators just before making the final tightening of the bolts on each die. To our amazement, at the final tightening of each bolt, the washers moved, but the readouts on the dial indicators both read 0! There was no movement of the die. “Let me try that again,” he said, and he did. Once again, there was zero movement of the die. This was a breakthrough. Now the other setup operators wanted to try it for themselves. They couldn’t believe it as one by one each of them saw the dial indicators stay at zero, no matter how hard they tightened the bolts on the dies.
We immediately added washers and oil to the dies waiting to be used on the other lines. Then, we modified the other dies on the production lines after we took them out of the presses following production runs. From then on, every die that was set up in our presses maintained its location, saving valuable time, effort, and reducing frustration. I like to think that I would have figured this out on my own, but I realize that we all get set in our ways and sometimes need a story or two to change our thinking. I don’t play golf, but I now have much greater respect for the game and what can be learned from it.
With Persistence and Desire, Anything is Possible
I started working for Thomasville Furniture out of college as an Industrial Engineer. Born and raised in Maryland and working in North Carolina, I was called “Yankee,” and I had to prove myself worthy every day. I felt like I was up for the challenge. My mother reminded me I was born south of the Mason Dixon line, but it didn’t seem to matter to North Carolina natives.
I started working for Thomasville Furniture out of college as an Industrial Engineer. Born and raised in Maryland and working in North Carolina, I was called “Yankee,” and I had to prove myself worthy every day. I felt like I was up for the challenge. My mother reminded me I was born south of the Mason Dixon line, but it didn’t seem to matter to North Carolina natives.
My first assignment was in Thomasville’s veneer plant. At this plant, many types of veneers were brought together to make beautiful panels used in expensive furniture, more expensive than I could afford. I was fascinated by the labor-intensive process of veneer making, and spent many hours in the plant observing what was going on and asking lots of questions of the workers. They seemed amused by the Yankee who was willing to listen to them.
An Expensive and Inefficient Process
One afternoon, I was in the basement of the plant and watched workers put materials into and out of a hot press. This press was a large, multi-opening machine used to cure and remove moisture from some of the most expensive veneers bought by Thomasville. The machine looked like a large pizza-oven, and had eight openings, one above the other.
I watched a crew of six workers place a large metal plate on a table. After that, they took a “book” of burl veneer – 14 slices from the same log that look generally the same, and spread out each slice on the metal plate. Then, they put another metal plate on top of all of the slices, creating a metal and veneer sandwich. This sandwich fit into an opening of the press. When all eight press openings were filled, a button was pushed, and the press closed on all of the sandwiches. 36 hours later, the sandwiches were removed, all extremely hot, by the same six workers. Now, the workers had to remove the metal plates without burning themselves or damaging the veneer. Heat and pressure had created a vacuum inside the veneer sandwiches, so when the plates were removed, the veneer would fly around and break, as it had become drier and more brittle.
This was the most expensive material used in the furniture and the plant was losing much of it in the course of the curing process. It really bothered me, so one afternoon I decided to talk with the plant manager to see if there was something that could be done.
Avis Tobin worked for Thomasville for many years. He was short, very round, kept a cigar in his mouth at all times, and had the type of loud, gravelly voice that would frighten small children away. I asked him if the “books” of burl veneer could be cured without separating them into single pieces. He responded, “Son, you just don’t know anything about the veneer business. It can’t be done. The veneer would stick together and we’d lose everything.” I wasn’t satisfied with his answer, but it was the most he had ever said to me during my time in the plant.
Opportunity for Change
Six months later, Avis retired and was replaced by a younger plant manager named Bob Ashley. Bob and I developed a strong working relationship over the next few months, as I was able to complete many projects he requested of me. One day, while sitting in his office, I brought up my idea of curing the burl veneer in stacks, rather than pieces. I thought there might be a better way to do it. Bob thought a minute or two, looked intrigued, and placed a call to the veneer buyer at the plant. “Do you have any contacts who cure veneer in the general area?” he asked. The buyer had one in Beaufort North Carolina, which was about four hours from the plant in Thomasville, on the East coast of the state.
Two weeks later, four of us, the plant manager, veneer buyer, truck driver, and me took a truck load of burl veneer to Beaufort to see if we could cure it without de-stacking it. When we arrived at the plant, we saw a piece of equipment we had never seen before: a combination hot press and cold press. The Beaufort plant cured straight grain veneer in this combination press with two people, one loading a conveyer in front of the hot press, the other unloading a conveyer at the back end of the cold press. The stacks of grain veneer would be conveyed into the hot press, pressed for a few minutes, conveyed out of the hot press to the cold press, pressed for a few more minutes, and then conveyed out of the press to the operator.
The stacks of straight grain veneer came out of the end fully cured, with no pieces sticking to each other. Would our burl veneer do the same? We were invited to put a few stacks of burl veneer into the combination press and try it out. We did, and when the stacks came out the other end, most of the pieces of veneer were stuck to each other. We were disappointed. The operations manager for the plant said, “Oh, I forgot to change the heat and dwell time for the burl veneer. It has more moisture in it, so I need to adjust the settings for that.” After he made the change, we tried a few more stacks of burl. Lo and behold, most of the veneer was cured and hadn’t stuck to any other pieces. Approximately 20 percent was still stuck.
A Valuable Lesson
We decided that was all we needed to see. We felt like we would be able to identify the settings required to eliminate the sticking completely. We drove the four hours back to Thomasville with grand plans to change the way we would cure veneer forever. I wrote an appropriation request for approximately $250,000 and bought Thomasville’s first combination cold and hot press. Six months later, it was fully operational. Manned by two operators, we found the proper settings cured burl veneer in one tenth the time of the prior process, with much less scrap and zero risk of being burned. After that, I realized the only limitation to solving difficult problems was preconceived notions of what was possible. If you are willing to take a risk, you may get a breakthrough. I still use this thinking today, as I help Kaizen teams of all sizes and structures worldwide.
Shine a Light on the Problem
The Corporate Quality Manager of a suspended ceiling manufacturer had a problem. When he wanted to check for defects on ceiling tiles, he had them shipped from the manufacturing plant and installed in ceiling grid in the corporate testing facility. This 12’ x 24’ ceiling grid configuration was adjacent to a large bank of windows. He then waited for the weather to cooperate. You see, he wanted the proper angle of sunlight to shine across the face of the tiles, and depending on the time of year and weather conditions, he might have to wait weeks to assess the quality of the tiles. The windows were often obstructed with testing materials, which made access and viewing even more difficult.
The Corporate Quality Manager of a suspended ceiling manufacturer had a problem. When he wanted to check for defects on ceiling tiles, he had them shipped from the manufacturing plant and installed in ceiling grid in the corporate testing facility. This 12’ x 24’ ceiling grid configuration was adjacent to a large bank of windows. He then waited for the weather to cooperate. You see, he wanted the proper angle of sunlight to shine across the face of the tiles, and depending on the time of year and weather conditions, he might have to wait weeks to assess the quality of the tiles. The windows were often obstructed with testing materials, which made access and viewing even more difficult.
The ceiling manufacturer was about to introduce a large quantity of new products and the installation setup would not be sufficient to check all the new products’ quality prior to product launch. A change had to be made. As Lean Champion for the company, my help was enlisted to solve the problem. After some initial discussions and a tour of the area, the Quality Manager and I agreed we needed to think differently about the setup and process of quality testing. We decided to use a Kaizen event to optimize the design of the required testing space.
We assembled a team of testing technicians, quality technicians, scientists, and marketing representatives to think through the testing requirements and systems to install. We also identified a space to use for the new quality testing area. After a few weeks of touring various buildings and negotiating for space, we chose two adjoining 20’ x 50’ spaces on the ground floor of the testing facility. These spaces were filled with equipment and materials from many years of testing and development. We were sure we would be able to remove most of it and re-purpose the space for the benefit of the company. Although these spaces were large, they had no windows to the outside, so we would have to figure out another way to provide proper lighting to the face of the ceiling tiles.
On the first day of the Kaizen, we reviewed Lean principles and spent extra time on 5S. Next, we took the team on a walk of the current testing area and then to the identified spaces. Their first reaction was surprise and disappointment. They thought we should use the existing space by the outside window and reorganize materials and tools.
Our goal was to be able to assess tiles for quality at any time, regardless of the weather. This goal forced us to rule out the current location for testing. In the new space, the clutter got in the way of the team’s vision of what was possible. So, we did the first S, “Sort”. During Sort, the team removed 90 percent of what was in the space. Some equipment, which had been purchased to provide critical data in years past, was no longer useful, and was removed. The team contacted as many of the equipment owners as possible, to ensure we wouldn’t throw out anything critical. Everything would be removed from the space, no matter what.
Once we cleared out the space, we developed our concept for testing. The idea was to create a number of testing spaces, or pods, in which to install and check various types of ceiling tiles. These tiles needed to be at least seven feet off of the floor, so that they could be observed from below as well as from the side, using some form of raking light. The light had to go across the painted face of the tile, so defects and inconsistencies would be readily apparent. The team agreed the size of each pod should be 12’ x 12’. This allowed us to create three pods in each 20’ x 50’ space, for a total of six. We now had three times the capacity of the existing testing space. But, how were we going to create the necessary lighting?
The first thing we had to do was to identify the intensity and angle of light we needed. Fortunately, we were able to do so on the second day of the Kaizen, as the sun came out and provided the necessary lighting required in the existing testing space. Using light meters and the experience of the team, we identified the proper number of lumens (intensity) and optimal angle for the light in the pods.
The next step was to build the ceiling grid configurations in the pods. We put together three installations of ceiling grid in one of the two rooms. Each was squared up and then ceiling tiles were installed. We made sure we had enough space on all sides of the installations, so we could view the tiles from any angle, without obstruction.
Now it was time to go shopping. We purchased enough lights for one of the pods, before committing to all six. We bought a number of different fluorescent lighting configurations (and kept the receipts) to allow us to test and identify the optimal configuration.
On the morning of the third day, we performed our first lighting tests in one of the pods. A technician climbed a scaffold and held one of the lights up to the ceiling tile installation. The team wasn’t pleased. They asked him to move the light a little further away and a little higher. Things started to look better. Then, after a slight adjustment in location and height, they felt they were getting the type of lighting required. Using light meters, they verified a consistent result compared with the natural light measured on day two. The team collected several measurements and developed plans to assemble permanent lighting fixtures for all pods.
Later in the day, the first lighting fixture was installed and the team verified their results. Everything was as expected. Then the team realized an opportunity to provide the same lighting at a 90-degree angle to the original light fixture. They would just need to install an additional fixture and connect it at right angles to the original fixture. This gave them additional inspection capability they never had before.
On the fourth day, the first pod was complete and plans were made to install the same lighting in the other five pods and to hard-wire everything to make it as safe and efficient as possible. Now the team had a new problem. With the extreme increase in productivity and complete elimination of wait time to test, everyone would want to use the pods at the same time.
The solution was to designate an owner for the area and a system to ensure the area was well-managed and organized. To reserve the use of a testing pod, a white board was installed to make reservations visible, by pod. If someone used a pod longer than the requested time, the area owner would follow-up and hold them accountable to honor their commitments.
At the report out, the team proudly reported on their results. They were able to take a process that used to take weeks and reduced it down to minutes. They also increased the capacity of the area by a factor of three. Anyone could now use the pods safely and productively and testing would no longer slow down any new product development or testing project. In the next six weeks, all lights and wiring were installed, and the space has been in continuous use for years.
The team learned how to shine a light on the problem and solve it creatively.
Little Things Mean A Lot
A global consumer goods manufacturer was experiencing high levels of downtime, jams, and long changeovers on a critical production line. They invited Process Improvement Partners to their plant to observe and discuss the problem and identify opportunities for improvement. After reviewing performance, we took a walk to the line. The line was running, and after a description of line components, it became apparent there were quick opportunities to improve performance of the line. The techniques we would use were quite basic: leveling, squaring, aligning, and centering of products with the process. It seemed so simple, and the customers were skeptical. We suggested a five-day Kaizen to improve line reliability, scheduled for January 2019.
A global consumer goods manufacturer was experiencing high levels of downtime, jams, and long changeovers on a critical production line. They invited Process Improvement Partners to their plant to observe and discuss the problem and identify opportunities for improvement. After reviewing performance, we took a walk to the line. The line was running, and after a description of line components, it became apparent there were quick opportunities to improve performance of the line. The techniques we would use were quite basic: leveling, squaring, aligning, and centering of products with the process. It seemed so simple, and the customers were skeptical. We suggested a five-day Kaizen to improve line reliability, scheduled for January 2019.
Leading up to the Kaizen event, we had many discussions with line operators, mechanics, and engineers, and we made several confirming observations on the line. During a discussion with the Plant Manager, it became apparent he didn’t buy-in to the approach. He had used a process called “Center Lining” before, and had mixed results. In addition, it took weeks to accomplish. We assured him centering of the process would be completed on the first day of the Kaizen and then we would optimize all parts of the process around the center in the following days. He was still skeptical, but heard enough and saw our confidence, and gave final approval for the Kaizen to proceed.
In most Kaizen events, we provide a structure and approach to the team charged with solving a problem. We very rarely dictate specific actions to the team. In this case, the entire first day was controlled and team members were asked to follow very specific instructions before implementing their ideas.
After receiving training on the approach, the team walked to the production line. We reviewed safety requirements, shut down the line, and locked it out. The next step was to identify the center of the critical packaging process. This was the part of the line where everything comes together – the product and the package. We told the team everything leading up to the packaging process should be located and optimized to the center of the process. They didn’t think it would be very important, but were willing to learn and find the center of the line.
We located the center of the line at the midpoint of the conveyor frame on the out-feed side of the equipment and wrapped a string around that point. Then, stretching the string through the equipment, we found the center of the conveyors leading up to the equipment. A trained eye can keep the center precise within 1/32”, so we found what we believed to be center along approximately 100 feet of equipment and conveyor and pulled the string taut. Then, we marked the equipment and conveyor every 4 feet along its length to identify center for the process. Once complete, we noticed all product was coming into the equipment off center. The packaging was tracking off-center as well. That was the first time the skeptical team members saw something they weren’t expecting.
Our next step was to check the levelness of all of the conveyors leading up to and through the equipment. Ideally, all conveyors should be no more than 1/32” out of level at every transition (one section of conveyor to the next section) and side to side. Using a torpedo level and some shims, the team documented levelness of every section of conveyor. They found many of the conveyors were out of level by more than ¼” and some were out as much as ½”. The good news was this condition was easily corrected, and by the end of two hours, all conveyors were leveled throughout the process. The team was losing its skepticism as the products ran more consistently once we started the line back up. The first day ended with the team handing the line back over to the production organization.
The next morning, the team came in energized. They heard from the afternoon shift and overnight shift that the line had run smoothly overnight - much better than anyone had expected. We had four more days to improve things before the end of the Kaizen.
The next step was to optimize the location of the product with reference to the center of the process. Now that we had identified the center and leveled the line, this was easy. The challenge was to determine ways to ensure that our new settings would not change as soon as the Kaizen was over. The team was given the freedom to come up with ways to create and sustain the new settings. Using collars, pins, and labels, the team came up with ways to identify the proper locations for all of the different products running on the line. They also identified the product changeover steps (in the order to be followed) and labeled each part of the line with changeover steps that would need to be accomplished in proper sequence. These labels were made with large, bright green stock, so people wouldn’t miss them and forget a changeover step.
One problem the team identified was that the packaging wasn’t wrapping the product in a consistent manner. Upon further investigation, it was determined a top guiding roller was applying unequal pressure to the corrugated wrapper and the wrapper was shifting from side to side. One of the team members came up with a simple solution - tie all parts of the top guiding roller together to guarantee equal pressure across the wrapper. By doing this, the wrapper consistently met the product every time.
Improvements came fast and furious over the final days of the Kaizen, and by the last day, everyone noticed a significant improvement in line performance. The operators on the line thanked the team for correcting years of problems and even offered suggestions to make things better, which the team was able to incorporate into their work.
At the report out, team members remarked they were surprised how extremely small improvements impacted performance. They also realized these techniques could be taken to any other line in the factory. Once skeptics, they become zealots.
Where Is It?
In 2010, the company I used to work for decided to go Lean. They brought in consultants, who taught tools and techniques to employees all over the world. One tool I learned from them was 3P - Production Preparation Process. This technique maximizes creativity of a team by driving their thinking way beyond their comfort level.
In 2010, the company I used to work for decided to go Lean. They brought in consultants, who taught tools and techniques to employees all over the world. One tool I learned from them was 3P - Production Preparation Process. This technique maximizes creativity of a team by driving their thinking way beyond their comfort level.
Because I had extensive experience with Lean and had applied it for many years in my work, the consultants recognized my capability to facilitate and lead Kaizen events that were broad in scope and of high complexity. One consultant, who asked me to co-facilitate a 3P Kaizen, explained each step to me before and during the Kaizen. The team accomplished breakthrough results, but I didn’t fully understand how they got there. A few months later, I was asked to facilitate another 3P Kaizen, with a consultant as my co-facilitator. Once again, using the 11-step method of 3P, we were able to attain another breakthrough. Over the next two years, I used 3P a few more times and facilitated teams to breakthrough results. Something was bothering me, however. I still didn’t fully understand the meaning of the steps and why they were so powerful. I wanted to know more.
After some research, I discovered the inventor of the methodology was Chihiro Nakao, who ran a company called Shingijutsu. I also learned Shingijutsu was hosting a 3P seminar in 2013 and knew I had to go. Knowing it wouldn’t be an easy sell (costing over $6,000), I asked a higher-level manager to join me and convince our company there was immense value in attending. We were successful and made plans to attend the seminar in Muscatine, Iowa.
Shingijutsu’s World-wide 3P/Moonshine competition was a real-world problem-solving seminar hosted by Allsteel, a leading manufacturer of office furniture. Three teams of six were challenged to design, develop, and demonstrate a new chair and the process to produce it - all in one week. Each team had Allsteel members, as well as participants from outside companies. At the end of the week, our work would be judged by our “customers” and a winning chair design and manufacturing process would be selected. The prior year’s winning chair was being manufactured for the first time the week of the competition. This was going to be intense!
All of our movements before, during, and after each day’s efforts were controlled by Shingijutsu. We were picked up at the airport by them, taken to the hotel, met for breakfast, taken to the factory, and taken to dinner and back to the hotel at the end of each day. This kept us laser-focused and also provided the opportunity to get to know them during downtime each day.
On the morning of the first day of the competition, we were given an introduction to 3P and our mission for the week. We listened to expectations of the plant and our customers next. After that, we were split into three competing teams. Each team was assigned a Sensei to guide them through the process and a space to do their work. My team, made up of my co-worker, four workers from the plant, and me, was given a space above the factory floor, on a mezzanine. Our Sensei, Mike, was a retired Boeing employee, who had come out of retirement to join Shingijutsu at the behest of their founder, Sensei Nakao.
Mike quickly started the team on Steps 1 and 2 of the 11-step Nakao method, named after the inventor of 3P. In these steps, team members were challenged to understand the requirements of the customer at the deepest level. In my prior experience with 3P, I typically rushed through these steps, as they were difficult to explain to team members. Now, I realized these steps were foundational and there could be no shortcuts. The idea of 3P is to design the most waste-free product and process possible. If you don’t understand the essence of what the customer is asking for, you will design waste into the product and process. I was starting to understand – the struggle is important and teams should not be shortchanged of the experience. The day ended with my team finishing Step 2.
The next morning, we started on Steps 3 through 6. In these steps, we were challenged to think in new ways about how to solve the problem for the customer. Using nature as the model of efficiency, all of us had to come up with multiple ways nature does what we are being asked to do. Then, we were asked to sketch. This activates another part of the mind and brings out creativity. Next, we were asked to go even deeper into ways to solve the problem.
At this point, team members were engaged, enthusiastic, and excited. My team went to a meeting table to discuss how we would solve the problem. We got a bit loud and the discussion went back and forth. In less than 1 ½ minutes, Mike came over to our table and asked us what we were doing. We told him we were discussing the problem. He immediately stopped us and said to go out and find the solution, not discuss it at the table. I had never been shut down like that before, and I didn’t like it. I stood up and said, “We don’t even know what it is!” Mike said to go find it on Gemba (the real place, the place where the work is done). So, I did what any respectful student would do - I stormed off!
I went downstairs to the factory floor and started walking around the production lines. I was not happy. I didn’t know what I was looking for, but if that’s what Mike wanted, that’s what I was going to do. My mind was racing, I wasn’t focused, so I kept walking around without purpose. After about 20 minutes of walking aimlessly around the factory, I stopped at a production cell and decided to watch what they were doing. In three minutes, my mind started to relax and I was able to focus on what was going on. Ten minutes later, the activity in the work cell got me thinking about possible solutions to the problem we were trying to solve. Now I knew what Mike was trying to teach. The answer is not at a meeting table, it’s in Gemba. Open your mind and you will find the answer. Could it be that simple? The answer is yes!
I came back to the mezzanine, rejoined the other team members and was ready to solve the problem with them. My experience in Gemba reinforced how important it was to follow the 3P process fully, and not take shortcuts. The rest of the week took us through all 11 steps of the Nakao method and by the end of the week we had a new chair design and the manufacturing process to produce it at the required rate of customer demand.
Our team didn’t win the competition, but we all felt like winners. For me, it was mission accomplished. I learned 3P from the masters. I now had a better understanding of the meaning and purpose of all 11 steps. I also knew I shouldn’t shortcut any steps, they were all vital to the success of the process. But, most importantly, I learned the value of going to Gemba. All the answers are in Gemba. You just need to be willing to look for them.
A Tasty Breakthrough
A North American ceilings manufacturer was closing a plant that produced a product no other plant in the division could manufacture, due to specialized, but obsolete technology. They had a customer who was buying millions of square feet of this product annually. They knew they had to come up with an alternative the customer would approve of and keep buying after the old plant was closed.
A North American ceilings manufacturer was closing a plant that produced a product no other plant in the division could manufacture, due to specialized, but obsolete technology. They had a customer who was buying millions of square feet of this product annually. They knew they had to come up with an alternative the customer would approve of and keep buying after the old plant was closed.
The product had a heavy texture and was extremely durable and tough. None of the remaining plants in the division had the capability to produce this particular visual with the same durability and the project team was at a loss to come up with an alternative. They decided to use a Lean technique called Production Preparation Process (3P). They had very little experience with it, but the stakes were high and they were assured a breakthrough could be achieved by using it.
I was asked to facilitate the Kaizen event with help from a consultant and we would use 3P and its 11-step method to drive the creativity of the team to create, test, and develop the new product in a one-week timeframe. Needless to say, there were a lot of skeptical people in the room, including me.
The first few steps of the 3P are designed to remove all preconceived notions of what the solution should be and force the team to define the true essence of what the customer is asking for. Once done, the team identifies how nature is able to meet those customer requirements. This part of the process usually results in the relaxing of inhibitions and the start of laughter and opening of minds to what might be possible. For some teams, it is a true leap of faith that these steps will lead to something useful.
This team consisted of engineers, designers, scientists, and technicians. We had the use of all of the testing and development facilities for the company and any resource we needed was made available to us. Scientists and engineers are typically more analytical than they are free thinking. Once we got to nature, I saw the team was loosening up and they seemed willing to try something new.
Steps 6 and 7 of a 3P require the team members to come up with 7 ways of solving the problem and then trying them out in real time with available materials. This is called “Moonshining”. During Moonshining, the team members started using available materials in the testing and development facility to come up with new textures and strength properties. Nothing seemed to look like or act like what we wanted. A respected engineer with more than 35 years company experience told us he was going on a shopping trip to find what he needed. We all wondered what he would come back with.
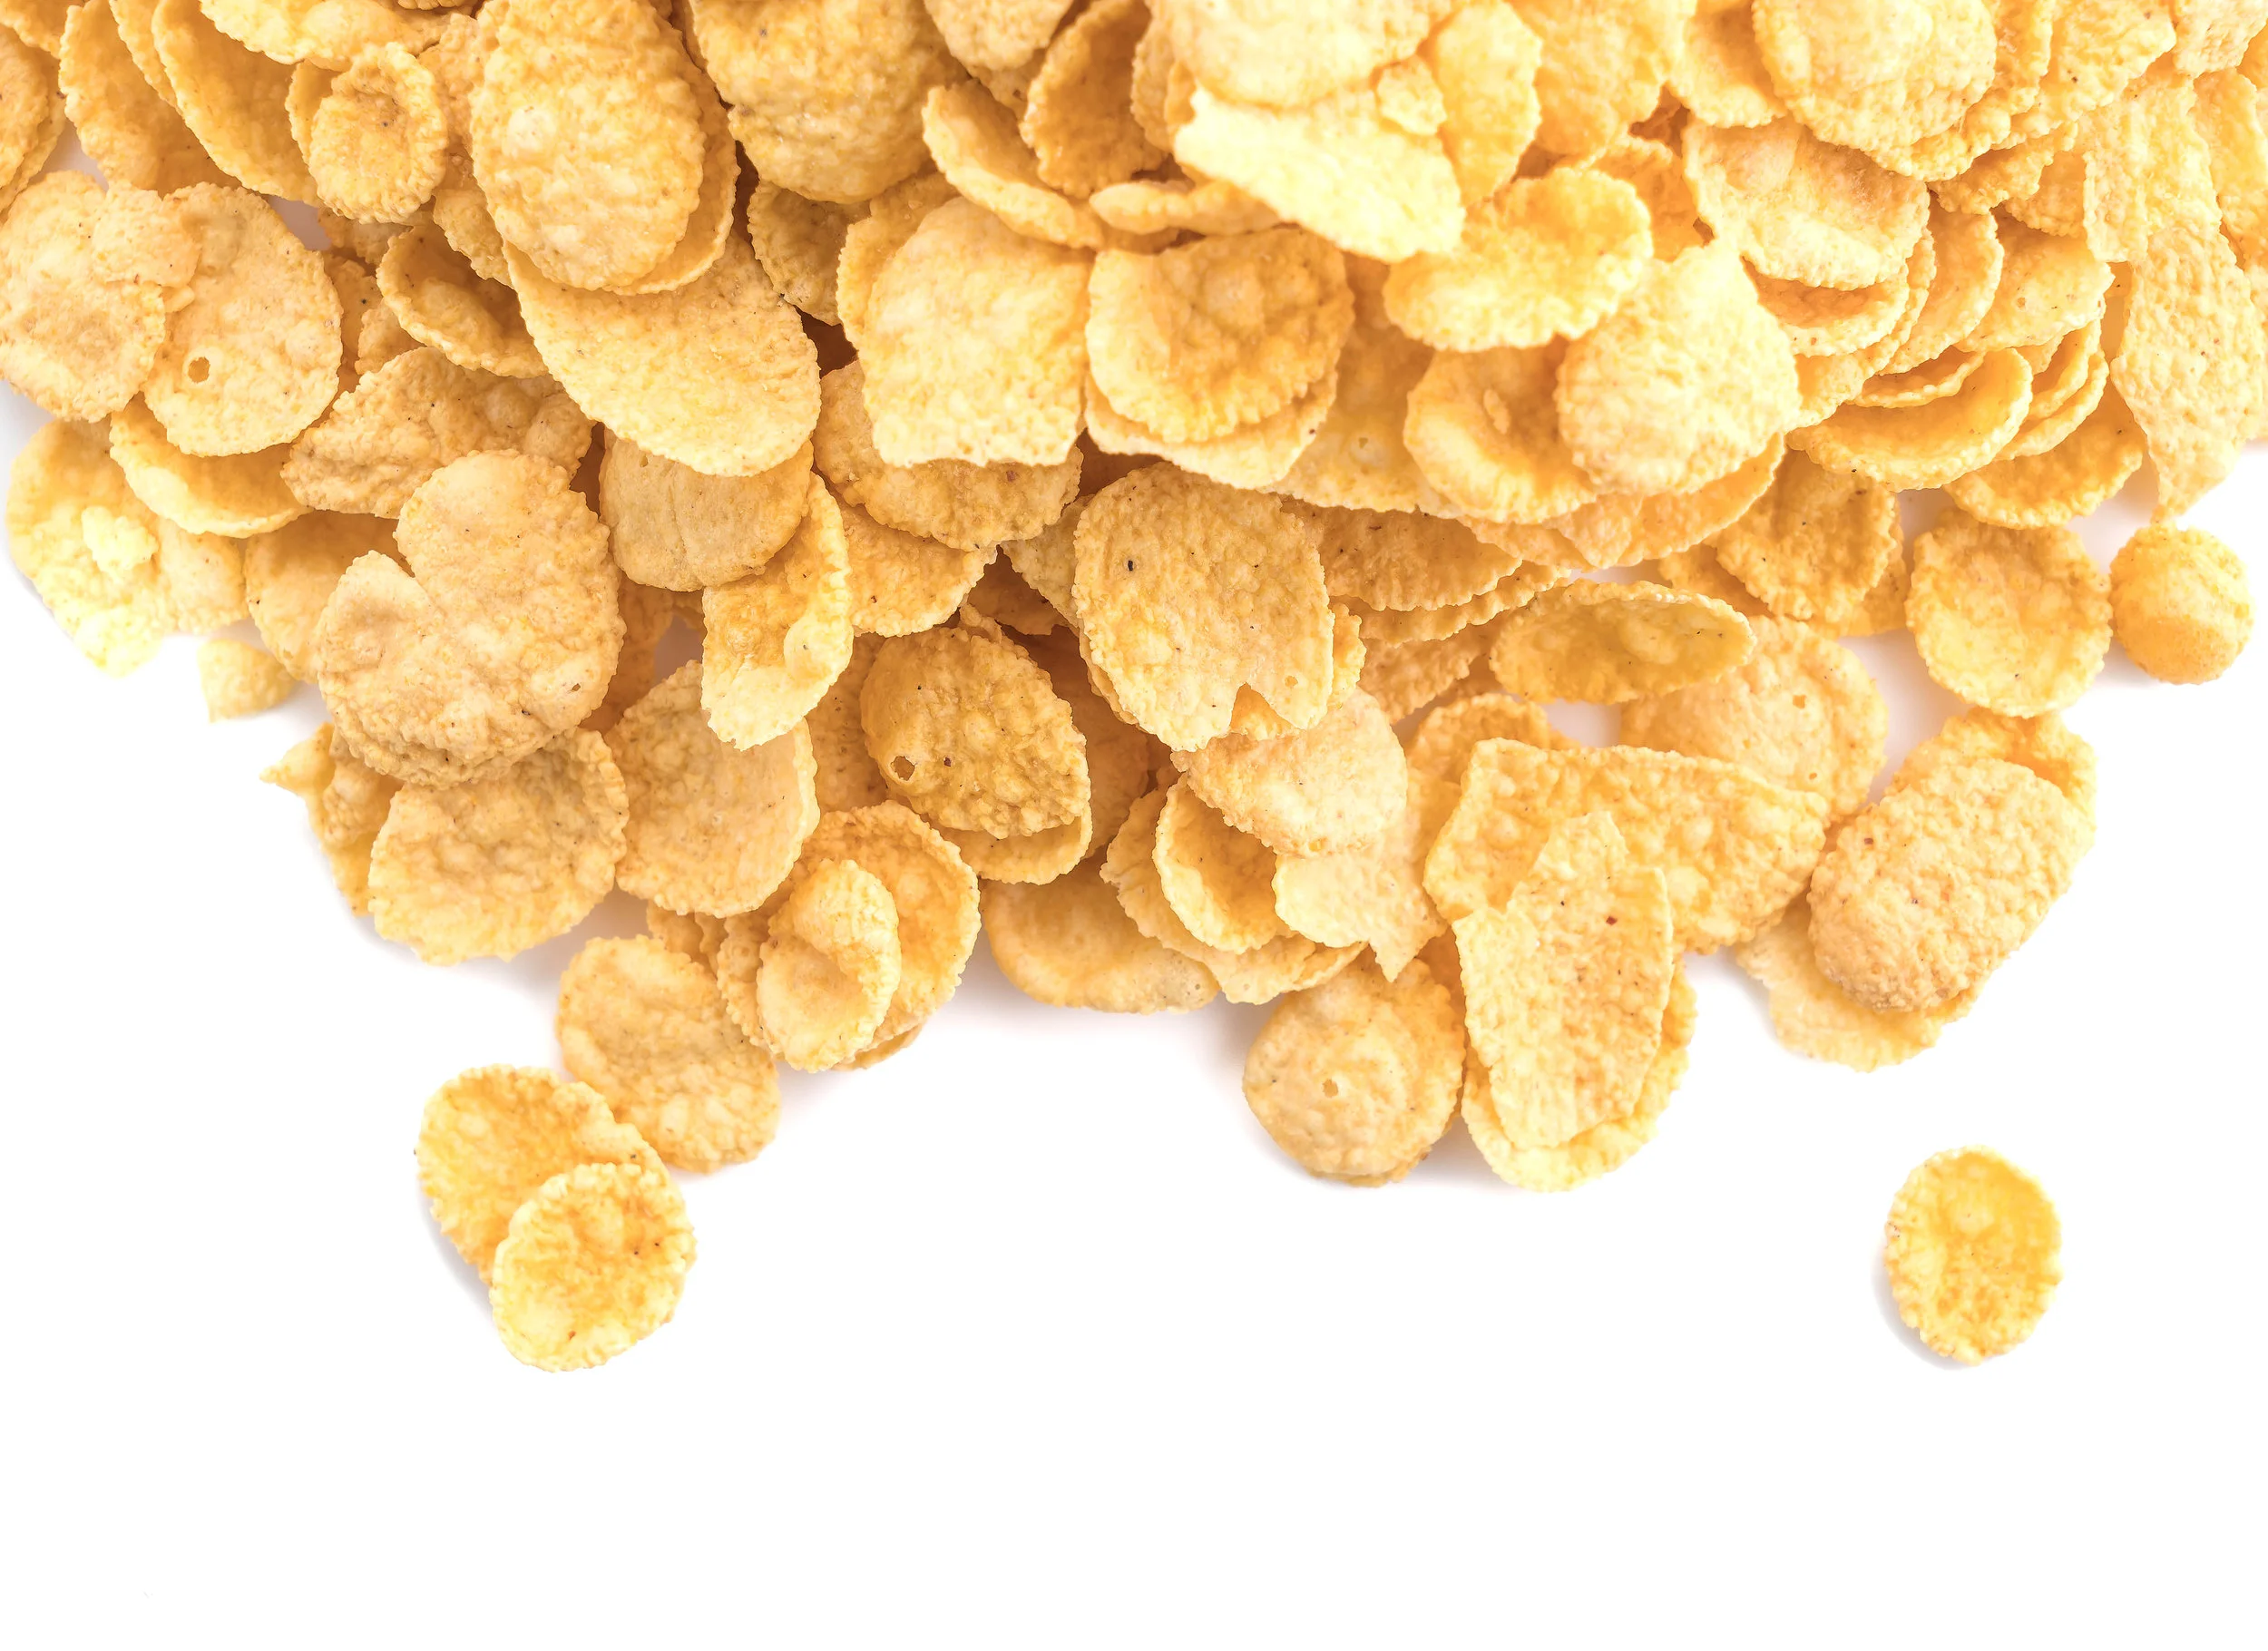
After about an hour, he returned with many different things he bought at a local grocery store, including various cereals, cat litter, salt, and other granular materials. Curious to see what would happen next, we followed him to the testing facility and watched as he poured the various materials, mixed with adhesives, onto boards. Cat litter didn’t look right to him. Then he crushed it, and it still didn’t look right. Next was salt. No good either. Next came cornflakes. He decided to grind them up and poured them on the board. They looked promising. They had the visual texture similar to the customer’s wishes. With the right mixture of adhesives, they might be able to achieve the desired durability. About a dozen trials later, he was able to get a texture and durability the whole team liked.
The team knew it couldn’t use cornflakes in the finished product, but they now knew they could create the proper texture and durability. The rest of the 3P (steps 8 through 11) was spent developing a method to replicate the cornflake texture with materials that could be adhered to the board and painted over in the manufacturing process. At the end of the week, the team was able to provide the overall project team with a concept and method to achieve this new product in an existing manufacturing facility.
Just over a year later, the product was being manufactured in an existing facility, at a reduced cost with better properties than the original product that was manufactured in the closed facility. The customer continues to buy the product to this day, and has no idea that the inspiration for it was found at the grocery store.

Go See for Yourself – The Best Selling Tool There Is
In 2006, our Kaizen team was working on improving changeover time for a painting operation. After reviewing changeover reduction techniques with the team, we took a walk to the line to observe a changeover. The team watched the paint technician clean the front of the paint booth with water for approximately 10 minutes. After that, he walked behind the booth for a few minutes and then came back to work on the front of the paint booth. None of the team members had followed him to see what he had been doing in the back of the booth.
In 2006, our Kaizen team was working on improving changeover time for a painting operation. After reviewing changeover reduction techniques with the team, we took a walk to the line to observe a changeover.
The team watched the paint technician clean the front of the paint booth with water for approximately 10 minutes. After that, he walked behind the booth for a few minutes and then came back to work on the front of the paint booth. None of the team members had followed him to see what he had been doing in the back of the booth.
After the changeover was complete, we asked the paint technician to demonstrate what he had been doing in the back of the paint booth. To our horror, he had to squeeze his body between a post and a wall, make his way to the paint tanks, stand on a natural gas line, twist his body, and reach above his head to open a valve on a paint tank. He told us, “This is the way it had always been done since the plant was opened [in 1990].”
A change was necessary, but the equipment had been installed this way and our small team would not be able to move equipment or automate valves in the short time we had during the Kaizen. We knew we had to sell the idea to the leadership team and identify safety and financial reasons for the change.
Luckily for us, each of the paint booths had some automation built in, so we wouldn’t have to install control systems from scratch. As a team, we decided that if we could automate the opening and closing of the valves on three paint tanks, we could eliminate the need for paint technicians to put themselves at risk while opening and closing the valves. We had an electrical engineer on the team, so while we worked on other aspects of the changeover time reduction, we asked him to develop engineering estimates for the valve automation.
Normally, engineers want to do research and build estimates with high levels of accuracy when they present their findings. But, in the spirit of Kaizen, he was willing to put together a cost estimate with an error of +/- 25% in a day. He came back with the cost estimate and we decided how we would sell our idea to the leadership team.
During the Kaizen, we worked on simplifying procedures, accessibility of tools, and the overall coordination of work by all technicians during the changeover. None of these things cost money, but they reduced the overall changeover time by more than 50 percent. We had accomplished our Kaizen objective.
On the day of the report out, we gave a tour of the new changeover procedure to the attendees. Our hope was to highlight the success of the team and the need for the automation. Eight leadership team members joined us for the report out. We began by thanking them for joining us and then explained the changes we had made. We then invited them to see the new changeover procedure.
We started in the front of the paint booth and demonstrated the simpler procedure. Then, it was time to take them to the back of the booth to see what was actually happening. One by one, they ascended and descended the stairs that crossed over the line to get to the back of the booth. They squeezed past the post and wall one by one. One of the team members showed what was necessary to open and close valves. From the looks on the faces of the leadership team, they were unaware of what was happening in the back of the booth during changeovers. The operations manager said, “we need to automate these valves as our top priority.” Right on cue, our electrical engineer presented the cost estimate and got immediate approval.
Within three months of the Kaizen, the automated valves were installed and a 16-year problem was corrected. If someone had walked the line with the paint technicians when the plant was being built, this issue would have been avoided. The best way to understand what’s going on is to go see for yourself.
The Pursuit of Creativity
In my years of running Kaizen events, I never saw anything as powerful as a creativity approach called 3P – Production Preparation Process. The goal is to eliminate waste in the design of a new or existing process or product in the maximum way possible, unlocking the creativity of the team in ways most of them have not experienced. In 2016 I was fortunate enough to experience this approach through the eyes of the man who invented it, Chihiro Nakao.
In my years of running Kaizen events, I never saw anything as powerful as a creativity approach called 3P – Production Preparation Process. The goal is to eliminate waste in the design of a new or existing process or product in the maximum way possible, unlocking the creativity of the team in ways most of them have not experienced. In 2016 I was fortunate enough to experience this approach through the eyes of the man who invented it, Chihiro Nakao. Sensei Nakao was a former Toyota employee who was sent out to help other companies at the behest of the originator of the Toyota Production System, Taiichi Ohno.
There are eleven steps to the approach, and although they may seem simple or counterintuitive on the surface, they are truly deep and complex and can lead to amazing breakthroughs. A short article will not do this justice, but perhaps it will motivate you to learn more about 3P.
A typical 3P Kaizen event takes 4 ½ days. They are long days, extremely engaging and exhausting, but at the end, the team will have a solution to an important problem that they are seeking. They will also have simulated their solution at a scale that will tell them whether or not it is truly viable.
Background – The team needs to understand certain key Lean principles and terms, such as Takt time, just in time, right sized equipment, and 5 whys prior to initiating the 11 steps of 3P. They also need to know how to use certain tools, such as the Standard Work Combination Sheet and the Fishbone Diagram.
Voice of the Customer – The team needs to hear directly from the customer to understand what is expected from them. There should be a direct exchange with the customer, so there can be no doubt about what is needed. Criteria for the solution is shared, so the team can measure their efforts against the criteria during the 3P.
Step 1 – Determine the Function of the Product or Transformational Step. As a first step, the team must identify what the customer would like them to accomplish in the simplest of terms. They will be challenged to describe this in two words, using a noun and a verb only. For example, a lightbulb does many things, but at its essence, it either “gives light” or “provides heat”. What is the product or process that the customer is most interested in? The team must avoid thinking about what is currently happening, but rather the bare essence of what the customer is willing to pay for, no more, no less.
Step 2 – Define the Essence of the Function Using Keywords. What words are the simplest way to describe what the customer is asking for? The team should generate as many key words as possible and then sketch them out on paper or sticky notes for everyone to see. The act of identifying the key words and sketching them is a way to drive the creativity of the participants forward. Some examples of key words are: drill, shear, guide, roll, and fasten.
Step 3 – Look for Examples of Keywords in Nature. In this step, team members do research and find examples in nature of the keywords. No examples should be man-made. Nature has used millions of years to perfect the simplest ways to accomplish tasks. Again, it is better to draw the examples than just list them. For example, if a key word is grip, then an example in nature could be an eagle’s talon gripping its prey. This step takes time and most team members will initially resist putting great effort into it, but with perseverance, they will make important discoveries about simple ways to perform complex tasks. Each team member should draw at least three examples, so that they expand their thinking beyond what they already know.
Step 4 – Sketch Examples and Examine “What is Happening” to Enable the Function. This next step is to examine in greater detail what allows nature to accomplish the keywords. What causes an eagle’s talon to grip its prey? Team members attempt to attain a greater understanding of the mechanism that is being utilized by nature through research and drawing. More examples are encouraged, as team members dig deep into their understanding and creativity.
Step 5 – Sketch Background and Conditions of the Function. This step takes a deeper dive at the function and the surrounding conditions that allow the function to occur in nature. More than just the eagle’s talon gripping the prey, what is happening with the muscles and nerves in the talon that allow it to grip? What interactions are occurring, and how are they able to do so?
Step 6 – Combine Ideas from Nature and Create Sketches. Each team member is challenged to come up with at least seven ways of solving the original problem using what they have learned from nature and other ideas that they may have. People generally have three alternatives in mind, so getting to seven causes them to think beyond their normal approach and have a bit of fun. It is not unusual to hear laughter during this step as people start to relax their creative minds and let go of their paradigms of what is possible.
Step 7 – Rapid Prototyping (Moonshine). This is the step that brings everything together and turns the ideas into reality. By reviewing, grouping, and prioritizing all of the many ideas shared across the team, the team picks two or three ideas to build. The team should break up into sub-teams so that each idea can be worked on simultaneously. The team is encouraged to use any materials available to them to demonstrate their concepts. The team assesses their prototypes against customer criteria and the
Seven Flows: Flow of People, Flow of Material, Flow of Parts, Flow of Products, Flow of Equipment, Flow of Information, and Flow of Engineering. They learn and improve as they go and are expected to make multiple iterations as they build. This build should be in three dimensions, so it is critical to have enough space and materials for team members to work. The term “Moonshine” refers to the historical practice of building stills in the woods by the light of the moon during Prohibition and using any available materials.
Step 8 – Conduct Trials and Gather Real Data. After building prototypes, they must be tested. Data is collected and compared to the customer criteria. As the comparisons are made, improvements are identified but not yet implemented. Often, the team identifies a better way to approach the problem and plans out the improvements for the next round of prototyping and moonshining.
Step 9 – Select the Three Best Designs Based on Criteria. During all of the prototyping and moonshining, it is not unusual to create variations on the original ideas and have many options to choose from. In this step, the team uses the original customer criteria to score all options and narrow down to three best designs to continue working on.
Step 10 – Continue Simulating and Gather and Evaluate Data on the Top Three Proposals. The team continues to do work on their proposals, learning about them, simulating them, and improving them. Any problems that occur are fixed on the spot, with as little discussion as possible. The act of building rather than discussing expands the creative process. At some point in this step, time will run out, so the team should set a target time to get all information and simulate how their idea will work.
Step 11 – Presentation of Solutions. The team demonstrates to the customer how each option works and shares the data and criteria evaluation. It is similar to a high school science fair, in that the customer acts like the judge and delivers constructive criticism and asks deep questions to the team. Rather than a Power Point presentation, this is a demonstration in 3D, with physical activity, so it’s easier to understand what the team is presenting.
The 3P approach is a highly engaging way to drive breakthrough creativity in teams that have the opportunity to participate. It has been shown to save precious project time and drive cost out of the finished product or process. Some teams saved 6 months in their Innovation cycle time by using 3P. Other teams have said that using 3P revealed viable options that they would never have pursued otherwise. I encourage you to consider this approach and learn more about it.
A Simple Way to Think about a Problem You Want to Solve
Many years ago, I was having difficulty getting my mind straight about a problem that I wanted to solve. A co-worker of mine introduced me to a thing he called a “Task Cycle”. Once I understood it, I had a simple way to go about solving problems and executing tasks.
Many years ago, I was having difficulty getting my mind straight about a problem that I wanted to solve. A co-worker of mine introduced me to a thing he called a “Task Cycle”. Once I understood it, I had a simple way to go about solving problems and executing tasks.
The Task Cycle was developed in the early 1990’s by Paul Boulian and revised by Marlyn Rabenold eight years later. I had the good fortune of meeting Marlyn and was amazed at the simplicity of thinking that can be used to help solve the most complex problems. Now, I want to share it with you.
The Task Cycle has 4 components: Purpose, Products, Process, and Functional Capabilities. It is truly a cycle and can be visualized in this way:

When you are planning a task (or planning to solve a problem), you follow the cycle counter-clockwise, from Purpose to Products, Process, and then Functional Capabilities. When Executing a task, you follow the cycle clockwise and start at the Functional Capabilities and end at Purpose.
Purpose
This is the reason that we are trying to do something, or the problem that we are trying to solve. That seems simple, and it is, but building a clear purpose statement is critical, and should not be taken lightly. As is said, the first step in solving a problem is know that you have one in the first place. When building a clear Purpose statement, consider and communicate why you want to do something, as much or more than what the specific task is. Consider these components of the Purpose statement with this recommended format:
“TO” – describe the task to be done or the problem to be solved
“IN A WAY THAT” – describe the benefit to be realized by the accomplishment of the task. Think in terms of the customer of the task.
“SO THAT” – describe the impact or result the task will have on the organization
Using the experience of writing this article, here’s an example of a Purpose statement:
To write a description of the Task Cycle, in a way that:
- Exposes the reader to a new way of thinking about a task
- Provides a simple construct for dealing with a complex problem or effort
- Engages the reader’s interest
So that this knowledge will help readers in their efforts to solve problems in the future.
Clarity of purpose helps us gain alignment and support from those who will either help us with our task or those who have assigned the task to us.
Now that Purpose has been established, it’s time to move on to Products.
Products
Products are the output or results that we are trying to create when we accomplish the task or solve the problem. A good question to ask is, “If we accomplish the task or solve the problem, what would we see or know that reinforces that the task is complete or the problem is solved?” We aren’t always looking for a physical product, but also non-physical or virtual products. These can be timing, a new way of doing things, or other similar results. Products of the prior example could be:
1. Ten or more responses or inquiries about the article
2. Three shares of the article
3. A phone call to discuss more in detail about the article
Now that the Purpose and Products have been identified, it’s time to move on to Process.
Process
How are we going to get the products that tell us that we have achieved our purpose? What is the methodology or approach that we will use to do this? We can now design a process to specifically accomplish the purpose and deliver the products as stated. Whether we use existing tools and methodologies that we are familiar with, or do research and ask others for their input, we can now test our thinking and approach and see if it delivers the desired results. We want to think through the series of steps and actions that we will take in order to get where we want to go. Because we are clear on purpose and products, we can now design process in a way that has the least amount of effort and waste associated with it.
For the prior example, the process being used is to research the original thinking and documentation on the Task Cycle, consider my personal experiences with it, and try to describe it in a way that the reader can utilize practically. Time will tell if my process was properly thought out.
Functional Capabilities
Do you need people to help you accomplish your task or solve the problem? Do you need tools for this? Are there skills that need to be acquired? What else do you need to solve the problem or complete the task? These are the questions that should be answered in order to identify the functional capabilities needed.
When all four components of the Task Cycle are put together, they should be the foundation for the effort. You should share your thinking with others to see if you have missed any vital elements, always improving as you go. You might even need funding, and that is why it is critical to have alignment around your task cycle.
Earlier in the article, I stated that when you are executing a task or solving a problem, you now go through the task cycle in the opposite direction. What I mean is that you use the functional capabilities to follow the process, which delivers the products and ultimately achieves the purpose.
Although this is not new thinking, I believe that many have forgotten about the Task Cycle and are missing out on this simple way of solving problems and accomplishing critical tasks. I will be interested to see if I accomplished my task in providing you with information that you can use. Your feedback will let me know if I have done so.
What Happens in a Cost Reduction Session?
Most companies want to reduce costs in their operations. There are many ways to do this. Some companies choose to reduce their workforce, others decide to sell off under performing businesses. Companies that use this approach are just avoiding the problems and inefficiencies of their business practices and are not targeting the root cause of their problems.
Most companies want to reduce costs in their operations. There are many ways to do this. Some companies choose to reduce their workforce, others decide to sell off under performing businesses. Companies that use this approach are just avoiding the problems and inefficiencies of their business practices and are not targeting the root cause of their problems.
At Process Improvement Partners LLC, we believe that the best way to reduce cost is to optimize your business to the benefit of your customers. Using that premise, we have developed an approach to leverage your team’s creativity to drive waste and inefficiencies out of your process, thereby reducing cost. In a 2 to 4-day session, teams will identify and build plans to take millions of dollars out of their operating costs, often greatly exceeding their cost reduction targets. The following summarizes how this can be accomplished.
Create Leadership Alignment
The first step in the process is to meet with Operations Leadership to gain their alignment and support for the approach that is being recommended. They have to stand by it, show their support for it, and supply dedicated resources that will participate fully in the cost reduction session(s). They should communicate with all potential participants and their managers well in advance, showing their support for the effort.
Event Preparation
Once Leadership is aligned, the event is scoped out, with a clear problem statement and objectives. When the scope of the event is known, we then plan the amount of time necessary for the team to achieve their cost reduction goal. Critical team members are identified who can help meet the goal, and then the event can be scheduled. All facilities should be reserved well in advance of the event, as meeting rooms come at a premium in most companies. There should be adequate space to move around and enough wall space to display information and ideas on. Typical supplies include flip chart easels, flip chart paper, sticky notes, pens, and a way to project presentations and information.
Session Kickoff
On the first morning of the session, an executive sponsor or key member of the leadership team kicks off the session, reinforcing the importance of the session and the targeted cost reduction that is to be realized. The sponsor should encourage team members to be as creative as possible and not limited by what has or has not worked in the past. It is not unusual for team members to be skeptical that their efforts will not be implemented, so the sponsor should meet that skepticism head on.
Voice of the Customer
Those who will be impacted by any cost reduction efforts must share what is most important to them and their customers. Often, Marketing will represent the customer’s interests, but other areas can do this as well, such as Operations, Research and Development, Sales, and Distribution. Some companies will bring in direct customers and this can be quite powerful. In the end, the team cannot and should not implement any cost reduction ideas that will negatively impact the customer. But, in some sessions that Process Improvement Partners has facilitated, cost reduction ideas created a positive customer experience.
Ideation
This is a free-wheeling exercise. In the early stages of ideation, it is more important to get as many ideas out as possible, regardless of their likelihood of success. Many team members will come to the session with ideas to share, so let’s get them all out on the table. When the team starts running out of ideas to share, facilitators will suggest topics and ask questions to encourage more ideas from the group.
Prioritization
Now that all of the ideas have been shared, the team needs to prioritize the ones that will make the most positive impact on cost, without negatively impacting the customer. There are many ways to do this, but we have used these in most sessions: Group rotation and review of all ideas, grouping of similar ideas, multi-voting with criteria, and a 9-block Impact/Difficulty matrix. The goal is to take literally hundreds of potential cost reduction opportunities and narrow them down to 20 to 30 of the best ones for the team to work on.
Concept Shaping
The team is divided into small groups of 3 or 4 people and asked to build more detail on the top priority cost reduction ideas. A focused, one-page concept sheet template is given to all team members, and they are required to answer all of the questions to the best of their ability. There isn’t a lot of time available, so team members are told that they should take one hour per concept. If they need additional information, they may phone a friend, or make their best educated guess. In all cases, they are encouraged to list their assumptions, so that others will understand their thought process. All concepts are audited for completeness and listing of assumptions, with the view that others who may not have been in the room may be assigned the project later on and must understand the initial thinking behind the cost reduction idea.
Managing System Development
Some teams work on the way that they will manage the cost reduction efforts after the session is over. This can include project communication, resource assignment, project visualization and management, and regular meetings to review status. Other teams just hand off their efforts to the session leader to take the work forward. In all cases, the results of the session should be communicated back to the sponsor and other stakeholders.
Reducing costs in your operation doesn’t have to be difficult or painful. When using people’s creativity and engagement and focusing on ideas that will benefit the customer, opportunities become apparent and a path to realize those opportunities can be identified. Then, everybody wins.
The 8 Deadly Wastes
The customer defines value for any product or service. If they aren’t willing to pay for something, it has no value to them. In the terminology of Lean, anything that doesn’t directly provide value to the customer is called “waste”. Further, there are eight specific types of waste.
The customer defines value for any product or service. If they aren’t willing to pay for something, it has no value to them. In the terminology of Lean, anything that doesn’t directly provide value to the customer is called “waste”. Further, there are eight specific types of waste. Once you know what they are, you can begin to spot them, and then work diligently to reduce or eliminate them. If you do, the customer experience will be improved and so will your operating results.
These are the eight deadly wastes:
Transportation
The movement of anything from place to place is considered waste, because it adds no value to the product or service being provided. It only adds time, and the potential for loss or damage. It may seem necessary to move things around in a process – putting things in trucks, putting things away on shelves, sending electronic data from one server to the next, but there is no change to the form or function of the thing being produced. The question to ask is, “how can we reduce or eliminate transportation in the process?”
Inventory
Ideally, the only product you should produce is the product that your customer wants; no more, no less. More production creates inventory. Less production creates a shortage. The risk of having too much inventory is that it may spoil, become obsolete, or never leave the shelf. Think about computer chips. Once the new version of computer chip comes out, who is buying the older version? Typically, nobody, or if they do, they are receiving a sizable discount. Another problem with inventory is that the thing you need may get lost behind the thing you don’t need. So, you end up producing more inventory that can hide the next thing, and the cycle continues.
Motion
This waste addresses the effort required to complete a task. If you must reach over your head, or grab something from the ground, you are using extra motion. If you must go away from your area to track something down and retrieve something, you are using extra motion. Ergonomics, which is the study of people’s efficiency in their work environment, is a method to identify and reduce excess motion.
Waiting
Time lost while waiting for an answer, a return email, an earlier process step, booting up your computer, or general waiting around is considered waste. It can be frustrating, time consuming and adds to the overall time in the process, which delays delivery to the customer. The key is to find the things that force you to wait and strive to eliminate them. Empowering people to make decisions is a quick way to drive waiting time down.
Overproduction
Have you ever noticed people who print out every email that they receive? This is an example of overproduction. How about a production line that is running really well and the managers want to keep things running? While the current product gets produced, the next product waits. There is a risk there will be a shortage of the raw materials to make the next product, or that there will be a delay in shipping the next product to the customer.
Overprocessing
This waste refers to the complexity in the process. If there are more steps than needed, or if the product or service is delivering beyond the requirements of the customer, this can be thought of as overprocessing. In the 1930’s, there was a cartoonist named Rube Goldberg, who devised the most complex ways of completing simple tasks. It was entertaining and creative, but not the ideal way of accomplishing work.
Defects
When the product or service doesn’t deliver to the required level of quality, this is considered a defect. When something has to be reworked, this is considered a defect. Many companies try to instill a culture of “Doing it right the first time.” They want to ensure that each process step will continue adding value to the benefit of the customer.
Unused Employee Creativity
The people who do the work generally have ideas to make their work simpler and safer. The best companies listen to their employees to get improvement ideas. Other companies think they know all of the answers and ignore suggestions by their employees. We don’t want people to shut their minds off when they come through the door, or we will be responsible for the worst waste of all.
In order to reduce or eliminate waste, you must be able to identify it. These eight wastes are easy to find in any process, if you are willing to look. If you make it a habit to reduce or eliminate these wastes, your customers will benefit. If your customers benefit, so will you.
Value Stream Mapping: The First Step on Your Continuous Improvement Journey
You can’t reach your destination if you don’t know how to get there. Maps, or in our technology-driven world, GPS systems, are critical resources for guiding you from point A to B. The same is true for your continuous improvement journey. Unlike your GPS, however, you must build your map through learning. The best way to build it is with Value Stream Mapping.
You can’t reach your destination if you don’t know how to get there. Maps, or in our technology-driven world, GPS systems, are critical resources for guiding you from point A to B. The same is true for your continuous improvement journey. Unlike your GPS, however, you must build your map through learning. The best way to build it is with Value Stream Mapping.
Value Stream Mapping views everything from the eyes of the customer. Anything that the customer would not pay for is considered Non-Value Added and is waste. The key to Value Stream Mapping is to see the waste in the current process and then develop strategies to remove as much waste as possible, delivering maximum value for the customer.
There are the 8 key components of Value Stream Mapping:
Identify the Value Stream to Map
What is the family of products or services that the customer is willing to pay for? Often, companies will pick a product or service that represents a significant portion of their overall demand or represents most of the process steps. It is better to pick a simpler process the first time Value Stream Mapping is attempted, increasing the complexity of processes to map as experience grows.
Build the Team
The members of the team are critical, as they will learn together and become supporters of the work going forward. The team should be diverse, comprised of people in the process, people who manage the process, customers of the process, and suppliers to the process. It can be beneficial to add a few team members who have no relationship with the process, as they provide “outsider” thinking and can challenge the team during the session.
Voice of the Customer
What is most important to the customer, from their point of view? Often, companies will engage Sales and/or Marketing to represent the customer, based on interactions they have had while dealing directly with customers. It is more powerful to invite direct customers to these sessions, but it can also be risky, as they will see some of the waste or inefficiencies in the current process. Most customers appreciate the opportunity to participate in these sessions, and the rewards far outweigh the risks.
Walk the Current State Value Stream
This is typically the most “eye-opening” part of Value Stream Mapping. The team should leave the meeting room and physically walk the process from the last step to the first. If they are mapping a physical product transformation, the team starts at the shipping dock, and then works their way back to the receiving dock. Start with the customer and what they are expecting to be delivered, then work your way back to the beginning of the process. All the while, the team is looking for waste and inefficiencies. They should be taking notes, pictures, and engaging with each other and others working in the process to fully understand what is going on and why things are working or not working as expected. If the process is virtual, the team should be demonstrating the steps of the process as they occur. Do not discuss the process in a meeting room. Go see what’s actually happening.
Gather data for the Current State Value Stream
How long does each process take? How many resources are needed for each step? How much inventory or waiting occurs at each step? How is information communicated to each step? How long does it take to change from one product or service to the next? How much space is required by each step? There is so much data that can be gathered, that you have to be careful not to do too much and miss the simplest and most impactful opportunities in the Current State.
Map the Current State Value Stream
Once the team returns to the meeting room, they map out all steps and interactions between steps of the process. This is a team activity, so don’t let just one person do all of the work. Each team member can take a pack of sticky notes and write down steps, placing them in order on a wall or something similar. Next, the team should measure the total time it takes for the product or service to get through the Value Stream, measuring the value-added time, non-value-added time, and lead time. Don’t use a computer, this is a visual activity, and most “A-ha” moments occur while placing steps on a wall and seeing how inefficient the current process is. Don’t be surprised if less than 10% of the time is value-added. In many manufacturing plants, that number drops below 1%. One key point is to map the process as it is, not how you want it to be.
Build the Future State Map
The team develops a vision of what they want the process to be in the future, for the benefit of the customer. By seeing the waste and inefficiencies in the Current State Map, the team imagines what the process would look like if they minimized or eliminated non-value-added steps, inefficiencies, defects, safety issues, and other waste in the current process. After the map is created, the team recalculates the value-added time, non-value-added time, and lead time in the future state. It is not unusual to drop the overall lead time to the customer by 50% or more. It’s also not unusual to identify quick, simple activities to accomplish this lead time reduction.
Create a Plan to Achieve the Future State
The team builds a roadmap of activities and strategies to make the changes required to drive to the Future State. These activities are typically low-cost and quick to implement, but some activities require an entirely new way of leading and managing the process. The team develops the action plan, with owners, due dates, and the managing systems to ensure that the work gets done.
A typical Value Stream mapping session takes between 3 and 4 days. When it’s over, everyone knows their new destination and how they intend to get there. Now, leadership has identified what is necessary to take the journey. Just like any journey, you must take the first step. Value Stream mapping is that first step.
How to Drive Teams to Success with Effective Facilitation
The best facilitators look like they’re doing nothing at all. The team is driving toward a solution, being creative, working together, and having fun. What’s the facilitator doing, just taking credit for the team’s hard work? As it turns out, the easier it looks, the harder it is.
The best facilitators look like they’re doing nothing at all. The team is driving toward a solution, being creative, working together, and having fun. What’s the facilitator doing, just taking credit for the team’s hard work? As it turns out, the easier it looks, the harder it is. But, if you use these techniques, you have a chance to look like you’re doing nothing, and doing it really well!
1. Stick to the charter.
This is the reason the team got together in the first place. Make sure all activities are conducted within the scope of the charter. It’s very easy to get off-track, or work on things that aren’t explicitly in the charter. The team should be reminded and guided back to the charter. An easy way to do this is to share a copy of the charter with every team member and have them read and discuss it at the appropriate time(s). They should be able to recognize if they are veering away from the charter.
2. The team solves the problem, the facilitator guides them to the solution.
Keep the roles separate, as the team will sometimes want the facilitator to give them the solution. This is not a good idea, as the team must own the solution and will not if they didn’t come up with it. The facilitator is responsible to come up with a solution path for the team, not the actual solution. There are times when a facilitator may have to provide direct help, but this should be rare, and only used as a last resort.
3. Everyone participates with an equal voice.
It’s very easy for some team members to dominate conversations, but in doing so, other team members may not have an opportunity to share their ideas. When this happens, there is no true consensus or full support for the solutions developed. Great care must be taken to give every team member an equal voice. One technique to do this is to give everyone a pack of sticky notes and let them write their ideas down, one per sticky note. Then, they share one idea at a time, one person at a time. Place each sticky note on a flip chart for everyone to see. Be careful not to let a team member share more than one idea before another team member gets a chance to share.
4. Keep the team moving.
I mean this both mentally and physically. If team members sit in one place too long or spend too much time on one topic, they will get bored, disengaged, and lose momentum. Get the team members out of their chairs, moving around the room, or out of the room. Break up activities into small chunks, so that there isn’t a chance for complacency or boredom. This tests the facilitator’s creativity, but it is vital for positive momentum and progress.
5. Time is precious. Break down barriers to progress.
Sometimes the team is looking for an answer and the expert is not in the room. A good facilitator will challenge the team to get the answer from someone else, in a different way, or by some quick estimate. In extreme cases, the facilitator will encourage the team to interrupt a meeting to get the answer they need. In even more extreme cases, the facilitator will get the answer for the team by interrupting a meeting or going to a higher-level leader for an answer.
6. The more ideas the better.
When a team is thinking up ideas and alternatives, their first ideas are typically things they are most comfortable with or don’t challenge them. Facilitators should drive the team to think of things that haven’t been tried before. The first step this is to ask team members for more ideas. Most people can come with 3 alternatives for almost anything. Ask for 7 in this case. If the team has stopped writing ideas, ask questions in as many different ways as possible, pulling more ideas out of the team. When we challenge ourselves, we are more often able to deliver breakthroughs.
7. Don’t let best get in the way of better.
We want teams to make improvements. Sometimes team members want things to be perfect before trying their solutions. The problem with this is that nothing is perfect and if we wait to have everything perfect, we will never test our improvement(s). So, the facilitator should encourage team members to try their ideas out before they are fully designed. It’s perfectly acceptable to make mistakes, as long as we learn from them and improve upon them. I tell teams to shoot for 60% confidence. It gives them more opportunities to try things quickly.
8. Use frequent check-ins of progress.
Once team members start working on their improvement projects, it’s easy to assume everything is going as planned and issues are addressed when they arise. However, that’s often far from the case. Team members often get stuck and struggle on their own until time runs out, if left to their own devices. Frequently connect with the team to check on their progress and determine any areas needed support. I have found that 1 ½ hours is about the maximum amount of time that team members should work independently before coming back together to share their progress. This is also a way to integrate efforts of different team members and eliminate duplication of efforts.
9. Teams that are having fun will accomplish more.
People like to win, laugh, have fun, and share in success. As a facilitator, you should be looking for ways to help the team win. Find activities that will make their time spent together engaging and fun. You may even need to develop team activities that help them work together better.
10. Less you, more them.
The reason the team was brought together was to solve a problem. If you had the answer to the problem, you wouldn’t need a team in the first place. A good facilitator will encourage as much participation from the team as possible by asking probing questions and creating a participatory atmosphere. Once the questions are asked, you must allow the team answer to them, not you. Often, they will want an answer from the facilitator, but you must resist the temptation. This is their effort, not the facilitator’s, so it’s best to let them struggle through hard questions.
These 10 facilitation techniques take practice, but they will help you get the best out of the teams you are working with. Take pride in knowing your teams solved their problems and it appeared you did nothing at all to help them!
How to Organize Your Work Space With 5S
In the world of Lean Manufacturing, 5S is used to organize workplaces to make them safer and more productive. Although many great manufacturing organizations and others have been credited with inventing or popularizing 5S, I’m pretty sure my mom invented it.
In the world of Lean Manufacturing, 5S is used to organize workplaces to make them safer and more productive. Although many great manufacturing organizations and others have been credited with inventing or popularizing 5S, I’m pretty sure my mom invented it.
When I was young, I wasn’t very organized. My mother told me, “pick up your clothes,” “put your toys away,” “make your bed,” and most importantly, “there’s a place for everything and everything in its place.” Not only did she tell me to do these things, she showed me how to do them, nagged me about them, and checked my work quite often. I couldn’t get away with anything!
Although I really didn’t heed my mother’s advice as a child, as I grew older, I came to realize how powerful these statements were. When I entered the working world, I started applying 5S to many different situations and was amazed at the immediate positive impact that I was able to make. I also saw how deeply it moved those that were able to participate in 5S efforts. They became disciples of the effort and wouldn’t allow others to erode any of the benefits of the change.
As simple and powerful as 5S is, there are many who don’t understand what it is and how it should work and use it to just “clean things up.” I would like to share my understanding and approach to 5S and try to clear up some of the confusion.
The first thing to understand is the purpose of using 5S. I believe 5S should be used to improve the safety and productivity of an area or work space. Once agreement and alignment around this purpose has been established, the team will make choices that will benefit the users of the area.
The first S, Sort, tells us to remove anything that is not immediately needed or useful in the area. Duplication, clutter, and non-working things are to be removed, discarded, donated, or sold. Three hammers turn into one, broken things are repaired or replaced. Things that were saved, “just in case,” are no longer allowed in the area. It’s not unusual to take away more than 70% of the tools, materials, documents, and other things that were just getting in the way. Productivity is improved by reducing the time and effort required to find what’s needed. Safety is improved, as you no longer have to move clutter out of the way to get to what is needed.
Set in Order, the second S, says to create visible, easy to find locations for all remaining materials, tools, and equipment in the area. Define proper inventory levels, place things within reach, make it impossible to lose anything or put it away improperly. As Mom said, “A place for everything and everything in its place.” Trip and bump hazards are eliminated in this step, greatly improving safety. Productivity continues to improve as it becomes difficult for anyone to be non-compliant to the system requirements.
The next S, Shine, tells us to clean and inspect everything that remains in the area, to ensure that it is in optimal condition. We are trying to prevent problems before they happen by identifying any issues, cracks, leaks, or poor performance that may occur with our tools, equipment, documents, and other things that help us do our work. Some think that Shine means “clean things up.” I believe Shine is much more powerful than that, as this effort can reduce risk of failure, greatly improving productivity. Safety is enhanced because we can rely on everything to work properly when called upon, creating no surprises.
The fourth S, Standardize, tells us to create expectations and audits to involve everyone in keeping things as they should be. No longer is it the responsibility of just one person, but the greater community. When I work in an area, I may not realize that things are shifting to their prior condition, things are starting to return to the area that were previously removed, or people aren’t putting things away properly. With a series of audits and auditors, there is a better chance to catch issues quickly and hold each other accountable to follow the rules of the area. In context of my childhood, I thought my room was OK every day, but Mom didn’t always see it that way, and often pointed out the error of my thinking. The safety and productivity gains are maintained through the commitment of the community and its auditors.
The fifth and final S, Sustain, challenges us to continually improve the performance of the area. By scoring the performance of the area and tracking it for everyone to see, we can identify further improvements that would enhance the safety and productivity of the area. Once an area has seen the benefit of implementing 5S, it is not unusual for people to see other things in the area that could become part of the overall 5S system.
I think we can all agree that being organized is beneficial. I think we also can agree that we should listen to our mothers more often. Because I don’t like my vegetables, I can’t guarantee that I will do everything that mom tells me, but I will definitely do my best to listen more.
Three Tips in Preparation for a Successful Improvement Event
Improvement Events are used to bring teams together to solve critical problems in a fast, engaging, and sustainable way.
Process Improvement Partners LLC was founded to help teams achieve breakthrough improvements in safety, quality, customer service, and productivity. Improvement Events are used to bring teams together to solve critical problems in a fast, engaging, and sustainable way. These Improvement Events, also known as Kaizen Events, can vanquish problems forever when they are done well. Preparation is a key component for success. In the spirit of helping teams achieve the best possible results, here are three tips to help you successfully prepare for an Improvement Event:
1. Develop a Strong Charter for the Event
At least 4 weeks before the Improvement Event, the Leader, Sponsor, and Facilitator of the event should come together and align around a charter for the event, which asks these four questions:
Problem - What is the problem that the team is being asked to solve? Why is it a problem, what is the impact of the problem on the business or the customer(s), and what would happen if the team could solve the problem?
Objectives - What are the objectives of the Improvement Event? What are the measurable results to be achieved? What would be the tangible evidence be that would show that the problem has been solved?
Team – Who are the people who can help solve the problem during the Improvement Event? Who has the interest, enthusiasm, and creativity to come up with potential solutions in a short period of time? Who can facilitate this event, to help the team on its way to a solution? Who will lead the team?
Output Owner – When the Improvement Event is over, who is responsible to implement the solutions developed by the team? Who will make sure that changes are properly communicated? This Output Owner should ideally be the Team Leader, as they will only agree to solutions that can implement and support.
Once the charter has been agreed to by the Leader, Sponsor, and Facilitator, the team is empowered to develop and implement their solutions to the problem that they are asked to solve. There is no need to gain approval for their solution after the Improvement Event. They are encouraged to get input and feedback during the event, to ensure that they have considered all aspects of the problem and potential solutions.
2. Create Leadership Alignment and Support for the Event
There should be an Executive Sponsor for the Improvement Event. This is the person that believes in the value of the event, supports the efforts of the team during the event, will remove roadblocks during the event, and will deal with resourcing issues that come up because the team members are being asked to fully dedicate their time to the event. The Executive Sponsor should communicate directly with the managers of each team member to gain their support and commitment to clear the calendars for their direct reports. Each team member should give their full focus and attention to the Improvement Event.
3. Plan Proper Facilities and Food
An Improvement Event is special. We are asking people to set aside their normal work and focus on a critical business problem. As such, we need to provide the proper food and facilities that will help them stay focused and engaged. Bring in morning and afternoon snacks, and feed the team lunch in their working space. If they stay together, they are more likely to stay focused on the problem at hand. If they disperse during lunch, they may get distracted, lose focus, or get drawn in to other business issues.The meeting space(s) should provide adequate space and privacy from outside distractions. There should be enough floor space and wall space to allow the team to try out and display their ideas and solutions. Improvement Events are interactive, visual, and energetic. People need to be able to move around freely and safely. If they need to use computers, there should be adequate power outlets available in the meeting space(s). Finally, they should have access to any resources necessary to solve the problem. Don’t move the team off-site if they need access to others in the company who may have vital information to share.
As you plan your next Improvement Event, keep these three tips in mind to give your team the best chance for success. The investment of time and effort will paid back many times over.