
Kaizen Success Stories
Real Manufacturing Results. One Kaizen at a Time
Explore real-world Kaizen success stories showing how manufacturing teams solved critical problems, improved performance, and created sustainable results.
Saving Is Not Saving
We were building a ceiling tile manufacturing plant in Russia. Like most projects, the engineering team was directed to save money, as long as it didn’t negatively impact safety or productivity. As most were unfamiliar with doing business in Russia, they used their experience with known vendors to acquire equipment for the plant. If there wasn’t enough capacity to fill equipment needs, the project team worked with local consultants to identify the “best” options for equipment purchases.
We were building a ceiling tile manufacturing plant in Russia. Like most projects, the engineering team was directed to save money, as long as it didn’t negatively impact safety or productivity. As most were unfamiliar with doing business in Russia, they used their experience with known vendors to acquire equipment for the plant. If there wasn’t enough capacity to fill equipment needs, the project team worked with local consultants to identify the “best” options for equipment purchases.
A few years earlier we had shuttered a plant in Alabama. Equipment was stored in the hopes it might be used for future projects. The project team identified equipment they thought they could use and had it shipped to a contractor, who was responsible to inspect it and bring it up to optimal operating condition. This was done to save more than $1 million for the project.
Two weeks before plant start-up, I traveled to Russia to assess and optimize the flow of ceiling tiles through the new production line. I had done this work many times in other manufacturing plants and was known as the flow “expert”.
When I arrived, I was assigned a team of two mechanics and one production operator. We were going to send ceiling tiles through various parts of the line and make adjustments and corrections where necessary to improve the flow.
Very few tools were available for our use. I packed string, levels, and flat steel bars to help us with the work. Our initial assessment and work through the line went smoothly. We identified conveyers that were out of level, causing the ceiling tiles to skew and jam. Fixing these problems was simple enough. Soon we had tiles flowing smoothly through the first half of the line. Until we reached the equalizer.
The equalizer is a large panel saw. Its purpose is to cut ceiling boards into finished ceiling tiles. The board goes through a first set of saws, strikes a transfer, and then is driven through a second set of saws positioned at a right angle.
Boards were going through the saws at an angle. Instead of tiles looking like rectangles, they looked like trapezoids. They weren’t going to fit into ceiling grid that way.
There were many possible reasons for the angled cuts. After resolving many issues, the tiles still weren’t correct. What was going on? Normally, fixes happen independently of the saw assemblies. Saws are typically located in a level and square way on a frame. Everything else controls how the boards come to the saws in a square or angled fashion.
In this case, the problem was in the saw assembly. We locked out and climbed up on the equipment to take a closer look. The equalizer was freshly painted and made to look as if it was new. But it was far from new. There were many missing or broken parts. Because of that, we couldn’t control the boards as they were being cut. Broken motor mounts caused the saw blades to rotate in an elliptical fashion. How did the contractor miss this critical detail? How did we miss this during equipment inspection?
We spent the rest of our time repairing or replacing broken parts. Some things couldn’t be fixed immediately. We ordered parts and equipment from other locations. Some had to be air-freighted from the United States at considerable cost. All fixes were completed prior to the official plant start-up, but took valuable resources away from other critical work. All of this could have been avoided had the project team recognized the critical influence of the equalizer and chosen to invest in the right tools for the new plant. Expected savings disappeared due to the lack of All Tools Available.
Status Indicators
During a Kaizen event, teams identify projects to work on and then go off and do the work, hoping to return with a finished product. In my early experience, I allowed team members to work on their own. I hoped they would complete their work in a reasonable amount of time. It didn’t always turn out that way. Hope is not a plan.
During a Kaizen event, teams identify projects to work on and then go off and do the work, hoping to return with a finished product. In my early experience, I allowed team members to work on their own. I hoped they would complete their work in a reasonable amount of time. It didn’t always turn out that way. Hope is not a plan.
They rarely completed their work on time. More often, they lost time and progress because they got stuck and no one knew about it. I started to rotate through groups to assess progress. That relied on one person: me. After a time, I realized there was a better way to track progress, make it visible, and create engagement. The answer: Status Indicators.
Here’s how Status Indicators work:
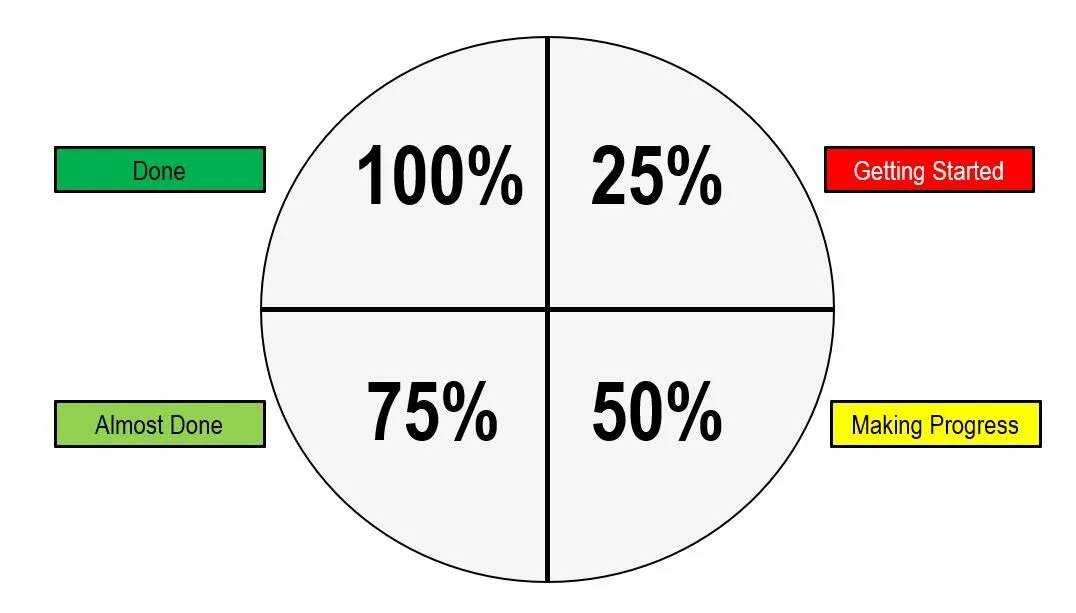
Draw a circle. Break it into quadrants. Fill in each quadrant using a marker, indicating progress towards completion. It doesn’t have to be scientific or pretty, it just has to work.
25% = Getting started – initial progress has been made or a plan has been created.
50% = Making progress – things are moving along and people know what to do and how to do it.
75% = Almost there – we can see the light at the end of the tunnel. We can finish the work.
100% = Done – we’re finished and ready to move on to something else.
There’s no need to break status down into smaller elements. That would cause the team to spend more time updating status and less time doing work. When properly updated, it’s powerful and simple to understand. I use flip chart paper to draw Status Indicators during Kaizen events. Flip chart paper is large enough to allow others to see the status from twenty feet away or more.
To give you a sense of the value and impact of Status Indicators, use the following example. Four teams are working on separate projects.
Project 1 is Almost there, Project 2 is Done, Project 3 is Getting started, Project 4 is Making progress, and Project 5 hasn’t been started. It’s clear who needs help and who can help. Team members from Project 2 can help Projects 3 and 4, depending on their skills and interests. If there are more resources than Projects 3 and 4 need, those resources can start on Project 5. Anyone else, even if they’re not on the team, can assess the status and help those who need it.
The value of Status Indicators has been reinforced to me many times, never more than when I forgot to use them. After a particularly busy day during a Kaizen event, some team members said they were frustrated because they didn’t know what to do next. Others said the day felt chaotic and disorganized. I realized I hadn’t trained the team to use Status Indicators. I immediately showed them how to use them. The next day, much more work got completed. At the end of the day, the team related how much easier it was to manage their work.
From a supervisor’s or manager’s point of view, Status Indicators make it simpler and more efficient to keep track of work going on in many areas. Hours of effort to track progress are reduced to minutes or seconds.
Attention to Detail
In 2007, I moved my family across country to take a new role as Production Manager for a ceiling tile plant in Oregon. The plant had a strong team-based culture. People genuinely wanted to help each other work in as safe and productive manner as possible. It wasn’t unusual to see the Plant Manager on the factory floor, assisting the technicians with their work or helping them stay safe.
In 2007, I moved my family across country to take a new role as Production Manager for a ceiling tile plant in Oregon. The plant had a strong team-based culture. People genuinely wanted to help each other work in as safe and productive manner as possible. It wasn’t unusual to see the Plant Manager on the factory floor, assisting the technicians with their work or helping them stay safe.
Plant performance had deteriorated over the years and we were operating at less than budgeted levels. I was determined to identify the reasons and work with the technicians to turn things around.
The first two months of my time at the plant, I spent more time on the factory floor than in meetings or in my office. I came into the plant at any hour of the day or night, trying to assess and understand the reasons for the lowered performance. People had the right attitude. They wanted to win. What was holding them back?
The Team Managers had strong relationships with their people. The equipment was in generally good condition and there was an established preventive maintenance program. Something was missing and I had to find out what it was.
One morning, while taking a walk around the plant, I noticed papers on clipboards at each operating station on the line. They were titled “While Running Tasks.” Taking a closer look, I saw operations checks to be completed and signed off by the technicians on shift. There were many blank spaces on the papers, meaning that checks weren’t completed during the week.
I reviewed these papers and found that less than half of the checks had been completed and signed off. The Team Managers told me the checks were defined as critical to the performance and safety of the line. Teams of technicians had identified and agreed to the tasks. They met every three months to review and update the “While Running Tasks” as new issues arose.
I reviewed the forms to see if there was any correlation between tasks not completed and downtime or scrap events. In a two-month sample, more than one-third of the downtime and scrap events could have been prevented if the checks were completed properly and on time. I now knew what had to be done.
Working with my three Team Managers, we came up with a plan to rapidly improve performance. We would rededicate ourselves to the “While Running Tasks.” Nothing less than a 100% completion rate was acceptable. Technicians would be accountable to complete and sign off on all tasks during their shift. Team Managers would audit the tasks on every shift, and I’d audit randomly every day and do a complete audit at the end of every week.
My Team Managers wanted to conduct crew meetings and share the new requirements with their crews. I told them I wanted to be a part of every meeting, sharing my logic and belief in our new requirement. They agreed and we planned crew meetings for the next day at 6:30 am, 3:30 pm, and 10:30 pm.
I kicked off each meeting. I told the crews how impressed I was by the teamwork I had observed. I also talked about the honesty of people working there. No one ever signed off on anything unless they had actually completed a task. Now, it was time to use our teamwork and honesty to improve performance at the plant.
I reviewed my findings about the “While Running Tasks.” I shared examples of line failures and scrap events directly impacted by the incompletion of the critical work they had identified and agreed to. We owed it to each other to perform the work we agreed to. Next, I laid out the principles and expectations moving forward:
1. Attention to detail will improve performance and keep everyone safe.
2. While Running Tasks are the first line of defense to prevent problems and reduce safety risk.
3. We must achieve 100% compliance to While Running Tasks – anything less increases risk for downtime and injuries.
4. Completing While Running Tasks is a condition of employment.
I then handed the meeting to the Team Manager, who described how he would work with his crew to attain 100% compliance. He described how he would hold himself and each crew member accountable to their “While Running Tasks.” Crews were also encouraged to review their “While Running Tasks” and verify they were practical and designed to prevent problems.
We received many questions. It was easy to answer any concerns. We truly believed this approach was going to keep everyone safer and more productive. People were worried they were going to be fired if they forgot a task once in a while. We understood and put in levels of discipline. We didn’t want to fire anyone. We did believe that 100% compliance was the best strategy to improve performance at the plant. We couldn’t compromise our beliefs.
During the first two weeks, there were a few “forgotten” tasks. There was some discipline recorded. No one was fired. The first month, compliance reached 90%. Plant performance was noticeably improved. The second month, compliance was 98%. The third month, we achieved 100% compliance. Everyone could tell the difference. The plant was running significantly better. For the next year and a half, compliance stayed at 100%. During that time, the plant attained company records for performance. Attention to detail cost us nothing; except time, focus, and commitment.
A Wakeup Call
In 2001, I was the Business Unit Manager at a Vinyl Flooring Plant in Pennsylvania. Responsible for the one of four business units on site, I had a unionized workforce of 160 employees, three supervisors, and eight technical staff. My job was to turn the shrinking business around and keep my employees safe and productive.
In 2001, I was the Business Unit Manager at a Vinyl Flooring Plant in Pennsylvania. Responsible for one of the four business units on site, I had a unionized workforce of 160 employees, three supervisors, and eight technical staff. My job was to turn the shrinking business around and keep my employees safe and productive.
With many layoffs over the years, the shortest tenured hourly employees had more than twenty-five years of service. They had seen many Business Unit Managers come and go over the years and were determined to outlast me. All three supervisors had been promoted from the ranks and were also of the mindset to survive until the next Business Unit Manager arrived.
This wasn’t the best situation to drive change, but we had to do many things better, and fast. One such change was to do a better job protecting the safety of our employees. We instituted a stronger safety program with improvements in the way employees interacted with and locked-out (an OSHA mandated program) their equipment. Although we were convinced that we were doing the right thing, we had major pushback from the union and even the supervisors, who saw all of the new requirements as a waste of time and effort. After much discussion, my staff and supervisors agreed as a team to be consistent in our safety message, approach, and accountability. At least that’s what I thought.
One day I overheard one of the supervisors telling his crew they needed to follow the new safety protocols because, “The company is making me do this.” Much to my concern and disappointment, this statement confirmed he didn’t believe in what we were doing. At that moment, I knew he would never hold himself or his crew accountable to keep themselves safe.
I couldn’t let this continue and immediately stepped in. I corrected the situation and sent him packing. It sounds harsh. There’s much more to this story. He had been demonstrating a pattern of subversive and destructive behavior for many months. This was the final straw. I was unwilling to put my employees at risk and knew a change had to be made.
Although firing someone is a life changing event for them and for those they work with, it ended up turning out fairly well for everyone involved. The remaining supervisors and crew took safety more seriously and the fired supervisor later admitted this was a wakeup call for him, as he was able to take a renewed commitment to safety to his next employer.
Let’s See How Things Go
During my tenure as Production Manager at a ceiling tile plant in Oregon, I implemented strict rules around changeovers: No one is allowed in the breakroom during a changeover without Team Manager approval; Everyone is available to help during the changeover; Everyone is at their stations when the line is ready to start up; One Best Way changeover procedures are followed to the letter. No deviations. The procedures were developed by the technicians. There was no reason not to follow them.
During my tenure as Production Manager at a ceiling tile plant in Oregon, I implemented strict rules around changeovers:
· No one is allowed in the breakroom during a changeover without Team Manager approval.
· Everyone is available to help during the changeover.
· Everyone is at their stations when the line is ready to start up.
· One Best Way changeover procedures are followed to the letter. No deviations. The procedures were developed by the technicians. There was no reason not to follow them.
These rules came from my observations the first two months after I arrived at the plant. Those not directly involved in the changeover used that time to go to the break room. We lost vital minutes waiting for technicians to return from break when a changeover was completed. Sometimes help was needed to verify changeover settings prior to starting the line back up. If resources weren’t available, things took longer. Technicians were frustrated when they had to wait for help.
Technicians didn’t like the “no break during changeover” rule. I explained changeovers were the most critical activity during the production run and everyone should be helping to execute the safest, most accurate changeover possible. It couldn’t be done from the breakroom.
Some argued they wouldn’t be able to get their breaks under these new rules. I felt they’d have more flexibility around their breaks once changeover performance improved.
Immediately after the new rules were implemented, employees came to my office to express their displeasure. After listening to their arguments, I explained why I felt the rules were necessary. The plant had a culture of teamwork and help. There was no way to help teammates from the breakroom. Then, I told them, “let’s give it a chance and see how things go.” They didn’t like my answer. I was firm in my convictions and sent them on their way.
At the beginning of every changeover, I took a walk to the break room to ensure people were following the changeover rules. I didn’t want to put all of the burden on my Team Managers. I held myself accountable for rule enforcement. From time to time, I found people in the break room during a changeover. I always asked if their Team Manager had approved the break. Most of the time, they got up and went back to the line, indicating they hadn’t.
After four weeks, changeover time was reduced by 33%. Not only was the time reduced, it was more predictable. Just by having everyone available to help with the changeover and in place when the line was ready to start up. My team noticed the results. Visits to my office by “dissatisfied customers” came down significantly.
Team Managers felt more comfortable enforcing the changeover rules. They knew I had their back and they were seeing results. They were able to explain the rules and the reasons for them. It was no longer “Adam’s rules for changeovers”.
Two weeks later, a technician came to my office. He said, “Adam, I know you’re just going to tell me ‘let’s give it a chance and see how things go.’ I just wanted to tell you how I feel about the changeover rule anyway.” I thanked him for the feedback. He knew what I was going to say. There was no point repeating it.
Changeovers became a source of pride across all of the crews. Teamwork strengthened and performance continued to improve. What was once difficult and frustrating was now safe, simple, and predictable.
This Stuff Works
At a gummy vitamin manufacturer in Pennsylvania, I was asked to facilitate a team of mechanics responsible for supporting and maintaining the manufacturing operation. They had difficulty keeping their maintenance area compliant with strict food production regulations. Our goal was to develop a system to guarantee compliance, while improving their ability to service their customers.
At a gummy vitamin manufacturer in Pennsylvania, I was asked to facilitate a team of mechanics responsible for supporting and maintaining the manufacturing operation. They had difficulty keeping their maintenance area compliant with strict food production regulations. Our goal was to develop a system to guarantee compliance, while improving their ability to service their customers.
On the morning of the first day of the Kaizen event, I taught Lean principles and how 5S is used to optimize safety and productivity in a space. It all sounds good in a classroom. The team wondered how it applied to their situation. After training, we took a Gemba walk through their workspace. They thought they were in pretty good shape. The space was cluttered and lacked any hint of organization. They had nothing to compare to and hadn’t been exposed to other examples of 5S in the facility. After generating ideas in their work area, I took them to two locations in the plant that had used 5S: a production line and the Weld shop.
Our first stop was the production line. I asked one of the technicians operating the line to give the team a tour and point out what they had done and the benefits he had seen. He obliged and described 5S and its benefits as best he could. Team members were paying attention to what he was saying, but asked few questions and wrote fewer notes. I thanked the technician and took the team to the Weld shop.
On our way to the Weld shop, I asked team members what they thought of the production line. Feedback fell into two categories:
1. It looks pretty good.
2. I can’t see how it applies to our area.
I knew the next tour stop would be more inspiring. I was intimately familiar with what was done in the area. I could provide a more compelling review for the team.
When we got to the Weld shop, I noticed Jimmy working on a project. He was the team leader when we applied 5S to the Weld shop.
Jimmy: “What are you doing here?”
Me: “This is the Kaizen team from the gummy vitamin maintenance area. I’m giving them a tour of the Weld shop and showing them what your team accomplished.”
Jimmy: “Okay, just don’t get in the way. I’ve got lots of work to do.”
Me: “Thanks Jimmy. If you want to give the tour or share your thoughts, please do.”
Jimmy: “That’s fine. You can give the tour.”
Jimmy is not someone who likes to speak in front of groups or work with teams. Jimmy is also one of those folks who isn’t a fan of management or consultants. But, if he believes in something, it’s useful and helpful to him and others. He doesn’t give out compliments often (ever?) and doesn’t fall in line and do whatever he’s told.
I started the tour pointing out various ideas and improvements the Weld shop Kaizen team made six months earlier. Jimmy was paying attention to what we were doing, but didn’t say a word. I think he was interested to see how I’d describe the work of the Weld shop team. I did my best to represent their efforts and as I did, you could see the pride grow in Jimmy’s face.
My next stop on the tour was at the tool board created by the team during the Kaizen event. As I started describing and demonstrating the use of the tool board to the team, Jimmy got more and more interested. My new team was asking many questions and taking notes on my responses and their observations.
Rob (team leader): “This looks good and all. Does it really stay this way?”
Me: “I don’t think they cleaned up for us.”
Ben (team member): “Does this really work?”
Jimmy: “Look, this may sound silly and it may sound stupid. This $#*% works!”
This was the moment of clarity and credibility for the team. If Jimmy thought so, it must be so. I stopped the tour. The team had seen everything they needed.
I thanked Jimmy and took the team back to the meeting room to review their observations and ideas. On the way back, I challenged them to beat the results of the production line and the Weld shop. They told me they were up for the challenge.
The rest of the week, the team did amazing work, identifying the critical tools needed (All Tools Available), giving them the most visible and logical homes (Visible Evidence) and even telling the leadership team what they needed them to do to sustain the efforts from now on (Layered Audits and Accountability). I am not sure their area was any nicer or better thought out than the Weld shop or the production line, but they thought so, and that’s all that matters.
You’re Never as Good as You Think You Are
Of all the Kaizen events I have facilitated, there is nothing like 3P. It’s the most exciting, energizing, and exhausting way to create breakthroughs with a team. 3P stands for Production Preparation Process. The idea is to design a new product or process with the least amount of waste possible.
Of all the Kaizen events I have facilitated, there is nothing like 3P. It’s the most exciting, energizing, and exhausting way to create breakthroughs with a team. 3P stands for Production Preparation Process. The idea is to design a new product or process with the least amount of waste possible.
Production Preparation Process uses an eleven-step method to open people’s minds to what’s possible and make them as creative as their 8-year old selves. The technique was invented by Chihiro Nakao, a legend in the Lean community.
I was first exposed to 3P by consultants in 2010. We used the technique to design a new product in half the time it would have taken us to using our standard product development methods. I had the opportunity to facilitate half a dozen 3P events and was able to achieve similar breakthroughs with other teams.
I was always curious about the thinking behind 3P and had the opportunity to participate in a 3P competition, run by Sensei Nakao’s company, Shingijutsu, in 2013. During the week, I was able to pick up the nuances and deeper thinking behind 3P. I realized I had been taking shortcuts during the events I facilitated and because of that, we were diminishing our breakthroughs and results. I didn’t get to meet Sensei Nakao at the competition, but gained a deeper respect for the man and his thinking. I decided I would have to meet him one day, if the opportunity arose.
Meeting the Sensei
In 2016, I found out there was an opportunity to meet Sensei Nakao, as Shingijutsu was running another 3P workshop at a plant in Connecticut. He was the overall sensei for the week. I convinced three other coworkers to register for the workshop and we drove up to Connecticut together. During the drive, we discussed our expectations for the session. I wanted to learn from the master, but I also decided I had to have the ultimate tourist experience: be scolded in Japanese by Sensei Nakao.
The host plant made parts for the aircraft industry. More than sixty people signed up for the workshop. We were divided into eight teams, each having a part of the process to improve using 3P. After some initial training in Japanese (with English translation) by Sensei Nakao, teams were assigned a sensei (facilitator) and toured their area of responsibility.
I had met my sensei at the 2013 competition. He chose me to be on his team for that reason. He also knew I had some experience in 3P and its facilitation, so he gave me more responsibility than the rest of the team.
We took a tour of the operation and spent many hours on the factory floor, engaging with the technicians and gaining deeper understanding of the process. By the end of a very long first day, I was exhausted and glad when the team dinner was over. I knew I would need a good amount of sleep to prepare me for the next day’s activities. I felt confident, having much experience with 3P. What could they throw at me that I hadn’t seen before, I wondered?
Go to Gemba
The next day, after a quick review, the team went back out to the factory floor to gather more data and test ideas. I was asking an operator some questions when our sensei motioned to me. He asked me to join him away from the line. He was working with another team member and wanted me to help facilitate the next step of the eleven-step method. They were drawing some pictures on a large piece of paper taped to a wall, just fifteen feet from the production line.
As I was helping my teammate at the wall, I felt a tap on my shoulder. I looked up and it was Sensei Nakao. He didn’t look happy. I got my wish. I was being scolded in Japanese! I only understood one word: Gemba. The interpreter told me that I should be spending more time in Gemba and not away from it at a wall. All learning was to be done in Gemba. There was nothing I could say, but I could see my sensei looked uneasy.
Achieving My Goal
My sensei must have said something to Sensei Nakao, as he was taken aside and spoken to in Japanese. He looked like a beaten puppy. When Sensei Nakao finished with him, he left and went to visit with the next team. I waited a few minutes and then said to my sensei, “You got scolded, didn’t you?” He looked at me sheepishly and finally admitted he had. We both laughed. I had realized my tourist objective.
The rest of the week was a blur. We were able to solve the problem we had been assigned. I learned deeper meanings of 3P and was able to bring back refined skills to my company. I continue to learn more about 3P. No matter how many 3P experiences I have, I can always do better. Sensei Nakao’s scolding reaffirmed it.
It’s Better to Beg Forgiveness than Ask Permission
In 1998, I was invited to Hoogezand, the Netherlands, to help a team make improvements to their ceiling tile production line. Little did I know it would be the longest Kaizen event in my life. I had been to the plant three months before and identified significant changeover time reduction potential. It was time to put my money where my mouth was. In advance of the trip, we identified members of the team and the need for an interpreter. I didn’t speak Dutch and still don’t. We’d have two weeks to work on the line and were to coordinate with the Production Manager any time we needed to shut the line down to work on or test the equipment.
In 1998, I was invited to Hoogezand, the Netherlands, to help a team make improvements to their ceiling tile production line. Little did I know it would be the longest Kaizen event in my life. I had been to the plant three months before and identified significant changeover time reduction potential. It was time to put my money where my mouth was. In advance of the trip, we identified members of the team and the need for an interpreter. I didn’t speak Dutch and still don’t. We’d have two weeks to work on the line and were to coordinate with the Production Manager any time we needed to shut the line down to work on or test the equipment.
I arrived in the Netherlands on Sunday and met with the team in a conference room on Monday morning. After introducing myself, getting to know each of the team members, and providing some Lean and changeover reduction training, we took a tour of the line to identify the highest priority areas to improve and also to get a sense for the team’s interests.
The line wasn’t running very well and I was informed this was typical. Most of the equipment was in need of repair and the maintenance department wasn’t in tune with the needs of the production organization. I told the team I wanted to meet the Maintenance Manager. They looked at me like I had asked for something outrageous. When he came out to the line, I could see why they were a bit apprehensive.
Progress vs. Paperwork
Ullrich was a very tall German man, perhaps six foot eight (I am five foot seven on a good day). With a shaved head, hands twice the size of mine, and a very low and stern voice, he introduced himself by grabbing my hand and saying, “You vill not touch or modify any equipment without filling out the proper paperwork!” Taking my hand back before it was crushed, I assured him we would follow the rules. Although he didn’t seem satisfied, he left to go to the maintenance office.
Realizing we couldn’t fill out paperwork while we were making our improvements, I promised the team I would fill out the forms at the end of each day. The team didn’t look like they believed me, but knew I didn’t want any broken fingers. There were so many problems on the line. Two weeks weren’t enough time to fix everything. With focus, dedication, and proper prioritization, I was sure we’d make significant progress.
The top priority of the team was to improve the reliability of the equalizer, which cut the ceiling boards into finished tile dimensions. Operators had a difficult time setting up the proper cutting sizes. It took hours for them to get the proper cuts. We asked the Lead Operator to shut down the line, to allow us to assess the situation and find out why it was so difficult to set up to the proper size.
Five minutes later, the Production Manager came by to find out why the line was shut down. We told him we were trying to figure out what was keeping the equalizer from being set up consistently. He reminded us we were supposed to let him know any time we were going to shut down the line. I apologized and said it wouldn’t happen again. Knowing it probably would happen again; I advised the team to remind me to let the Production Manager know our intentions before shutting the line down. They promised they would. I wasn’t so sure.
Asking the Right Questions
The equalizer used precision screws to guide the saws to their final positions on the cutting bed. Operators turned a handle to move the saws on the screws. Watching the saws move as the handle was turned, I could see the saws weren’t moving consistently. With the first full turn of the handle, it appeared the saw moved twice as far as it did with the second full turn of the handle. This situation had to be resolved. First, we had to figure out why things were acting in this way.
We tracked down a dial indicator with a magnetic base. We wanted to see how much variation was occurring when we tried to move the saws. On our first test, the handle was turned one full revolution and the saw traveled 0.020”. We turned it one full turn in the opposite direction and the traveled just 0.005”.
The team was convinced the precision screw had worn down, causing variation in movement. Thinking about this, I knew this should not be the case, but I also know what my eye had seen. Then I asked the question, “What is riding on the precision screw?” It turns out it was a brass bushing. My next question was, “Which component is more likely to wear down, the brass bushing or the hardened steel precision screw?” It had to be the brass bushing. My next question was, “When was the last time the brass bushings were replaced?” No one remembered it ever happening.
We tracked down Ullrich, explained the situation and found enough brass bushings to replace all of the assemblies on the equalizer. Four hours later, we had replaced bushings worn down to the nub with brand new brass bushings. After, we tested out changes and now had saws able to repeat their locations within 0.001”. Ullrich reminded me to fill out the proper paperwork, but was impressed enough to shake my hand. This time, he didn’t crush it.
Making Progress and Earning Trust
Over the rest of the first week, we made similar improvements to all areas of the line. We never filled out the paperwork in advance, but our earlier success at the equalizer reduced the pressure on me, the team, and my hands. We also made a game of shutting down the line and then betting on how long it would take the Production Manager to show up to see what we were doing. We were improving so many things so quickly he also gave us the leeway to shut the line down without approvals, but kept playfully reminding us to follow the rules.
The team enjoyed the work so much they decided to work on Saturday and then take Sunday off. I took Sunday to go sightseeing and got lost in the village of Makkum, 80 miles to the west, known for their ceramic tile craftsmen. That’s a story for another time.
Monday, the team was ready to make more improvements to the line. We improved almost every part of the production line by Friday morning. Our report out was scheduled for Friday afternoon. The entire plant staff showed up at the production line and listened to the team explain and show their improvements in Dutch. At the end of the report out the team said, “Adam leerde ons dat het beter is om vergeving te smeken dan om toestemming te vragen!” After much laughter and clapping by the staff, Ullrich, and Production Manager, I was told the translation was: “Adam taught us that it is better to beg forgiveness than ask permission!”
Let It Go
In 2010, Armstrong World Industries emerged from bankruptcy. A minority stake of the company was bought by a private equity firm. This firm knew there were many improvement opportunities and brought in consultants to help create a culture of continuous improvement across the global organization. Their approach was to hold many Kaizen events on a weekly basis, exposing as many people to the principles of Lean as quickly as possible.
In 2010, Armstrong World Industries emerged from bankruptcy. A minority stake of the company was bought by a private equity firm. This firm knew there were many improvement opportunities and brought in consultants to help create a culture of continuous improvement across the global organization. Their approach was to hold many Kaizen events on a weekly basis, exposing as many people to the principles of Lean as quickly as possible.
Having recently completed my assignment as the St. Helens Oregon Operations Manager, I was asked to provide support to the consultants. Sometimes I co-facilitated Kaizen events with the consultants. Other times, I was asked to facilitate Kaizen events independently of the consultants. This story is about one of the first Kaizen events held at the Marietta, Pennsylvania ceiling tile plant.
Paired with a consultant, I co-facilitated a team using 5S to improve the safety and productivity of their packaging area. 5S stands for: Sort, Set in Order, Shine, Standardize, and Sustain. Using this methodology, teams take a step by step approach as they make quick and meaningful changes to a target area. Lean was new at the plant, so we provided extensive Lean training to the team. The team was comprised of line operators, mechanics, a supervisor from the area, and a few staff members.
After the training, we took the team out to Gemba (the place where the work is done) to assess the materials that were no longer needed in the area. This is the first S, Sort. During Sort, the team is to decide what is absolutely necessary and what is clutter. The clutter is then disposed of or removed from the area. Once done, the team then moves on to Set in Order. The packaging area was built twelve years earlier and it was apparent most things in the area were from the first days of production.
A Case of Clutter
Many of the team members were having a difficult time finding things to dispose of. When something was found that didn’t look current or relevant, people would say things like, “We may need it in the future.” Or, “If we fixed it, we could use it.” After a few hours in the area, it didn’t look the team was willing to take a leap of faith and remove much of the unused and unusable equipment and materials.
The consultant and I stepped away from the team to discuss a strategy. “Adam,” he said, “we need to demonstrate it’s alright to remove and dispose of the clutter. Let’s pick a few things to remove, do it ourselves, and see if we can get others to join in.” I agreed, knowing we had to demonstrate it was okay to do something drastic to get breakthrough results. We took a walk around the area and found a few items that looked like they didn’t belong and then happened upon something that definitely needed to go.
Underneath a platform was an old rolling toolbox, covered in dust. Except it was unable to roll. One of the wheels was missing. When we looked through the drawers, all we saw were various nuts and bolts covered with years of grease and grime. The toolbox hadn’t been used in years and it looked to be an ideal candidate for the dumpster. It was pretty heavy, so we asked one of the team members to assist us as we pulled it out from under the platform. After getting it out, we placed it on a skid, ready to be taken away by a forklift.
A Toolbox Road Block
Except we couldn’t. Just as soon as we had called for the forklift, the supervisor on our team came at us with an angry look in his eyes. “What do you think you’re doing?” We explained what and why we were doing what we were doing. His face turned red. “I bought that toolbox for $300 and it’s served us well. I can’t believe you would just throw it out. We could fix it and use it.” When we pointed out the three new, clean rolling toolboxes in use in the packaging area, he stormed off.
We decided to talk with the rest of the team members. They told us no one had used the toolbox in years, the other toolboxes were sufficient, and the materials inside the old toolbox were of no use to them. They agreed to dispose of it and started to find other things in a similar condition to be removed as well.
The supervisor didn’t return that day. At the end of the day, the consultant and I were called to the Plant Manager’s office to talk about what had happened. The supervisor had stopped by the office earlier. After describing what we had done and the reaction of the supervisor and the team, we were told to tone down our approach. Lean was new to the plant and the people working there, and not everyone was on board. The supervisor was very proud of his accomplishments, helped design the packaging area, and took ownership for everything in the area, even the broken-down toolbox.
The Plant Manager told us it was more important to get the whole team engaged, rather than take extreme measures to prove a point. We agreed, and after leaving what felt like the principal’s office, we developed our strategy to reengage the team and improve relations the next day.
Taking a New Approach
The next morning, with the full team in a meeting room, we apologized for taking such drastic actions. We promised to get full team approval before making any more changes. When the team went back to the packaging area, they were energized. The consultant and I were able to step back and let the team make all of the organizational decisions in the packaging area. By the end of the week, the team removed more than 80% of the supplies, tools, equipment, and materials in the area. What remained was logically organized, in pristine condition and very visual. It was easy to see the condition of the area and if anything was out of place.
After a tour of the area, plant leadership remarked how much better everything looked and felt. Team members talked about the impact of the work and how it would benefit them in their normal jobs. This was the first of hundreds of Kaizen events at the Marietta ceiling plant over the next decade. Everyone learned valuable lessons. But I may have learned the most valuable lesson of all – pay strict attention to the team and understand what engages and motivates them. Even small changes are important; you don’t have to shoot for the moon every time. As long as the team owns the change, it will be sustained.
Recognize the Effort, Not the Results
When teams start working on a problem, they are often given the freedom to choose their own solution path, and it may not be anything like you were anticipating. I learned many years ago every time I tried to predict what a team was going to do; I would be wrong. They typically beat anything I could come up with. So, I decided to stop trying to guess and shifted my focus to helping them accomplish as much as was possible during the short time of the Kaizen event. To do this, I had to come up with creative ways to encourage them. Some ways were silly, some were formal, but they always seemed to remember the recognition. Here are two examples…
When teams start working on a problem, they are often given the freedom to choose their own solution path, and it may not be anything like you were anticipating. I learned many years ago every time I tried to predict what a team was going to do; I would be wrong. They typically beat anything I could come up with. So, I decided to stop trying to guess and shifted my focus to helping them accomplish as much as was possible during the short time of the Kaizen event. To do this, I had to come up with creative ways to encourage them. Some ways were silly, some were formal, but they always seemed to remember the recognition. Here are two examples:
Clapping helps, believe it or not
I set milestones during Kaizen events. When the team reached them, I encouraged the rest of the team members to clap in recognition for their efforts. A team would come back with their plan for the next steps of their work. They’d review it with the rest of the team and then get feedback on their approach. At the end of the review, I’d say, “Let’s show them how we feel about their efforts so far.” I’d start clapping for them and the rest of the team would join in. Those who were reviewing their plans started clapping, and you could see the pride in their faces for their efforts. As we did this more, the team would naturally clap for each other’s efforts. Sometimes we’d make fun of ourselves, but we didn’t stop clapping. It’s infectious! We came up with any number of reasons to clap for each other.
Little trinkets seem to matter
When awards are given, the money gets spent, but the symbol lives on and reminds us of what we did and how we felt. Here’s a little story about that:
As a consultant, I was always getting something – shirts, cups, paperweights, and other trinkets from my clients for the event. It was usually my suggestion to the sponsor to give the team something to remember the event by and make sure it wasn’t money. So, invariably, I’d receive a trinket too. Plus, I was paid for what I was doing, and was well fed. Not a bad deal. But I felt like I should do something for my team members too. I wanted to show my appreciation for their efforts. After a while, I came up with the idea of creating a special coin, which I call my “token of appreciation.” It’s gold colored and is given to team members who make it through the entire Kaizen event. On the last day of the Kaizen event, I greet each team member as they enter the room and hand them a coin and thank them personally for their efforts.
When I first started handing out coins, I was a little uncomfortable doing it, as it was new to me and to them. But I got all sorts of positive reactions to it. Some thanked me, some asked me if they were chocolate or real gold (they weren’t), but everyone seemed to appreciate my thinking of them. Then, one of my team members said, “This is my new lucky coin!” I thought he was just being kind. A few months later, I was walking through the factory and heard a forklift coming down an aisle in my direction. Stopping about 20 feet from me, the forklift driver called to me, “Adam, check it out, I still have my lucky coin!” I couldn’t believe it. He was holding up the coin proudly. It really mattered to him. It made my day, and over a year later, it still makes me smile when I think about it.
But wait, the story isn’t over. Over 9 months later, I was walking through the same plant, ran into the same team member, and he proudly showed me how much his lucky coin had worn down. I have been carrying a coin in my pocket since the first time I started handing them out, so my coin was pretty worn down too. We compared our two coins and he was proud that his coin was more worn than mine was. So simple, but so meaningful. I was going to find a new trinket to hand out for the future, but now I realize there’s no reason to. People like the idea of the coin, so why change? It’s the thought that counts.
Understanding is Critical
In February 2020, Process Improvement Partners was asked to facilitate a strategic planning session in Montreal for a global consumer products company. Having facilitated multiple Kaizen events where English is not the primary language, we set about to design an event that would incorporate additional translation time and resource effort for the event. Normally, this type of session takes three days. Even though we were told that most participants were bi-lingual, we aligned with the sponsor and leader and added four hours to the event plan.
In February 2020, Process Improvement Partners was asked to facilitate a strategic planning session in Montreal for a global consumer products company. Having facilitated multiple Kaizen events where English is not the primary language, we set about to design an event that would incorporate additional translation time and resource effort for the event. Normally, this type of session takes three days. Even though we were told that most participants were bi-lingual, we aligned with the sponsor and leader and added four hours to the event plan.
In the weeks leading up to the event, presentation slides were developed and sent to the team leader to be modified to show English and French terms. I knew that the first day of the session would be the most challenging, as most participants had no Kaizen event or Lean experience. With much training, demonstration, and direction, we had to ensure important elements were clearly and correctly understood.
On the first day of the event, every time anyone spoke, there was translation into French or English. Every time someone asked a question in French, it was translated into English. Any English discussion was translated into French. Things were going slower than anticipated. By lunchtime, we were two hours behind. People were getting concerned. I knew we were going to be fine as the week wore on. The first day is more focused on discussion than teamwork and it feels longer and is more challenging to first-timers.
Aligning and Adjusting
At the end of the first day, we were exactly four hours behind. Those four extra hours planned for in the overall event were already used up. Additionally, in a feedback session at the end of the day, most team members said we were translating more than necessary. After most of the team left, we regrouped with the team leader and sponsors to build a plan to get us back on track. On a positive note, all team members were speaking freely and engaging extremely well. This was most critical for the overall success of the event. In preparations for the event, the leader and sponsors weren’t expecting so much engagement. Their initial skepticism led to the translation requirement.
We agreed we would reduce the translation to an “as needed” basis. This meant that we would ask our engaged team members to speak up when they needed translation or further explanation. It was risky, but we would pay attention to the room and draw out requests for translation if we saw engagement declining. We then joined the team at dinner and watched the team strengthen during the evening.
On the morning of Day 2, we explained our new strategy to the team, in English and French, and told them it would be the last translation they received until they requested it. We also agreed not to translate anything into English. When a question was asked in French, it would be answered in French. The facilitators didn’t need to understand the conversation, unless they were asked something they had to specifically answer. The team liked the new approach.
Less Translation, More Engagement
Once we got the hang of the reduced translation and started watching the team for their understanding, progress happened faster and the team seemed more engaged and satisfied. At the end of the second day, the team reflected their appreciation for the change in approach and showed an optimism for the day’s work and the work to come.
The next two days flew by and the team built a strategic plan of which they could be proud. Their plan improved productivity, safety, quality, and customer service. They also learned many new tools and techniques they could use to solve problems in their day to day work. On the final day, ten different presenters told the story of the week and the strategic plan to an audience attending by video conference all over the world. Those in the audience said they could feel the enthusiasm and alignment and were amazed by how professional the presenters were, regardless of their position. They voiced their support to the team and encouraged them to implement their plan. Some even wanted them to implement it sooner than planned.
The week reinforced how critical communication and understanding is for the team to win. Even though we reviewed progress and issues with translation at the end of the first day, we now know we need to do it sooner if we find ourselves in a similar situation in the future. For the team’s part, we can only thank them for hanging in there while we were learning this valuable lesson.
Things Aren’t Always What They Seem
In 2011, Armstrong’s Marietta ceiling plant was utilizing technical resources and replacement workers to run the plant. Management and the labor union were unable to come to an agreement around their contract, and for seven months, the union workers were locked out.
In 2011, Armstrong’s Marietta ceiling plant was utilizing technical resources and replacement workers to run the plant. Management and the labor union were unable to come to an agreement around their contract, and for seven months, the union workers were locked out.
During that time, I assisted with day to day production operations, maintenance activities, and many process improvements. I worked all over the plant, identifying and implementing as many improvement projects as possible. I was extremely motivated, as the projects improved safety, quality, and productivity for the rest of the plant. The work helped me through the long days, energizing me as I could see instant results from my efforts. Others were mostly happy with my work. I say mostly, because not everything worked as planned or as expected. This one of those stories.
The Lamination Line
One of the most critical lines in the plant was the lamination line. It put a top layer on the ceiling tiles. Customers were willing to pay a premium for these tiles. The lamination line was producing at a lower than budgeted rate and had a large amount of downtime. I decided to see if I could help reduce the downtime and increase the production rate.
When I arrived at the line, I met with Wayne, an innovation scientist who was running the line and teaching others to operate it efficiently. We discussed the issues causing line downtime and reduced output rate, then he gave me a tour of the line. On the tour, it became apparent that the position of the board as it enters the laminating process was most critical. I noticed boards were entering the process at an angle. Wayne told me most of the time the angled board could be cut into usable pieces and when it appeared to be too much of an angle, he would stop the line and make adjustments.
I took a look at the conveyer before the laminating process and noticed a series of angled rolls. These rolls were angled to move the board over to one side of the conveyer and keep it against a guiding rail. There were 36 total rolls along the conveyer, and of those, 28 were angled. I believed there were too many angled rolls. They were driving the board at an angle past the guide rail, keeping the board from entering the laminating process squarely.
A New Way to Roll
I asked Wayne if he was willing to try an experiment. I wanted to straighten out most of the rolls, leaving just a few angled rolls. The board would be driven to the guide rail using the angled rolls and then the straight rolls would keep it straight as it entered the laminating process. Wayne asked me how long it would take. I estimated four hours of effort with his help and the help of a mechanic. The line was scheduled to be down for maintenance the next day. If we could do the work then, he would be happy to help.
The next day we started the work with the help of a mechanic. We identified the center of the laminating process and positioned the guide rail parallel to the direction of travel of the board into the process. Next, we moved the guide rail to the optimal position to guarantee the board would be centered entering the process. We marked the original position and current position, just in case we had any issues. Next, we started straightening the rolls.
An engineer came by to see what we were doing. When I explained, he told me he had installed the laminator a few years back and was responsible for all of the angled rolls. He didn’t agree with what we were doing and tried to convince us to stop our work and put everything back. I assured him we were experimenting and were willing to put everything back to its original position if necessary. Although he didn’t seem satisfied, he decided to go elsewhere while we did our work.
Sometimes Less is More
After just under four hours, we were done. Before starting up the line, I called the engineer to see if he wanted to see the results of our experiment. He said he would come over later that day. We didn’t want to wait, so we started up the line and sent some test boards down the line. The first time, we had a jam. When we looked at the cause, we realized the new position of the rolls and the guide rail had an adverse effect on equipment on the other side of the line. We shut down the line and made some adjustments to take into account the new arrangement.
On our next attempt, the test boards entered the laminating process in a straight and square fashion. We were excited, but weren’t ready to declare victory. We started up the line and put it into production. We were amazed, the boards were not only going in exactly as we hoped, but they were spaced out more evenly as they came down the line. Wayne was excited and now wanted to speed up the line. He made small changes to speed until the line was running 20% faster than it had ever run. Right in the middle of this, the engineer came by to see what had happened. He was surprised things were going so well, but admitted he had angled so many rolls without considering the impact on the overall process. He then said, “Maybe less is more - too much of a good thing may be a bad thing.”
Over the next few months, we made additional improvements to the laminating process and the plant had a much more productive and safe operation than before we started.
Trust, but Verify
In 2005, I was asked to be part of a team to help Armstrong’s Mobile Alabama ceiling tile plant improve their performance. Production output had steadily declined over the first few months of the year, and they were well behind budget. The team was tasked with identifying and implementing improvements to the operation that would drive performance back to budget for the full year. The team leader called the effort a “Full Court Press”, meaning we would not give up until we accomplished our mission.
In 2005, I was asked to be part of a team to help Armstrong’s Mobile Alabama ceiling tile plant improve their performance. Production output had steadily declined over the first few months of the year, and they were well behind budget. The team was tasked with identifying and implementing improvements to the operation that would drive performance back to budget for the full year. The team leader called the effort a “Full Court Press”, meaning we would not give up until we accomplished our mission.
The Mobile plant had one board forming line and two fabrication and packaging lines. The board forming line was clearly not the problem, as the quality, productivity, and safety were well above budgeted performance. The fabrication and packaging lines were where the losses were occurring, so we agreed to focus our efforts there.
On our first day at Mobile, we attended the morning production meeting. We introduced the team to the staff and reviewed performance. The plant staff members were open to our help, but weren’t sure what we would be able to deliver in a short time. We assured the staff we would do our best and coordinate any efforts through them. Once the meeting ended, we took a tour of the fabrication department. During this tour, we observed many problems and spoke with operators, mechanics, and other staff to get feedback and ideas. Many were disappointed with the performance and hoped we would be able to help them turn things around.
Each of our team members had a specialty. One was interested in the programming used to control the equipment, another was fascinated by the coordination of materials and resources. My area of expertise was flow of materials through the production line. During the tour, I noticed many line-stops and jams. I knew I could provide help.
With the agreement of our team leader, another team member and I took a detailed look at one of the main fabrication lines. This line was led by a technician named Walter. Walter was extremely interested in what we were doing, and asked if he could tour the line with us. We were happy to have him along, as he introduced us to all of the crew members and lent credibility to our efforts. He also appreciated our approach of watching the line carefully to identify the causes of the line-stops and jams.
Something Isn’t Hitting Right
On our tour, we stopped at the punch press to watch its operation. Something didn’t look right to me. The press creates holes in the ceiling tiles which allow air and sound to enter the tile. It’s critical for the ceiling tile to enter and exit the press squarely and centered. Following the press, there’s a gate that stops the tile while the press completes its work. If the tile is angled, the edge of the tile gets damaged when it hits the gate. As I watched the tiles enter and exit the press, I noticed they weren’t exiting the press squarely and hitting the stop-gate at an angle.
I asked the press operator if he was concerned about the tiles hitting the stop gate at an angle. He told us he thought any damage would be cut out later down the line. It looked to me as though the amount of damage wouldn’t cut out completely, but the operator was convinced otherwise. I made notes of what I had seen, and we continued our tour.
Following the press, tiles were being painted and then cut to final size. After the cutting station, tiles went through an inspection station, where two operators were visually checking the quality of each and every one. While we were there, the inspectors were rejecting one-third of the tiles they were inspecting. There was so much scrap being generated they were having a hard time keeping up and had to stop the line many times.
During one line-stop we asked the inspectors what they were seeing. They showed us the broken edges of the tiles. The edges had cracks down the length of the tiles at an angle. They looked just like the angle of the press stop-gate we had seen earlier. I asked the inspectors for a few samples, which they were more than happy to share.
A New Angle on the Situation
We took a walk back to the press with Walter. We showed the press operator the sample ceiling tiles. He was shocked. He didn’t realize the stop-gate was causing so much scrap. He immediately shut the line down to make adjustments.
While the line was down, I asked if I could take a look inside the press to see if there might be a reason the tiles were hitting the gate at an angle. After locking out the press, I took a closer look and was amazed at what I saw. The guide rails in the press were not straight as designed, but curved. These rails were causing the tiles to turn at an angle when they entered the press. All plants had scheduled maintenance to replace press guide rails every six months. When I asked the press operator when the last time the rails had been changed, he didn’t remember, but thought it had been years. I then asked if they had backup press guide rails in their storeroom. Luckily, they did. Even luckier, they were straight.
Setting Things Straight
We replaced the curvy press guide rails with straight ones, and started up the press. Immediately we stopped the press. We were still damaging the edges of the tiles, this time at a different angle. We quickly identified the problem. The stop-gate was angled for the curvy guide rails and had not been adjusted for straight press guide rails. Once we straightened the stop-gate, the edge damage disappeared. After a few handshakes and high fives, we created a monthly press guide rail inspection and a six-month replacement program for this critical component.
During the week, the team made many other quick improvements and planned out other work that helped the Mobile plant return to budgeted performance for the year. If there’s a lesson to be learned from Armstrong’s Mobile plant, it’s to trust your processes, but verify them on a regular basis. Trust alone cannot eliminate inefficiencies or waste from creeping in, but consistent verification can identify these issues quickly so that they can be corrected.
The Strength of Ownership
My focus in continuous improvement has always been to help teams solve problems in a sustainable way. Early on in my career, I learned many facilitation techniques through trial and error, mostly error. One of the biggest errors I ever made during a Kaizen event was to be too directive with a team. When one of the team members said, “Adam wants us to do this…,” I knew I was in trouble.
My focus in continuous improvement has always been to help teams solve problems in a sustainable way. Early on in my career, I learned many facilitation techniques through trial and error, mostly error. One of the biggest errors I ever made during a Kaizen event was to be too directive with a team. When one of the team members said, “Adam wants us to do this…,” I knew I was in trouble.
Another early mistake I made during Kaizen events was to take responsibility for writing team member ideas on a flipchart while they were shouting them out to me. While this seems like a natural thing to do, I was taking ownership for team member ideas by writing them. I also was hindering engagement during the event, as the only person that cared about what I was writing was the person speaking the idea and me, the person writing it. The rest of the team didn’t need to pay attention to what was going on. This approach also allowed for dominant team members to get more attention than less vocal team members.
Post-It™ Notes – The Great Equalizer
I knew I needed to change my approach to drive engagement and ownership to the team members. My first change was to use Post-It™ notes for gathering ideas from team members. Each team member would write their ideas, one per Post-It™, and then speak them, one at a time. In this way, everyone had an equal opportunity to voice their ideas, and they were written in a way that was meaningful to them.
I started to develop fun ways to share the ideas, with a focus on giving everyone equal opportunity to share their thoughts and minimizing the opportunity to dominate the conversation by stronger team members. I also noticed that Post-It™ Notes were the great equalizer. It didn’t matter what level in the organization a team member was. Their Post-It™ Note looked just like anyone else’s.
Once we uncovered all team ideas, I had to develop ways to prioritize them. There are many ways to do this, but the approach I settled on was multi-voting. Each team member gets an equal number of votes and is asked to pick their favorite ideas and place their vote on the ideas. As an example, there might be 100 unique ideas written on Post-Its™ and 10 team members. Each team member is given a vote to place on their 5 favorite ideas to work on and implement during the Kaizen event. The ideas with the most votes are the ones the team will work on. This technique works fast, but there seemed to be something missing. People told me that it was chaotic and there was something didn’t feel right about how things were prioritized. I knew I had to improve multi-voting.
Adding Process to Chaos
One event, I added criteria to the process of multi-voting to see if it would focus the group and help them feel more comfortable with the approach. I added these criteria to use when voting for a favorite idea:
1. It provides the biggest benefit to the customer and to us (related to the problem to be solved)
2. I actually want to do this (personal interest in the work)
3. We can accomplish and implement this during the Kaizen (fast implementation and low money spent)
Once I developed the criteria, the teams seemed more confident they were choosing the right ideas to work on. The criteria all but guaranteed people were interested in what they were doing, which would maximize the results, and the work would get completed quickly.
Pick Your Passion
Now that we knew the top priority work, we would assign team members to the work. I usually left this to the team leader. I noticed some team members didn’t like their assignments and I knew I had to come up with something better. That’s when inspiration hit me. What if I could help team members connect with the project they truly wanted to work on? One day, I decided to try something new. After prioritizing the top three projects to work on and writing them on a flip chart, I said, “First come, first served, put your name on the project you want to work on.” Immediately, two team members jumped out of their chairs in order to put their names on projects that were most meaningful to them. This was just the reaction I was hoping for. The connection between the team members and the work was strong. But, could I replicate this reaction?
It turns out, I have used the same approach throughout the world and it’s not unusual for some team members to jump out of their chairs to put their names on the projects that matter to them most. Not everyone does that, and it allows us to balance the teams to the projects. I learned to set the safety expectations prior to making my “First come, first served” statement.
I have used these facilitation techniques and many others to strengthen the engagement, empowerment and commitment of teams. In the end, I want them to win. I will continue to refine my approach to help them do that.
Ownership at the Right Level
I was Lean Champion for the global technology team at Armstrong World Industries for many years. During that time, I supported teams of technicians, scientists, engineers, project managers, and the leadership team across four different departments. I had the good fortune to assist teams in their efforts to develop and launch new products, deploy capital equipment, and build factories all over the world. All departments had access to the Pilot Plant to support their efforts when necessary.
I was Lean Champion for the global technology team at Armstrong World Industries for many years. During that time, I supported teams of technicians, scientists, engineers, project managers, and the leadership team across four different departments. I had the good fortune to assist teams in their efforts to develop and launch new products, deploy capital equipment, and build factories all over the world. All departments had access to the Pilot Plant to support their efforts when necessary.
The Pilot Plant was a series of disconnected processes which had the resources and capabilities to test new materials, products, processes, and other ideas in a controlled way. Information gleaned from tests and trials was utilized in the effective delivery of projects and other development efforts. Each of the processes in the Pilot Plant had an owner, who was responsible for the care and safety of the process. The owner would also try to schedule the process to allow it to be utilized effectively and to keep wait times to a minimum. All process owners were the technicians who were most familiar with the operation of their process. Although they were at the lowest level of the group, they were very proud of their equipment and took ownership to keep things safe for their customers.
As Lean Champion, I spent many hours in the Pilot Plant, learning about its capabilities and trying to understand how I might be able to help the technicians in their efforts to support the rest of the organization. It was during my early days in the Pilot Plant that I met a gentleman, we’ll call him Roy, who was lead technician. He had just taken on the leadership role for the Pilot Plant, responsible for the overall effectiveness and operations. Having worked in one of Armstrong’s factories prior to his arrival at the corporate center, he had vast equipment knowledge and some leadership experience.
A Source of Frustration
Before taking over as lead technician, Roy worked in the Pilot Plant as a process owner and participated in the annual Pilot Plant clean-up. This was a multi-day effort by all technicians at the end of the year. They would go through all of the materials, supplies, and equipment throughout the plant and clean out the clutter and reorganize things in as safe and productive manner as possible. All development and testing in the Pilot Plant would be delayed during this time, as all technicians were busy cleaning things up and trying to make sense of what they had.
None of the technicians liked the annual clean-up process because they knew it wouldn’t take long for things to go back to the way they were prior to the clean-up. Roy expressed his frustration to me more than a few times. Once he became lead technician, he was even more frustrated and wanted to do something about it. My first suggestion to Roy was that he should discuss his frustration with his manager and gauge his support for Roy’s efforts. Roy did this, but seemed just as frustrated. Upon further discussion with Roy, I found out his manager was supportive of his efforts, but didn’t offer solutions Roy thought he could implement without direct assistance from his manager. He really wanted his manager to tell everyone to clean up after themselves.
Over the next few months, I facilitated 5S (Sort, Set in Order, Shine, Standardize, Sustain) events in the Pilot Plant to support Roy’s efforts to make areas safer and more productive for everyone. The few area owners who had completed 5S events had a strong managing system to keep their areas in top shape. The other 30 or so areas did not, so clutter and disorganization was prevalent everywhere else in the Pilot Plant. Roy was getting more and more frustrated.
Turning the Corner
One Monday morning, following the weekly technician meeting in the Pilot Plant, Roy stopped me on my way back to my office. “Adam, I’m really frustrated,” he said. “My manager won’t hold everyone accountable to keep the Pilot Plant organized and safe. He tells them it’s their responsibility, but doesn’t do anything about it when they’re not compliant. What can I do?” “Roy,” I said, “Who’s the leader of the Pilot Plant?” “I am,” he said. “Well, as leader, you have every right to set expectations and hold accountability. You are the operations manager; your boss is the plant manager. The plant manager needs you to get your operations in order. Let me help you do that.”
Over the next few weeks we built our strategy for putting the Pilot Plant in order. Our strategy included: setting clear expectations for all areas of the Pilot Plant, redefining responsibilities for all area owners (not just the areas that had been 5S’d), developing a weekly leadership walk (Gemba walk), and creating visual management to hold all area owners accountable. We mounted a large white board in the main meeting room and put lines and names on it, ready to explain it to the technicians at the next technician meeting.
The next Monday morning, we introduced the new strategy for making the Pilot Plant the safest, most productive place possible. The technicians listened with keen interest and asked many questions as Roy described the changes. They were skeptical that there would be any change in behavior of the scientists, engineers, or managers when they used the spaces in the Pilot Plant. Then Roy explained the white board, which he called the “Area Owner” board. On it were over 30 Pilot Plant locations with the corresponding name of the area owner and a space for a date to be written. At the first of every month, a red magnet would be placed for each location, signaling the owner hadn’t yet met certain monthly requirements. Once those requirements were met, the Area owner would replace the red magnet with a green magnet. The Area Owner would write in the date the requirements were met. At the beginning of the next month, all magnets were set back to red.
The technicians were furious. They thought those red magnets made them look like they weren’t doing a good job and didn’t want any part of the new system. I jumped in and explained it was a very visual and urgent way to show what areas weren’t yet compliant and who might need help. The system wasn’t a reflection of the specific area owner, unless he or she hadn’t made the effort to meet the requirements or ask for help. We felt if we could get all areas to green every month, we wouldn’t need the annual cleanup, which everyone hated.
A Delicious Incentive
At this point, the technicians started to buy-in and support the idea, but they were still skeptical that some of the area owners would be motivated to get to green every month. I knew I needed to provide incentive. I said, “The first month we get all areas to 100%, I’ll buy every area owner lunch and we’ll celebrate!” That got their attention. I then described the design of the management walk: We would take a selection of managers of the scientists and others who used the Pilot Plant and tour all areas, looking for areas where we could reinforce the need for compliance to the requirements. We would do this every week and sign off to show we had and we were just as accountable as the technicians.
For the next few months, I attended every Monday morning technician huddle, and reinforced the new systems and encouraged the area owners to get their areas to green before the end of the month. One Monday, late in the third month of the “Area Owner Challenge”, there was only one technician whose area was still red. Almost to a person, the technicians pressured him to get his requirements done and make sure Adam would buy them lunch! They did it in a fun way, but I knew they were serious. I knew our system was working at last.
Over the next months, the technicians hit 100% compliance almost every month, and by the end of the year there was no need for the annual cleanup. Pride in the Pilot Plant grew. In the following years, the Pilot Plant was bench-marked many times. Not because of the technology, but because of the strong ownership and pride and systems that allowed new products and projects to be delivered in the safest and most productive way possible.
Training in the Moment
Process Improvement Partners was invited to help a gummy vitamin manufacturer reduce their changeover time. Walking through the process with the sponsor, we felt that we could attain a sustainable 50% reduction in time, while improving the safety of the process and engaging the team with a winning attitude.
Process Improvement Partners was invited to help a gummy vitamin manufacturer reduce their changeover time. Walking through the process with the sponsor, we felt that we could attain a sustainable 50% reduction in time, while improving the safety of the process and engaging the team with a winning attitude.
After the charter was developed, we identified the winning team of participants. This included people who work in the process, those who manage the process, and others who were quite interested in helping the team win.
First Day Skepticism
On the first day of the Kaizen, the team was joined by a group of others from management and support groups, who were very interested in what was about to happen. After some introductions, those in the room voiced their concerns about the ability of the team to reduce time in half without substantial capital investment or significant training. As I had been through many of these sessions before with continued success, I assured them we wouldn’t have to spend much money and we would be able to train everyone properly by the end of the week. After all, we only had a week to accomplish our goals. I told the team that every team before them was able to achieve the 50% goal and I knew they would too. Most in the room looked like they thought it wouldn’t be possible, but they were supportive of our efforts.
The average changeover time for the past year was 4 ½ hours, so our goal would be to safely complete the same type of changeover in 2 ¼ hours. After some training in Lean concepts, we walked out to the factory floor and observed the crew on shift complete a changeover. This changeover took 5 hours and 32 minutes, a full hour longer than our baseline. After the changeover was complete, I brought the team into the meeting room to share their observations and ideas for improvement to the changeover. At the end of a very long first day, the team had four prioritized improvement efforts to work on during the morning of the next day. We went out to dinner to unwind and continue the discussion. Even though it was a very long day, everyone seemed excited about what might be possible.
On the morning of day 2, the team started to make changes, based on their observations and ideas. The plan for day 2 was to implement as much as possible in the morning, and then the team would conduct the changeover in the afternoon. This time, the crew on shift would observe the team, rather than the other way around. Some basic organization, visualization, and minor equipment improvements were made before lunchtime. We were now ready to see what would happen.
The plan was to conduct the changeover after lunch and then review our results and ideas following the changeover. I knew this might make the day even longer than the first, but this was critical for team learning and new improvement ideas.
The team completed the day 2 changeover in 5 hours and 1 minute and looked really tired and uninterested in reviewing things in the meeting room. Undeterred, I brought them together and got their immediate feedback. One of the team members pointed out that while the individual team members had simpler and safer methods to do their work, there was no real coordination of effort between the six team members doing the work. This was a revelation, and he was energized to build something that we could try out the next day. The team was spent and went home to rest and hopefully relax a bit.
The next morning, there was a flurry of activity, as the team came together to develop ways to coordinate efforts across all people doing the work. A large white board was developed to track the activities of the team members and show status before the changeover was to start as well as during the changeover. It wasn’t completed before our next test, but we decided to start using it in the afternoon.
Using the new ideas from the morning, the team completed the changeover in 3 hours and 17 minutes. Even though they were still an hour away from their goal, they were extremely excited about what might be possible. None of them remembered completing a changeover of this complexity in less than 3 hours and 30 minutes. I told them that on day 4, we would be asking the crew, not the team, to try the new changeover procedure. This meant that we not only had to complete the improvements, but also have to train others in our new approach. Now the team was nervous. How would they train people who had never seen our new procedure in such a short amount of time? I assured them that we would be just fine. They all went home a bit skeptical, but energized.
Training in an Hour
The team came into the meeting room on day 4, wondering how they would be able to transfer all the changes to the crew to use that afternoon. I told them we would do it in a very simple process: “Tell, Show, Do.” This means each team member would be paired up with a crew member one hour before the changeover preparation was to begin. They would first tell their partner about the new procedure. Next, they would show how to do the procedure. Finally, they would have their partner demonstrate their understanding of the procedure. This technique would bring out questions and full understanding in a short amount of time. By describing the process early in the morning, the team could think about it as they were working on their improvements.
By lunchtime, all the major improvement work was complete. The board was upgraded to show status of each task for each of the six crew members in “swim lanes”. There was a timeline from two hours before the changeover was to start (preparation steps) to three hours from the changeover start, in 30-minute segments. The idea was to complete every preparation task before the line stopped running and every changeover task assigned in less than three hours across all six swim lanes. Every task had a red magnet on it, and when complete, it was to be switched with a green magnet. If one of the crew members was still red in their swim lane while another crew member was green, he or she could be asked to help the crew member who was behind.
We brought the team and the crew together just before the training was about to begin. We thanked them and told them the team was doing their best to make this the safest, easiest changeover possible, and they would be pairing up and showing them all of the new changes. We asked them to try everything in the new way, in as safe a manner as possible, and we would get their feedback following the changeover. If they thought anything was unsafe, they should determine a safe way to complete the task and we would make the appropriate changes afterwards.
The one-hour training started and everyone paired up and walked around discussing and trying the changes. The white board was placed prominently in front of the supervisor office, and everyone could see what was happening.
It’s OK to Ask for Help
After the training was complete, the two-hour changeover preparation began. This preparation was being done while the line was still running. Crew members had to watch the line as well as complete their preparation steps. Team members shadowed the crew members and coached them in the new procedure, but they were not allowed to do the work for them.
Back at the board, the team leader and shift coordinator were turning some of the red magnets green, as preparation tasks were completed. I walked up to the board and asked them what they were seeing. They weren’t really sure what I meant. I pointed out one of the swim lanes had many green magnets, meaning one of the crew members was an hour ahead of everyone else. One of the other swim lanes had all red magnets and was falling behind. I asked them what they thought they should do. They were unsure, so I pointed out that Green could help Red catch up. I left them, hoping they would take the initiative to get help for Red. Three minutes later, I noticed they hadn’t left the board to get help, and Green was getting further ahead of Red. I returned to the board and asked them if they were going to get help for Green. This time, they said they would. I left them but didn’t go far. I noticed they weren’t making any moves or approaching crew members to get help for Red. I went back to the board and said, “let’s go see Green and ask her to help Red.”
They grudgingly walked with me up to the mezzanine, where Green was working. I introduced myself to Green and told her she was doing great and was way ahead of schedule. Then I asked her if she would be willing to help Red, who was getting pretty far behind. She said she would be happy to, and walked with us to Red, who was appreciative to get help. The light bulb went off for the team leader and shift coordinator and they started to make more moves to drive Red tasks to Green.
Back at the board, every time a red magnet was switched to green, the team leader and shift coordinator would high-five each other. There was no way the team would fail now. One of our other team members found a large monitor and placed it in the window of the supervisor office and started a timer for everyone to see how long the changeover was taking.
As we approached the two-hour mark, it became apparent we might meet our goal. People started to get really excited and the shift coordinator was making all of the moves he could to ensure a win for the team. At two hours and five minutes there was a bunch of cheering and clapping. Everyone thought they were done. It was a false alarm, however, as the Quality Department had not yet signed off on the new product being produced. One of the team members went to the Quality Office to get a representative to look at the product and do the appropriate tests required. At two hours and ten minutes, all of the approvals were received. There was a roar of applause and a bunch of hugging all over the place. I doubt that has ever happened before in the plant.
We brought the team and the crew back into the meeting room to get their feedback. To a person, they didn’t think what we had done was possible, but now realized it was. They realized the importance of coordination, help, and coaching. The team decided they would train all of the other crews in this way, to ensure full understanding and buy-in.
On the day of the report-out, each team member admitted they didn’t think we would be able to reach our goals. It was hard for me not to say, “I told you so!” If I were to pick the most important changes they made, it would be the coordination and visualization of effort. Everyone knew who needed help and what they had to do to win.
The Path to Consultancy
I worked more than 30 years for a multi-national company. During that time, I had the opportunity to help teams and solve problems all over the world, from the US to Europe to Asia. I worked in five distinct industries and had many roles, from engineering to operations to continuous improvement. I enjoyed most of what I did, but realized something was missing.
I worked more than 30 years for a multi-national company. During that time, I had the opportunity to help teams and solve problems all over the world, from the US to Europe to Asia. I worked in five distinct industries and had many roles, from engineering to operations to continuous improvement. I enjoyed most of what I did, but realized something was missing.
When you work for someone else, you meet their requirements and work on their assignments. You don’t always get the opportunity to pick your projects. Sometimes you have to work on things that have nothing to do with your chosen field or interests. But, that’s life in a big company.
I used to take time off and help friends identify and implement improvements in their own businesses. I would take a day, travel to their location, and walk through their process with them. We would spend time with the people, processes, and equipment, reviewing the issues and problems in their business. At the end of the day, I would help them lay out a plan to improve things, which they were able to use after my visit. I enjoyed doing this, and thought I could become a consultant after I retired from my primary career.
In April 2018, I was visiting a local company, and spent the day doing what I enjoyed, reviewing their processes, people, and issues. Following a wrap-up meeting, I told my contact I wanted honest feedback on my visit. I felt like I could use this feedback for the time in the future when I intended to consult. Maybe in about 3 to 5 years, I said. He said he would let me know what he heard and we left it at that.
One week later, I was downsized. While this was surprising to me, I didn’t feel bad about it, because I felt something better would come of it. I just had to figure out what that was. It didn’t take long, as I realized I had the opportunity to forge my own path as a consultant.
Downsizing with an upside
I placed a call to my friend from the week before and let him know I would now be available 3 – 5 years sooner than I expected to be. He seemed excited to hear that and said he would talk to his plant manager to see if he was interested in letting me help them execute the improvement plan we had developed together. The plant manager was willing to use my help. Now I had to figure out all of the details required to open and run a consulting business.
Luckily for me, and for many others, there are ample resources willing to help and support small business owners. Using those resources, a lot of networking, and tons of phone calls and meetings, I established my consultancy in May 2018. Once done, I was able to start working with my first client. We decided to run a Value Stream Mapping session to lay out a continuous improvement strategy for the plant in June. I had run many such sessions in my prior company. Now, I had to put one together with a group who had little to no experience with this approach. I knew I had to prepare them for what was going to happen and do everything possible to ensure they had a great experience and beat their expectations.
Success is in the details
I spent many days at the plant, preparing them and myself for the Value Stream Mapping event. Every detail was critical, from the layout of the meeting room to the activities each day and the food we would be feeding the attendees. The people at the plant were intrigued by how involved I was in even these details. I kept telling myself and them that it was all for ensuring a winning experience.
The first day of the event, we had over 50 people attend, and we broke them up into three working teams, with facilitators I had trained in advance. Throughout the week, each of these teams identified waste in their processes, ways to reduce the waste, and improvement efforts and projects to implement over the next few years. It was hard work, but the team members seemed to be having a good time and were energized by the opportunity to create their future. I was having a blast, realizing I was helping people do something they had never done before.
By the end of the week, all teams had strategic plans they were committed to implementing. Corporate leadership came to the plant for the report out and was extremely pleased with the results. After the event was over, I reviewed my approach with the leadership team to see what they thought. They were very happy and even suggested I could help them with a number of other improvement efforts over the coming months. This reaffirmed my belief that I had chosen the right path.
The reward for good work is more work
A few months later, I received a call from the corporate supply chain director for the same company. He told me I had been recommended to him by the plant manager and he wanted my help with another improvement project. I was elated and scheduled the work for August.
Since those early days, I have had the good fortune to acquire more improvement efforts for multiple locations of the same company and other companies as well. The more I do, the more I learn, and the more fun it has turned out to be. I have the opportunity to help people and do it in a way that is fun, engaging, and energizing. I am so glad I didn’t wait to get into consulting, even if I needed a nudge to start.
Communication is Critical
In 2010, I was helping a team in Hilliard Ohio simplify the method they used for changing over a production line from one product to another.
The team came up with many ideas to simplify things and make things safer and more efficient around the line, and it looked like they were well on their way to reducing the changeover time by more than 50 percent, which was one of the key objectives.
In 2010, I was helping a team in Hilliard Ohio simplify the method they used for changing over a production line from one product to another.
The team came up with many ideas to simplify things and make things safer and more efficient around the line, and it looked like they were well on their way to reducing the changeover time by more than 50 percent, which was one of the key objectives.
A Special Job for Steve
On the afternoon of the third day, they identified some work that required the help of an electrician who worked at the plant. Not just any electrician, but a specific electrician, let’s call him Steve, who happened to work on the overnight shift, from 11 pm to 7 am. He had special programming skills and the team wanted to have him do some work that evening, so that they could test out the changes the next morning.
The team leader, let’s call him Tom, wanted to write an email to the electrician, so he would know exactly what was being requested of him the moment he came to work that evening. As Tom wrote the email, it became apparent the request was complex and could be interpreted in many ways. In addition, if the electrician had questions, he would have to wait until the next morning to get them answered. This meant that our work request was at risk.
Never one to be shy, or keep my big mouth shut, I volunteered to stay at the plant until the electrician came to work that evening. Because I was the one traveler on the team, and the hotel was less than 3 miles away, I figured I could sacrifice my evening easier than the rest of the team. Besides, how long could this take? We had the email, which appeared to be pretty well written.
Comprehensive Communication
Steve the electrician came to the plant at around 10:15 pm that evening, and I met with him soon after. I told him all about the team and their request and asked him if he would take a look at the email soon. He agreed and said he would find me if he had any questions. I left him as he prepared for his shift.
In less than 15 minutes, Steve found me in the meeting room. He had many questions. Apparently, the email wasn’t as clear as we thought. We started talking about the note and I realized that just discussing the note wasn’t going to be enough to answer his questions. We took a walk to the production floor and reviewed all of the work the team had done so far and the programming request. We had to call for some downtime so we could lock out the equipment and climb up on top of it to look at some specific details and measurements that had been left off of the request.
We dug deeper and kept finding information that had been left off of the note, but was critical to the changes being requested. We did this all over the line until Steve was satisfied he had all of the information he needed to safely and properly make the changes for the team. I was very happy to hear that and as I left the plant, I realized how long a day it had been for me. It was 1:15 am when I arrived at the hotel. Having started the day at the plant at 6:00 am, this was a new Kaizen record for me.
New Record Set, New Lesson Learned
On the morning of the fourth day, the team came in and I told them the story of my meeting with Steve. They quickly realized their information left much to interpretation, and it was critical that I or someone else should meet with Steve the prior night. Then, we verified all of the changes Steve had made for us. Everything worked as we had hoped.
At the end of the Kaizen week, the team was proud to report that they beat all of their safety and productivity goals. In addition, they learned an important lesson: no matter how clear you think you are in your communication, it’s better to review things in person to make sure the person receiving the information truly understands what you are asking of them.
I am proud to say that I have never beaten my personal record of longest day spent on a job site in the years following this event. I am also proud to say that I learned how critical communication is and I now teach all of my teams that same lesson.
Line Up and Do the Right Thing
In 2011, I was asked to facilitate a Kaizen in Pensacola Florida. The problem to be solved was to improve material flow through the plant. Specifically, there were millions of square feet of goods in process, and items were getting lost, damaged, and generally causing confusion and chaos in the plant.
In 2011, I was asked to facilitate a Kaizen in Pensacola Florida. The problem to be solved was to improve material flow through the plant. Specifically, there were millions of square feet of goods in process, and items were getting lost, damaged, and generally causing confusion and chaos in the plant.
Building 37
After training the team in Lean concepts, we took a walk out into the process to see what was happening. These Gemba walks can be quite eye-opening, and in this case, it made the problem very real to all team members. There were literally hundreds of pallets of material all over the plant, with much of it stored in a building they called 37.
In Building 37, there was no rhyme or reason to the way materials were stored. These materials were stored for various processing lines, but there was no way to know what was being stored and where to find it. It was obvious something drastic had to be done.
The team developed a concept early in the week that made storage and retrieval of the materials more manageable and thought they could organize and store everything in one location, rather than all over the plant. They determined that they could use Building 37 for this purpose, but would need to make the building more visual and create some rules around storage of materials.
Creating Visual Organization
After many different layout suggestions, we came up with a scheme we thought would work. We decided we needed to move everything out of Building 37, in order to reorganize and line out the space in accordance with our new recommendations. We also realized that we would have to clean the floor and paint it to make it as visual as possible and easy for everyone to use and manage. Painting the concrete floor was something the team didn’t want to do. In the past, forklifts tore up the paint and the lines would be lost quickly. Instead, they did some research and found a company out of southern Georgia with a technology to stain concrete, rather than paint it. It seemed like this was a good option, so we placed a call with them to see if they could come and help us.
To our good fortune, they were willing to drop what they were doing and drive more than 4 hours to meet with us and do the work during the Kaizen week. We told them what we intended to do and the size of the building to be stained. They estimated 28 gallons of yellow concrete stain would do the trick.
All Hands on Deck
We spent many hours moving over 1100 pallets (2.3 million square feet) of ceiling tile out of Building 37 into the open air. We crossed our fingers that it wouldn’t rain overnight. After we moved all of the material out, we swept and scrubbed the floors. The whole team pitched in and we were almost finished before the concrete staining company showed up in the late afternoon. They helped us finish up and started going about their work.
Most of the team members had to leave by 6 pm that evening, so I volunteered to stay with the concrete staining company, who was busy doing their work. In the middle of it, they realized that 28 gallons of stain wouldn’t be enough. They placed a call and sent a runner down to the plant with more stain. The runner happened to be the wife of the owner, who had just put dinner on the table. She dropped what she was doing to help us.
Grievance to File
Around 7 pm, I was approached by a very tall and unhappy Pensacola employee, who happened to be in their workers’ union. He wanted to know what was going on. I explained that our Kaizen team was transforming Building 37 in a way that it would be safer and easier to find and retrieve materials for the production lines. He wasn’t happy with my answer. What he really wanted to know was why the union employees weren’t doing this work. I explained that our team decided concrete stain was the best way to line the floors, given the issues with forklift traffic, and since this technology and equipment wasn’t available in the plant, we had to utilize outside contractors. We wanted to keep this work in-house, but that option wasn’t available to us.
Again, he wasn’t happy with my answer, but really didn’t have a valid argument as to how the work could have been completed with existing Pensacola employees. So, he angrily stormed off, vowing to file a grievance. Around 10:30 pm, all the lines were stained into the floor, and the contractors were finished. I was happy to see them leave, as I needed my rest for the next day of the Kaizen.
Good Intentions, Great Results
We lucked out, there was no rain overnight, and we spent the morning putting everything back into Building 37, this time in a logical sequence and order for the materials to be easily found. The lines really helped, and to this day, the plant uses this system to keep materials organized for all of their production lines.
I never found out if the union employee filed a grievance, but even if he did, we had done the right thing for the plant with the best of intentions.
Kaizen Every Day – The Armstrong Lockout
In all my years doing continuous improvement work, I worked with teams during Kaizen events of short duration, or influencing continuous improvement behavior daily. Never did I think I would be doing 6 months straight of Kaizen. That is, until the Armstrong Lockout.
In all my years doing continuous improvement work, I worked with teams during Kaizen events of short duration, or influencing continuous improvement behavior daily. Never did I think I would be doing 6 months straight of Kaizen. That is, until the Armstrong Lockout.
Supporting Operations During a Lockout
In 2011, Armstrong World Industries and their Marietta PA ceiling plant workers were unable to reach a contract agreement by the time the contract expired. Historically, Armstrong would allow the employees to continue working without a contract, until negotiations were completed. There was always a risk that the employees would walk out any time without notice, but that had never happened. New management decided that it wasn’t worth the risk and decided to send a message to the union by locking out the hourly production and maintenance employees until an agreement would be reached.
Armstrong was ready for this contingency and had made an arrangement with a company that supplied replacement workers and security to companies in similar situations. These workers would move to the site and fill in for the employees until a resolution was reached. Many of the Armstrong engineers, retirees, and other technically skilled corporate employees were asked to train and supervise the replacement workers and also run the complex equipment. Some non-union workers came from other plants in the Armstrong system to help too.
I had been helping a project team building a plant in China. When I returned to the United States in July, I was asked to help support the Marietta plant in an operations role, alternating between equipment operations, training, and supervision.
Armstrong employees were required to meet at an off-site parking lot, and then board a blue bus with blacked-out windows that would take us to the plant. We were to work 12-hour shifts, 6 days a week (we could work 7 days a week if we wanted to) and weren’t allowed to leave the plant property unless we had a personal emergency to attend to. Some of us, including me, had pre-shift supervisor meetings, that extended our days to 13 ½ hours. Needless to say, we all wanted the lockout to end quickly. We also wanted to make sure that no customers would feel the impact of reduced service levels due to the lockout, so we were committed to keeping the plant running, 24/7/365.
A Plan to Reduce Downtime
In my first weeks at the plant, I spent much of my time helping to solve downtime issues and coordinate efforts of workers who were unfamiliar with the equipment. It was apparent that the plant wasn’t left in the best of shape by the Armstrong union employees and they were using their experience to compensate for low performing equipment. We didn’t have the experience, so it was clear that something would have to be done to make the equipment more reliable.
I started to assess the factors impacting equipment performance and realized that many of the downtime issues could be solved with some basic line maintenance – conveyer guiding, leveling, and squaring. Lucky for me, this was and is an area of experience and expertise. On a Saturday in August, I was talking with the plant manager, and suggested that I could provide more value at the plant if I were to work with maintenance to solve some of the basic conveying issues I saw in my time at the plant. He was intrigued and asked me to show him what I meant. I took him on a tour of various parts of the line and pointed out the issues I was seeing. Then, I described my plan to solve those issues, one part of the line at a time. More intrigued, he called the maintenance manager and asked him to join us for a tour.
The maintenance manager met us at the line and took a tour with us. He was a bit skeptical, but after about 30 minutes, he was convinced that I might be on to something beneficial. He asked me what I needed to start the work. I told him I could work with a skilled mechanic to start making line improvements. He asked me when I would be ready to start. I was ready any time.
A Team on a Mission
On the following Monday morning, I was assigned a mechanic named Joe. Joe and I took a tour of the lines and I shared my vision of the work we could do to improve performance. He was enthusiastic. We decided we would tackle one line at a time and prioritized the first line to work on. We agreed that we would do work in 1 to 2-hour blocks and try to utilize downtime to get our work done. We also agreed that since the lines were running so poorly, we could make our own downtime blocks, as long as the crew and supervision was aware and agreed to our plan.
At first, no one wanted to give us any downtime to do the work, so we were frustrated and couldn’t plan well for the work. The only way we could make a real difference would be to convince one of the acting supervisors to take a chance and let us shut a line down in a planned way. I was persistent and convincing and finally had the approval of a line supervisor to try out our plan on his line.
Joe and I got to work, leveling, squaring, and improving the guiding on the first line. We worked one section at a time, and after about a week, the line was running noticeably better. After three weeks, we were setting production records and others were noticing. All of the sudden, Joe and I were getting more calls for help than we could manage. So, we asked for more mechanics to help. We started expanding our work and touching all of the lines in the plant. We also taught the techniques to others so that they could solve problems too.
From time to time, I would get calls on the radio from mechanics who wanted my advice and help and they would meet me and take me by maintenance cart to the site of the issue for review. Now we were making a huge difference in the plant performance and the problems of the past were being solved in a sustainable way. Some areas of the plant looked nothing like they had prior to the lockout, as much of the equipment had been stripped of the problems that kept it from running reliably. Although tiring, this work was also exhilarating, and made working long hours fun. We could see improvement happening every day.
The Lockout Ends, But Improvements Remain
In January 2012, the union agreed to contract terms and was scheduled to return in the middle of the month. I was asked to stay on for a while to show the changes we had made to the plant. Many of the lines looked markedly different and were unfamiliar to the union employees. I gave tours of the line and fielded questions from the employees. For the most part they were appreciative of the changes, as they could see how the improvements would help them do their job in a safer, less stressful way.
The union president asked me specifically why I made the changes the way I did. I told him that due to our lack of experience and skills, we had to make the lines easier to run or we would disappoint our customers. We really missed our experts and were extremely glad they were returning. He liked my answer and ended up doing more of this improvement work with my assistance in the following years.
I am very proud of the work I was able to complete for Marietta during the lockout. I was also extremely grateful the lockout ended when it did. I was ready to go back to riding in something other than a blue bus with blacked out windows.