
Kaizen Success Stories
Real Manufacturing Results. One Kaizen at a Time
Explore real-world Kaizen success stories showing how manufacturing teams solved critical problems, improved performance, and created sustainable results.
Weld It in Place to Sustain It
Before I developed the Wheel of Sustainability, I had to find other methods to sustain the gains my teams worked so hard to develop during weeklong events. Here’s a story of the extreme lengths one team went to make sure no one could ever make a change to their improvements.
Before I developed the Wheel of Sustainability, I had to find other methods to sustain the gains my teams worked so hard to develop during weeklong events. Here’s a story of the extreme lengths one team went to make sure no one could ever make a change to their improvements.
I was requested to help a team in Armstrong’s Macon Georgia ceiling tile plant. They were experiencing jams at the end of the production line. These jams caused significant safety risk and high levels of downtime that affected the productivity of the operation. I was known for my efforts to improve flow on production lines and this was an extremely high value project.
I took a tour of the line and saw many opportunities to improve flow and reduce jams. I discussed my observations with the plant manager, and he agreed to assign a high skill team of line operators, mechanics, and the day shift supervisor to assist me.
We spent the first day of our event observing the flow of ceiling tiles as they traveled around the line over various conveyers. One area stood out above the rest: the twenty foot conveyer leading up to the flipper. Tiles were turning and entering the flipper in a skewed fashion. Every so often, they would get stuck and not flip correctly, causing the tiles behind them to back up and jam. People on the line had to rush around and clear the tiles off the line. Many times, they shut the line down and threw out a lot of damaged tiles.
We adjusted the conveyers and guides and tested our changes. The tiles were now going straight into the flipper. None of the other tiles were backing up and jamming. We had our solution. Our new challenge was to keep things in this optimal situation.
We brainstormed ways to sustain our improvements. We came up with ways to mark the conveyer rollers and guides. We considered drilling holes in the guides and pinning them in location. Then, one of our mechanics asked the question, “Now that we have the best location, why would let anyone make a change to it?” We looked at him and wondered what his idea was. He said, “Weld everything in place. Nobody can ever change it without a torch!”
He was right, of course. But were we willing to take such a leap and make our changes permanent? We decided to make further observations for the next two days, doing everything we could to make sure no one changed our settings during that time. To our relief, no changes were made, and more importantly, there were no jams.
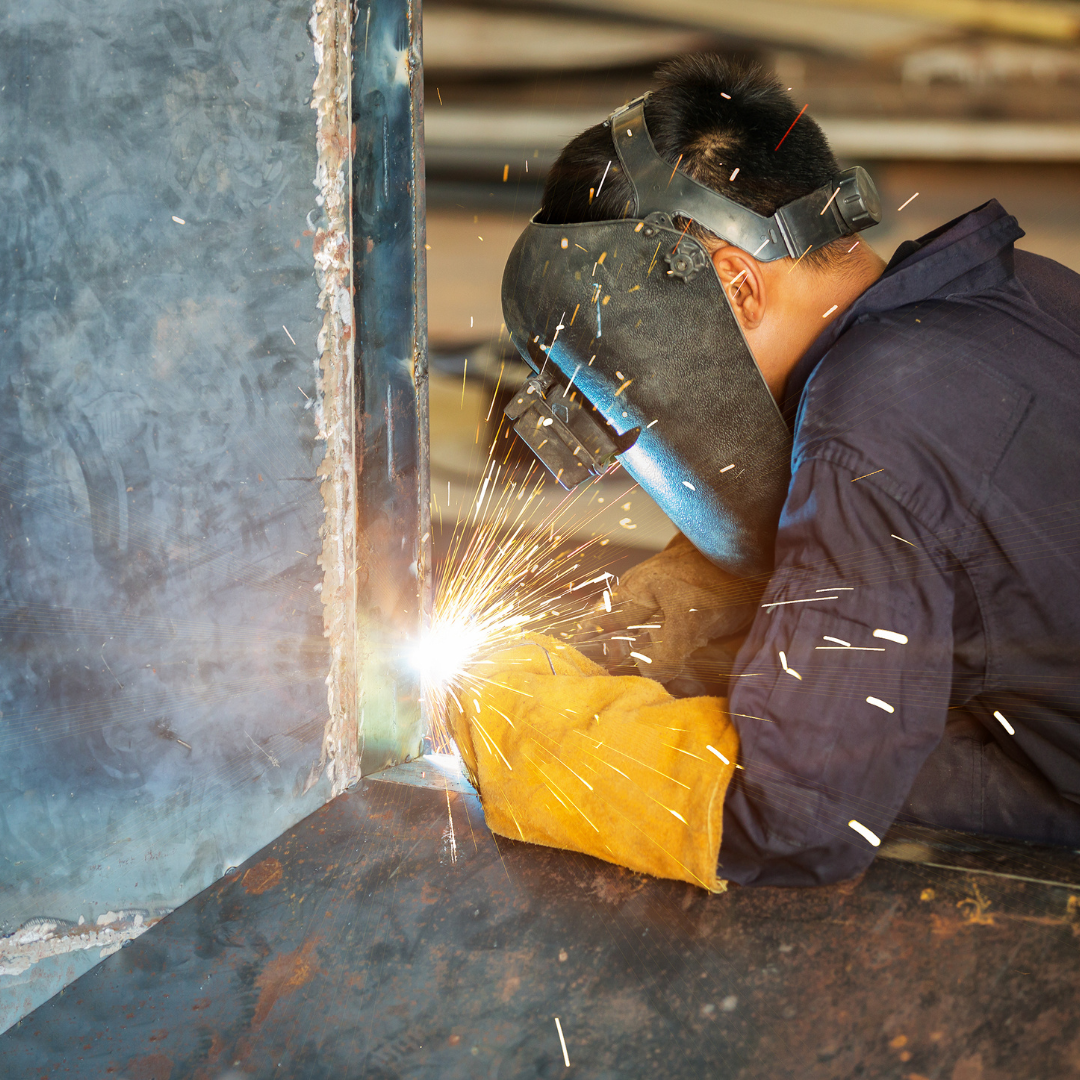
The next day, we took a leap of faith and shut the line down. Two of our mechanics welded all guides in place. Once everything had cooled down and was cleaned up, we started the line back up. The tiles entered the flipper squarely and without incident. Even though we knew this should work, we were all relieved.
We gave a tour of this and other changes we made to the line and our sponsors were impressed and pleased. Team members remarked how important it was to keep our changes in place from now on. We joked about keeping the “red wrench” (torch) out of the hands of our maintenance department, so that they wouldn’t take our welds out.
From time to time, on subsequent visits to the Macon plant, I would go to the production line and verify that the guides were still welded in place. Ten years later, everything was as we left it and the line continued its improved performance.
Visibility Equals Accountability
Do all your meetings happen in a room? Mine did, until I realized we needed to do something to shock the system and change our performance quickly.
I was the Business Unit Manager at Armstrong’s vinyl flooring plant in Pennsylvania. Our performance and profitability had been in a downward spiral for many years prior to my arrival and things weren’t getting any better while I was in charge.
One day, the vice president of manufacturing told us we needed to significantly improve our scrap and productivity performance or he’d find somebody who could. It didn’t take a lot of soul searching to know this was an ultimatum. I took a close look at everything we were doing from a management standpoint. We were complacent in our approach and our performance mirrored that fact.
After sitting through another meeting hidden from view from our associates, I realized what I had to do. I needed to get the entire organization aligned around our most critical priorities: safety, quality, customer service, and productivity. Every time we had a meeting in a closed room, it was hard to tell what was agreed to and if any progress was being made.
With the help of my staff, we reorganized an area around the time clock. This was the location every hourly member of our staff utilized twice per day. They had to use it or they wouldn’t be paid.
We put the agenda for our production meeting to the left of the timeclock and action items resulting from the meeting to the right. It was a tight space and we typically had 12 people in attendance. The only way to accommodate everyone was to stand in a semicircle around the timeclock as we worked through the agenda. We had to stand in the main aisle in the plant. Every so often, we’d have to stop what we were meeting about and move out of the aisle to allow a forklift to bring supplies to one of our production lines.
It seemed like these supply runs happened more often than necessary, just to break up our meeting. But we persevered. It was loud, so everyone had to stand close to hear each other. This forced us to be concise and to the point. Whenever we had an action item, we’d write it on the large sheet of paper next to the timeclock. We put the item, owner, and due date on it.
In the meeting room, it would take many days or weeks to complete action items. Out in the open, things were getting completed more quickly than before. We observed our hourly workers reviewing the action items on the sheet. It looked like they were interested in what was going on.
One day, I got a question from an hourly worker about one of the action items – what did it mean and what could they do to help it get completed? This was a breakthrough! All of a sudden, people were paying attention to our efforts and trust was growing as progress was being made.
No one wanted their name on the action item sheet for too long. They were getting pressured to complete their responsibilities. Soon, our performance improved, the business was stronger, and we weren’t under the threat of replacement as much as we had been.
Raise Your Standards and Take Ownership
I was the industrial engineering manager at a ceramic tile plant in New York. We made mosaic tiles. The color went all the way through the tile. Mosaic is also a word used to describe the artistic patterns we made as special orders from our customers.
I was the industrial engineering manager at a ceramic tile plant in New York. We made mosaic tiles. The color went all the way through the tile. Mosaic is also a word used to describe the artistic patterns we made as special orders from our customers.
For years, we had a department that had the task to take any requested design and turn it into reality through manual assembly of the many different colored tiles we made. Sometimes this required tiles to be cut, an extremely slow and difficult process to accomplish. These special orders took many weeks to complete and were very expensive.
We heard about a technology called “water-jet” cutting that was being used at a few locations in our parent company, Armstrong World Industries. Using high pressure water, you could cut into almost any material (metal, plastics, etc.) and get a clean and precise cut. We were intrigued and felt there might be an application for this technology at our plant.
We arranged a visit to two of our plants, one, a ceiling tile plant in Beaver Falls Pennsylvania, and the other, a vinyl flooring plant in Lancaster Pennsylvania. We took the company van and I was joined by two operators, a programmer, and an engineer.
When we got to the vinyl flooring plant, we were met by a project engineer, who oversaw the samples department. They were using their water-jet to cut small pieces of vinyl flooring out of the larger rolls, so that they could send samples of different colors and patterns to customers. The shapes being cut were rectangles, so although this saved a lot of labor, we weren’t convinced it would help us cut complex shapes into our ceramic tiles.
Our team was convinced that in order to program and cut complex shapes and designs, we’d need someone specially trained and highly compensated for this new skill we were seeking. As an industrial engineer, I knew it wasn’t a good idea to have such a highly specialized job very few would be able to master. It limited flexibility and raised operating costs.
At the ceiling tile plant, we were met by a production operator. She showed us how she programmed and cut complex designs into the face of ceiling tiles using the water-jet. We were intrigued and impressed by the variety of shapes and designs she was able to cut. When we asked her how difficult it was to learn to program the equipment, she told us it was extremely simple and intuitive. You could either import a CAD (computer aided design) drawing or scan an existing design and the machine would figure out the cuts to make.
Our team members weren’t convinced that anyone could do it. They were ready to leave for home when I asked the operator if she’d provide some basic training and let our operators try it for themselves. She said yes, and I was able to convince my team to take the extra time to decide about the skills needed.
They picked out a couple of designs and after an hour of training, they were cutting ceiling tiles exactly as programmed. Now they knew they could do it and easily apply the water-jet to our ceramic tiles. On the way back to our plant, there was excitement about how easy this new technology was to master.
A few months later, we purchased and installed the new equipment. The plant was able to make beautiful mosaic patterns for many years thereafter and had the flexibility to use almost any operator to do it. Although seeing is part of believing, it wasn’t until the team actually tried their hand at the process that they were convinced it was a good idea. The lesson: open your mind to fully experience your options before counting out a solution.
Change Your Perspective
I moved to Baltimore to be the industrial engineering and quality manager at a ceiling grid factory. We had just consolidated three plants into two, following a joint venture. Early on, changes were happening so fast that my plant manager informed his boss that he wasn’t comfortable with the direction of the new company. He offered to stay as long as necessary to bring his (yet unnamed) replacement up to speed.
I moved to Baltimore to be the industrial engineering and quality manager at a ceiling grid factory. We had just consolidated three plants into two, following a joint venture. Early on, changes were happening so fast that my plant manager informed his boss that he wasn’t comfortable with the direction of the new company. He offered to stay as long as necessary to bring his (yet unnamed) replacement up to speed.
He was informed his services were no longer needed. His replacement was ready to take over operations. So, he packed up and left the same day. Much of this wasn’t told to us immediately. We just watched our leader leave the plant, never to return. We wondered what was going to happen in the interim.
The next day, we met our new plant manager, Jim. He arrived at the plant just before lunchtime and introduced himself to each of us separately. He had been a salesman for the competing company that had merged with ours.
Jim seemed highly motivated and excited to be at the plant with us. He told us he was committed to our success and would help us through the transition of the joint venture. This was reassuring and we were happy to have Jim as part of the team. Until the next day. At 10 am, Jim hadn’t shown up for work. The plant kept running, but we wondered if something had happened. Just before noon, Jim arrived and acted as if there was nothing wrong. For the next few weeks, Jim came to the plant at a time the rest of us considered “late” every day. Sometimes, he would tell us he was in a meeting. Other times, he said he was playing golf with some of his customers.
This was unusual behavior for people who work in operations. Factory staff members tend to arrive early in the morning and stay until the evening. Jim was different, and it was beginning to weigh on the staff and the operations crew. We’d get questions about where Jim was and why he wasn’t with us in the plant. Many times, I’d walk by an office and observe others complaining about Jim’s “lack of commitment.” I was commiserating too. Finally, I decided I should try to do something about it, if no one else was willing to do so.
Our engineering manager wished me luck and said he would “miss me when I was gone.” I told my wife I felt I had to say something to be part of the solution. She told me that she believed in me, but was prepared for the ramifications of the discussion.
The next morning, after Jim arrived, I asked if I could talk to him about something important to me and the plant. As I described my observations to Jim, I told him I realized as a salesman, the hours he put in were likely different from running a factory. We needed his leadership, guidance, and his commitment to be with us during key morning meetings and other critical times during the day. He wasn’t able to do that while on the golf course or whatever errands he was running in the mornings.
I gave my feedback for what felt like hours, but it was probably 10 minutes. Through it all, Jim didn’t say a word, he just listened. After I finished, I thanked him for giving me the opportunity to speak with him and left his office. It felt strange to say all those things without a response, and I told a few of my team members that it might be my last day at the plant, but at least I followed my conscience. I hoped I wouldn’t have to look for another job.
Over the next few weeks, without acknowledging our meeting, something changed. Jim started showing up at the plant earlier in the morning. He got extremely involved in our meetings and critical plant decisions. Soon, he was no longer an outsider; he had become our leader.
Two years later, as I was preparing to move on to my next assignment, Jim called me into his office. He reminded me of the day I brought my concerns to him and how it changed his perspective and approach. Now that we were close friends, I said, “You #%$@, you never said anything that day and never acknowledged it until now. I thought I was about to be fired!”
He said, “I really did appreciate it, but at the time I didn’t know how to respond. Then, as time went on, I just wanted to leave you hanging. Now, I just am happy to get that reaction from you!”
Be Careful What You Ask For
I was the plant operations manager at Armstrong’s St. Helens, Oregon ceiling tile plant for three years. During my tenure, I was able to test and refine my management and continuous improvement approach on an operation that employed just under 100 people. I made many mistakes and I’d like to think I learned from each one of them. Sometimes, it took me a few times to learn from the same mistake.
I was the plant operations manager at Armstrong’s St. Helens, Oregon ceiling tile plant for three years. During my tenure, I was able to test and refine my management and continuous improvement approach on an operation that employed just under 100 people. I made many mistakes and I’d like to think I learned from each one of them. Sometimes, it took me a few times to learn from the same mistake.
With around the clock responsibility, I was the one who was called in the middle of the night when there was a significant safety, quality, human resource, or productivity issue. If I couldn’t resolve the issue, I would then escalate it to my boss, the manufacturing manager. I hated waking him up, but sometimes I had to. I was determined to keep those occurrences to a minimum.
It seemed like most critical issues happened around 2 am. If I got one call after going to bed, I usually could get a restful sleep during the night. If I got two or more calls, then it was hard to sleep well. I tried not to be too grumpy when I got to the plant the next morning, realizing my supervisors were fighting the issue far longer and were doing everything they could to avoid calling me.
One evening, the supervisor called me because he had suspicion one of our employees had broken our “no alcohol” policy. Because he was the only manager at the plant at the time, he needed a witness. I came in, saw clear evidence of alcohol use and drove the employee to get tested. He denied it the whole time, saying he had taken some cough syrup before coming to work. When his results came back at 3 times the legal limit, he had to admit his indiscretion. I drove him home and we subsequently terminated him once he was allowed back on the premises.
After a particularly challenging week, with multiple calls in the middle of the night, I remarked to one of my supervisors, “Just once, it would be nice to get a call in the evening saying that everything’s ok.” He agreed with me, and we laughed about all of the situations that forced those late evening calls.
Two months later, the plant was running smoothly. Safety, quality, and productivity were near record levels. The vibe in the plant was positive and there was nothing we couldn’t accomplish. I found myself bragging about our employees to anyone who would listen.
One evening, after having a particularly nice dinner at home, I decided to go to bed at 9 pm, so I could visit with the overnight shift early in the morning. After falling asleep quickly, I woke to the telephone ringing. I had been conditioned to expect the worst. On the other end of the line was my evening shift supervisor, who told me, “Adam, this is Jim. It’s 10 pm and I wanted to let you know that everything’s ok!” I couldn’t help but laugh as my words came back to haunt me.
Image is Everything – Understand How Your Reflection May Look to Others
I have been a small business owner for a few years. My company consists of me, my wife, my son, and my dog. I quickly learned I am responsible for everything that goes on. Nowhere is this more critical than customer acquisition.
I have been a small business owner for a few years. My company consists of me, my wife, my son, and my dog. I quickly learned I am responsible for everything that goes on. Nowhere is this more critical than customer acquisition.
In my first year, I was fortunate enough to work with people who had seen what I do and how I do it when we worked together at Armstrong World Industries. Because I had already built strong relationships with them, they trusted me to utilize my approach to their problems in their companies. When it was time for me to expand beyond those I knew, I learned I had to build that trust in other ways, without a prior relationship. Sometimes trust was built easily, other times not so much. Here’s a story about how I didn’t build trust in a way that led to a business relationship.
During a Google search, a local business leader reached out to me to see if I could help his company with a couple of Kaizen events. I was excited for the opportunity and scheduled a visit.
We met in a conference room and I explained my process for the visit. I would get to know their leadership team, take a Gemba walk, and then put together an action plan for the work in which we could engage. They were polite, but seemed skeptical. I was confident, maybe too confident, that I could win them over.
After the initial meeting, we took a walk through their manufacturing process. I met many people and asked a lot of questions and could see many opportunities to apply my skills to help the business improve their safety, productivity, quality, and customer service. I took copious notes and built a plan in my head to create a shared vision for our journey together.
When the Gemba walk was over, three people stayed with me to review my observations and plan: the director of operations, the plant manager, and a young engineer. I thanked them for the opportunity to learn more about their business and then started describing the opportunities I saw and believed I could help them with. Reviewing my Kaizen approach and the Wheel of Sustainability, I said most of these issues could be solved in a week or less, using Kaizen events.
The group looked at me skeptically and I just plowed forward, describing how the Wheel of Sustainability works and how teams engage with it to solve problems in a sustainable way during the Kaizen week. And that’s when the engineer said, “I don’t see it. I don’t think you and a team can do all that you say you can in a week or less.”
I tried to assure him and the rest that we could, but clearly, I hadn’t instilled the confidence in them and built the image of what “good” looks like in a way that was meaningful and real to them. Although they gave me the opportunity to write a proposal for the Kaizen events, I never got the chance to work with them.
This was my fault. Luckily, I realize it now. It is my responsibility to build the image of what is possible in a way that is clear to my audience. It must be in terms that make sense to them, so trust is built, and we can partner to solve their critical problems.
I still have a lot to learn, but I feel that I am on a good path to create the trust that is so critical for lasting business relationships.
Why Would You Treat Your People that Way?
Our fiberglass ceiling tile plant in Ohio got their board stock from another company (let’s call them Vendor X). They had some problems with the quality of some of the boards they received. As Vendor X was a critical partner, they decided to co-host a Kaizen event to eliminate the quality problems.
Our fiberglass ceiling tile plant in Ohio got their board stock from another company (let’s call them Vendor X). They had some problems with the quality of some of the boards they received. As Vendor X was a critical partner, they decided to co-host a Kaizen event to eliminate the quality problems.
The first day, we met at the ceiling tile plant and laid out the issues we were experiencing. Walking through the receiving and production areas, we identified several quality issues that could be rectified from the plant’s internal processes. We then agreed to walk the Vendor X process on the second day.
Walking through Vendor X’s factory, we saw many impressive safety ideas we could emulate back at our factories. One was the painting the bottom stair red, so everyone would know it was the last stair before reaching the ground. This idea was implemented after they learned some of their people were missing the last step and had tripped or fallen. Once implemented, these issues went away.
The process to make fiberglass panels was fascinating and somewhat like the process to make mineral fiber ceiling tiles. We learned how molten fiberglass was spun into fibers and formed into long panels. Then, the panels were cut to finished lengths and stacked at the end of the line. Then, I saw something I wasn’t expecting. Instead of a barrier for the panels to hit and be stacked, they were hitting a worker.
This worker was taking the blow of the panel on his waist or stomach and letting it bounce off and then drop into a stack in front of him. I asked if this was a temporary situation and was informed it was a “normal” job in the factory.
This company, which was known for its focus on safety, was clearly missing a huge opportunity to eliminate a safety risk. They told us they had tried to automate it in the past, but it didn’t work and their employees preferred the current method of stacking. I couldn’t believe it could be okay to put their people at risk like this. It was clear their Leadership Commitment didn’t reach to this area of their process. I can’t imagine people are still treated that way in their factory these many years later. But, when I am having a bad day, I think back to that tour and realize that someone is always having a worse day! The lessons here: 1. No matter how good you think you are, there is always room for improvement; 2. Put yourself in the position of your people; and 3. Even someone who says they’re “OK” with a current process deserves to have it improved, if possible.
Blow It Up
Here’s a mining story from my time at Dal-Tile that involves blowing up a hill!
Here’s a mining story from my time at Dal-Tile that involves blowing up a hill!
We were invited to an annual mining training event (required MSHA training) at our talc mine in Van Horn, Texas. To get there, we had to fly to El Paso and then drive 120 miles in the middle of nowhere to our mining operations. Once we got there, we met Junior, the mining operator. He had spent his life out in the hot Texas sun and you could tell it by the condition of his skin. He lived on the mining property with his wife in a trailer and was one of the nicest people I have ever met.
After a day of training, we went out to dinner and spent the evening sharing stories, drinking, and dancing. Wayne, my boss, tried a shot of vodka with tabasco sauce on top and forgot to open his lips wide enough to avoid the burn. We all had a laugh at that.
On the second day, after a few hours of training, we were treated to a mining demonstration. We were going to clear some overgrowth on a hill by blowing it up. The only things I had blown up in the past were fireworks on the Fourth of July, so I was excited to see how it was done.
When we got to the hill, we were told there were 159 sticks of dynamite placed in three rows. They would be used to clear the growth and expose the talc for mining. Wayne and I got the opportunity to string the fuse through some of the sticks, while being assured by the mining operator we were perfectly safe to do so. I strung two sticks. Wayne was having such a good time, he strung around a dozen.
Then we were asked if we wanted to light the fuse to blow up the hill. I knew I did, and Wayne deferred to me. Since I had never blown anything up of this magnitude, I asked the operator what safety precautions we should follow. He pointed out the two vans with the motors running. Each one had enough capacity to take all of us away, should one of the vans fail.
Next, he told me the fuse between the sticks of dynamite took milliseconds to burn, but the main fuse I would be lighting had enough time on it to get us into the vans and approximately ½ mile away, where we would be safe.
I was a bit nervous, but I told myself the mining operator had done this many times before, so I would try to hide my anxiety. My natural inclination was to run as soon as the fuse was lit, but I thought that would make me look silly. So, I decided to do whatever the mining operator did. If he walked, I would walk. If he ran, well then …
He lit a cigarette, took two puffs and handed it to me. I bent down, held the cigarette to the fuse, and watched it light. Time stood still. I cleared my head and saw the mining operator walking slowly to the van. And that’s what I did. Wayne ran like a scared child and jumped into the van.
Once we were all in the van, we drove to the other side of the site and watched as the 159 sticks of dynamite exploded with a precision that took the face of the hill down exactly as planned.
We got back to the training room and poked fun at Wayne and any of the other folks who ran to the van. I would have too, but I had convinced myself to not panic. Was this the right call? I don’t know, but at least I had some fun at my boss’ expense!
These days, I work with teams to develop standard work to keep them safe and productive. To be sustainable, it needs to make sense to them. Although I don’t recommend lighting a fuse with a cigarette, it worked for the mining operator in Van Horn Texas.
The Journey is Long
After five years as Lean Champion, my voice wasn’t being heard so well. Sure, I was able to promote and facilitate Kaizen events and help people solve problems, but I was unable to move the leadership team to take the next steps in our Lean journey. Any time I spoke to our leaders about strategy, they were too busy to consider anything that deviated from their current operating approach.
After five years as Lean Champion, my voice wasn’t being heard so well. Sure, I was able to promote and facilitate Kaizen events and help people solve problems, but I was unable to move the leadership team to take the next steps in our Lean journey. Any time I spoke to our leaders about strategy, they were too busy to consider anything that deviated from their current operating approach.
I realized that I needed to engage an outside voice. Someone with credibility, who could say the difficult things I was saying with different words. Someone who could influence our leadership team to change their behavior in a way that would support our Lean transformation.
You’re Never Too Good for Growth
Two years into our Lean transformation we had undertaken a Lean assessment to see where we were and where the opportunities existed. Looking back, it was more tactical than strategic, but was appropriate for our maturity.
Now, I had an idea. What if we tried another Lean assessment, this time focusing on the leadership and strategic aspect of our efforts? When presented to our four Value Stream Directors, they seemed satisfied with their efforts and indicated they had this “Lean thing” down. I knew right then we were in trouble!
I met with my manager, the Executive VP of Technology, and convinced him that we needed something to open our eyes to the possibilities for the next steps in our transformation. But, if we used our internal resources to conduct the assessment, we would rate ourselves too highly. We had become complacent and overconfident. Our results were impressive. The product portfolio had doubled and time to market had been reduced from eighteen to ten months.
After receiving approval, I reached out to Mike, a consultant from Shingijutsu, who I had met four years before. He taught me that no matter how good you think you are, there are always ways to improve and grow. He agreed to join us at no cost. He was interested in how we were doing and had the freedom to do what he wanted. He flew in from Seattle and I joined him for breakfast on the first day of his visit. We talked about the current situation. He assured me that he had seen this many times before. He knew he could help.
Our first meeting was with the Leadership team. As they introduced themselves, most of them talked proudly about their team’s accomplishments and how they incorporated Lean into their processes. Each time, Mike asked them probing questions about their progress and approach. He exposed gaps in their efforts and understanding of Lean in a way that was respectful, but eye-opening. Team members took many notes during the discussion.
The Beginning of Breakthrough Thinking
For the rest of the week, Mike and the assessment team participated in many meetings and activities and identified huge opportunities in our Lean journey. Mostly aligned with my prior efforts, Mike had a way of communicating to the organization that had credibility beyond any internal resource.
At the review of findings, we presented four recommendations:
1. Learning starts at the top – leaders must demonstrate the behaviors of the change they want to make
2. Linkage – become in lockstep with customers and suppliers to ensure that everyone gets only what they need, when they need it
3. Stability – level the flow of work to drive the production system stress level down
4. Cycle time and quality – deliver only what the customer wants, when they want it, at the appropriate level of quality
Although these were not new ideas, the leadership team saw them as breakthrough thinking and instantly committed to them. One Director admitted that prior to the assessment he thought he knew Lean very well. Now, he was sure that he had much learning to do to become competent.
Following the assessment, there was a renewed commitment to Lean in the organization and many breakthroughs were made over the next year. For my part, I was extremely appreciative of the time Mike gave us and the renewed interest that was generated by his visit.
Cream Rises to the Top
I was working with a team in New Jersey to implement Training Within Industry (TWI) on a critical household cleaner line. Plant leadership saw this as a key element in their strategy to improve overall line performance.
I was working with a team in New Jersey to implement Training Within Industry (TWI) on a critical household cleaner line. Plant leadership saw this as a key element in their strategy to improve overall line performance.
In the initial Kaizen event, I trained twelve team members to competently create standard work and train others using the TWI method. Much like my first experience with TWI, the training method wasn’t natural for the team, but by the end of the Kaizen, they had all shown proficiency with it.
One of the hourly team members, Rita, seemed inspired by this “new” method for training. The rest of the team members agreed she had a flair for it and would do quite well training others on her crew.
When I got home at the end of the week, I was confident that TWI would help the plant improve line performance. I hoped the enthusiasm for TWI would continue. Over the weekend, I received a text from Rita, who was excited by what she had learned and had done further research on TWI and other Lean concepts. While this isn’t unheard of, I am always impressed how a winning Kaizen experience can move certain team members to want to learn more.
I sent Rita a congratulatory note and provided a list of my five favorite continuous improvement books for her consideration. She thanked me. I wondered if she would continue to take the initiative to learn more.
Boosting Confidence Through Training
Over the next few weeks, line performance wasn’t improving. I was asked to return to the plant to support the TWI rollout. Other issues had taken priority and the trainers hadn’t been given the opportunity to create standard work or train their coworkers.
I suggested that we have a refresher for the trainers and then practice training their coworkers with the standard work created during the initial Kaizen. Leadership agreed, and I was assigned to four team members, including Rita. I was curious to see what she had done in the weeks between the Kaizen and my visit.
It turned out she had been training some of the people on her crew and getting really good at it. She even gathered feedback at the end of each training session, asking for the level of confidence before and after the training. When her coworkers expressed their level of confidence had risen, it reinforced how important the training was to Rita.
It Takes One Good Leader
Over the next two months I returned to the plant for a few days each week to continue the training rollout. Rita participated every time. It was clear that she had become an amazing trainer. During one session, she taught the plant manager to change over a critical piece of equipment that only the highest skilled workers had previously done. We now knew this was going to work. Other trainers saw what Rita was able to accomplish and it boosted their confidence.
The following month, the line reached its performance objective and has stayed there since. I am convinced that the training process and Rita’s leadership contributed to this success.
The Vortex
Sometimes we don’t see what’s right in front of us. We just do what we do and deal with the problems that inevitably arise.
I facilitated a Kaizen event for a non-profit. Contributions were declining significantly. After taking a Gemba walk through the process, we identified the need to improve donor engagement. It was taking up to two months to acknowledge the highest value donations. No wonder donors were leaving in droves. Recognition was slow and not meaningful.
Two months before, I ran a workshop and donated the proceeds to Feeding America. I received a thank-you note less than thirty minutes after I sent my credit card payment. It felt good to be recognized so quickly.
We brought together a team and mapped out the donation acknowledgment process end to end. There were many points in the process where the information stalled. Of those, the worst was in the office of the VP of Finance. Information could sit in his office for weeks before anything happened. If he was busy with other duties, he might forget to take any action. A call from a disgruntled donor would restart the process.
It was so bad his office was nicknamed “The Vortex”. Things came in and were lost to the world. This Recognition of poor performance had to be turned around.
The rest of the week, the team worked on ways to eliminate The Vortex. Time was reduced from two months to six days. Unfortunately, major damage had already been done to donor trust. It will take immense effort to reverse the negative Recognition for the organization.
Saving Is Not Saving
We were building a ceiling tile manufacturing plant in Russia. Like most projects, the engineering team was directed to save money, as long as it didn’t negatively impact safety or productivity. As most were unfamiliar with doing business in Russia, they used their experience with known vendors to acquire equipment for the plant. If there wasn’t enough capacity to fill equipment needs, the project team worked with local consultants to identify the “best” options for equipment purchases.
We were building a ceiling tile manufacturing plant in Russia. Like most projects, the engineering team was directed to save money, as long as it didn’t negatively impact safety or productivity. As most were unfamiliar with doing business in Russia, they used their experience with known vendors to acquire equipment for the plant. If there wasn’t enough capacity to fill equipment needs, the project team worked with local consultants to identify the “best” options for equipment purchases.
A few years earlier we had shuttered a plant in Alabama. Equipment was stored in the hopes it might be used for future projects. The project team identified equipment they thought they could use and had it shipped to a contractor, who was responsible to inspect it and bring it up to optimal operating condition. This was done to save more than $1 million for the project.
Two weeks before plant start-up, I traveled to Russia to assess and optimize the flow of ceiling tiles through the new production line. I had done this work many times in other manufacturing plants and was known as the flow “expert”.
When I arrived, I was assigned a team of two mechanics and one production operator. We were going to send ceiling tiles through various parts of the line and make adjustments and corrections where necessary to improve the flow.
Very few tools were available for our use. I packed string, levels, and flat steel bars to help us with the work. Our initial assessment and work through the line went smoothly. We identified conveyers that were out of level, causing the ceiling tiles to skew and jam. Fixing these problems was simple enough. Soon we had tiles flowing smoothly through the first half of the line. Until we reached the equalizer.
The equalizer is a large panel saw. Its purpose is to cut ceiling boards into finished ceiling tiles. The board goes through a first set of saws, strikes a transfer, and then is driven through a second set of saws positioned at a right angle.
Boards were going through the saws at an angle. Instead of tiles looking like rectangles, they looked like trapezoids. They weren’t going to fit into ceiling grid that way.
There were many possible reasons for the angled cuts. After resolving many issues, the tiles still weren’t correct. What was going on? Normally, fixes happen independently of the saw assemblies. Saws are typically located in a level and square way on a frame. Everything else controls how the boards come to the saws in a square or angled fashion.
In this case, the problem was in the saw assembly. We locked out and climbed up on the equipment to take a closer look. The equalizer was freshly painted and made to look as if it was new. But it was far from new. There were many missing or broken parts. Because of that, we couldn’t control the boards as they were being cut. Broken motor mounts caused the saw blades to rotate in an elliptical fashion. How did the contractor miss this critical detail? How did we miss this during equipment inspection?
We spent the rest of our time repairing or replacing broken parts. Some things couldn’t be fixed immediately. We ordered parts and equipment from other locations. Some had to be air-freighted from the United States at considerable cost. All fixes were completed prior to the official plant start-up, but took valuable resources away from other critical work. All of this could have been avoided had the project team recognized the critical influence of the equalizer and chosen to invest in the right tools for the new plant. Expected savings disappeared due to the lack of All Tools Available.
Status Indicators
During a Kaizen event, teams identify projects to work on and then go off and do the work, hoping to return with a finished product. In my early experience, I allowed team members to work on their own. I hoped they would complete their work in a reasonable amount of time. It didn’t always turn out that way. Hope is not a plan.
During a Kaizen event, teams identify projects to work on and then go off and do the work, hoping to return with a finished product. In my early experience, I allowed team members to work on their own. I hoped they would complete their work in a reasonable amount of time. It didn’t always turn out that way. Hope is not a plan.
They rarely completed their work on time. More often, they lost time and progress because they got stuck and no one knew about it. I started to rotate through groups to assess progress. That relied on one person: me. After a time, I realized there was a better way to track progress, make it visible, and create engagement. The answer: Status Indicators.
Here’s how Status Indicators work:
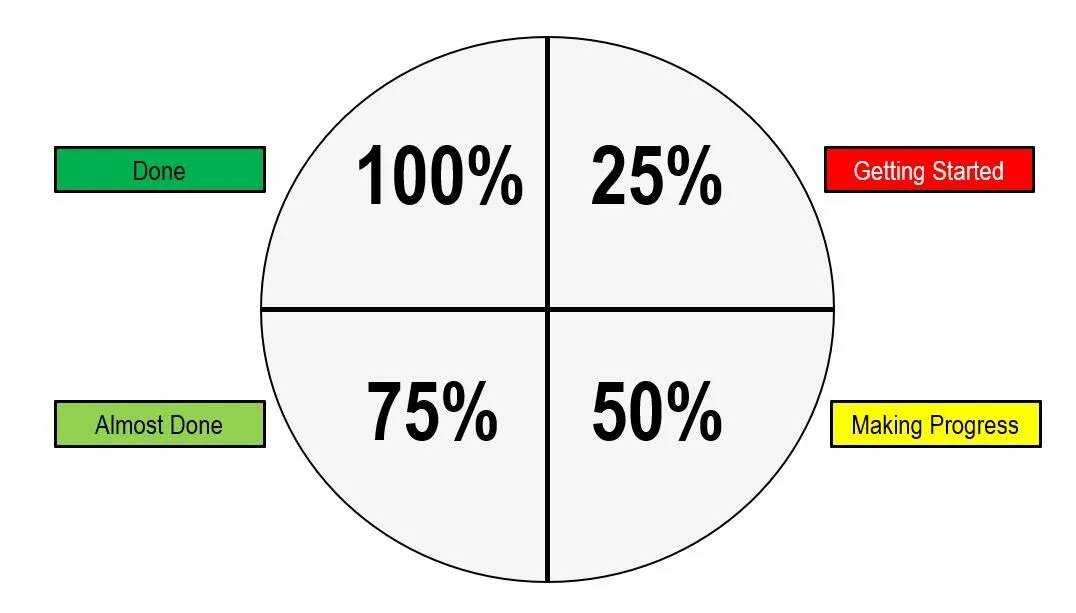
Draw a circle. Break it into quadrants. Fill in each quadrant using a marker, indicating progress towards completion. It doesn’t have to be scientific or pretty, it just has to work.
25% = Getting started – initial progress has been made or a plan has been created.
50% = Making progress – things are moving along and people know what to do and how to do it.
75% = Almost there – we can see the light at the end of the tunnel. We can finish the work.
100% = Done – we’re finished and ready to move on to something else.
There’s no need to break status down into smaller elements. That would cause the team to spend more time updating status and less time doing work. When properly updated, it’s powerful and simple to understand. I use flip chart paper to draw Status Indicators during Kaizen events. Flip chart paper is large enough to allow others to see the status from twenty feet away or more.
To give you a sense of the value and impact of Status Indicators, use the following example. Four teams are working on separate projects.
Project 1 is Almost there, Project 2 is Done, Project 3 is Getting started, Project 4 is Making progress, and Project 5 hasn’t been started. It’s clear who needs help and who can help. Team members from Project 2 can help Projects 3 and 4, depending on their skills and interests. If there are more resources than Projects 3 and 4 need, those resources can start on Project 5. Anyone else, even if they’re not on the team, can assess the status and help those who need it.
The value of Status Indicators has been reinforced to me many times, never more than when I forgot to use them. After a particularly busy day during a Kaizen event, some team members said they were frustrated because they didn’t know what to do next. Others said the day felt chaotic and disorganized. I realized I hadn’t trained the team to use Status Indicators. I immediately showed them how to use them. The next day, much more work got completed. At the end of the day, the team related how much easier it was to manage their work.
From a supervisor’s or manager’s point of view, Status Indicators make it simpler and more efficient to keep track of work going on in many areas. Hours of effort to track progress are reduced to minutes or seconds.
We Won the Battle but Lost the War
During my corporate career, we identified a critical gap in our safety training system. There wasn’t a good way to ensure traveling engineers, scientists, and technicians were compliant for annual safety training requirements. We had to get everyone immediately compliant and then develop a system for annual recertification.
During my corporate career, we identified a critical gap in our safety training system. There wasn’t a good way to ensure traveling engineers, scientists, and technicians were compliant for annual safety training requirements. We had to get everyone immediately compliant and then develop a system for annual recertification.
Working with a small team and under the direction of the Global Technical Services Vice President, we established “Technical Services Safety Days”. No one was allowed to travel during the week of training.
We developed interactive safety training activities that included everyone in the group. This would allow us to achieve compliance and provide useful skills for work and at home. We added some fun activities and games to encourage team building and networking. When training wasn’t occurring, employees were encouraged to catch up on paperwork and reconnect with others at the corporate center.
Technical Services Safety Days was a success. One hundred and fifty employees learned and practiced firefighting, equipment lock-out, chemical hazard identification, and many other critical safety topics. Tell, Show, and Do was used extensively. People appreciated the personal touches throughout the experience. My team won an award for putting together this meaningful activity and restoring safety compliance in short order.
For the next three years, Technical Services Safety Days was an annual event. People looked forward to it. Everyone blocked out their calendars for the week. For some, it was their only time in the office and they took advantage of the opportunity to network with their co-workers. They honed their skills through the creative training of best safety practices.
Then, everything changed. The company purchased a computer-based system to deliver required safety training. Employees could review the training on their own time and at their own pace during the year.
Except, it really didn’t work that way. Most waited until the end of the year and then crammed the training in to get it done. There was little engagement or knowledge retention. It seemed like a good idea and a better use of resources, but in the end, we lost the immeasurable value of having interactive Technical Services Safety Days.
Lean in Action
I was Lean Champion for the Global Technology group at a ceiling tile manufacturer for six years. During that time, I was responsible to train all new employees in Lean principles and techniques as they joined our group. The goal of this training was to help them understand what we were doing and how we applied Lean to our work. My aim was to generate interest and engagement around Lean. In the early years, things didn’t always go the way I expected.
I was Lean Champion for the Global Technology group at a ceiling tile manufacturer for six years. During that time, I was responsible to train all new employees in Lean principles and techniques as they joined our group. The goal of this training was to help them understand what we were doing and how we applied Lean to our work. My aim was to generate interest and engagement around Lean. In the early years, things didn’t always go the way I expected.
When I first started training new employees, I created eighty PowerPoint slides that described as many Lean concepts as I could squeeze into the two hours allotted for the training. I reviewed the slides, gave participants a chance to ask questions, and then declared them “trained.” I never got many questions during this training and new employee participation in Lean efforts was hit or miss once the training was completed.
I knew I had to do better if I was going to realize my engagement and participation goals. The first thing I did was develop activities to demonstrate the various Lean concepts I was trying to reinforce. From an interactive 5S number search to a triangle peg jumping game, new employees started to draw value from the time they spent with me. I saw a slight increase in engagement and participation. I wasn’t satisfied. What else could I do, I wondered?
My breakthrough came one day when one of the trainees asked, “This is all well and good, but how does it apply to what we do in Global Technology?” I knew what I had to do. Make the training specific to the actual work we did and give demonstrations of Lean in action.
The first thing I did was test my training against the Global Technology Vision and Mission. If parts of the training didn’t support our Vision and Mission, I either removed it or modified it. Now the theoretical became practical. Power Point slides were reduced and made more relevant.
Focusing on the suggestion of Lean in action, I added a Gemba walk to the training. After an hour of classroom training, I led an interactive tour of areas that had applied Lean thinking to their processes. From the Pilot Plant to the Capital Engineering Records Room to the New Product Development Project Board, new employees could observe and interact with people using Lean. They had a more definitive picture of how Lean worked in practical settings.
The training still took two hours, but was much more interactive and engaging. Because I took a different tour route each time, I was more energized by it as well. Most importantly, participation and engagement of the new employees rose to record levels.
Four Value Streams = Four Boards
I reported to the Vice President of Global Technology for a ceiling tile company as Lean Champion. During my tenure, we kicked off our Lean transformation and established four Value Streams: Innovation (R&D), New Product Development, Capital Engineering, and Business and Operations Support. Each Value Stream Director guided efforts to deliver value to the internal and external customers who relied on their critical results.
I reported to the Vice President of Global Technology for a ceiling tile company as Lean Champion. During my tenure, we kicked off our Lean transformation and established four Value Streams: Innovation (R&D), New Product Development, Capital Engineering, and Business and Operations Support. Each Value Stream Director guided efforts to deliver value to the internal and external customers who relied on their critical results.
While the Value Streams had different customers and missions to accomplish, they interacted frequently and shared resources. I supported all Value Streams and had the opportunity to build relationships across all areas of the business. One area we worked on was how to keep critical information in front of us and engage in it at all times.
In the early days of our Lean transformation, we identified the need to create white boards to display the most relevant and urgent information for everyone to see and act on. Using weekly huddles, the boards would be reviewed and decisions were made and documented. Some of the teams took this need for a white board to be a requirement and put together their boards and huddles just because they thought the Global Technology VP and Lean Champion said it must be done.
It quickly became apparent these boards weren’t helping the teams accomplish their work in a manner more productive or safer than they had been before the boards were established. In fact, one of the teams got a bit rebellious and started to make their huddle a grind, rather than a value-adding exercise. Snide remarks and rushing through information replaced deep discussion and problem-solving.
I called a meeting with the Global Technology VP and the four Value Stream Directors. After much discussion, I was able to draw out their resistance to the boards and huddles. Probing further, we identified the issue. They thought the design of the boards was prescriptive, leaving them no room to design for the purpose of their individual Value Streams. Directors thought everything had to look the same and act the same, even if it didn’t work.
Now that we had revealed the problem, we were ready to improve the situation. We quickly agreed that design of the boards and huddles should be left to the Value Stream teams. They’d decide what was most relevant and useful and then design the boards and huddles to highlight only that.
I offered my assistance in helping the teams design their new boards and huddles. Two Value Stream teams took up my offer. Two others decided to do it on their own. We agreed to these design principles:
1. Design the boards and huddles with the tools and information that help your team make decisions in the best possible way.
2. Don’t worry what your board looks like. If it helps you, that’s all that matters.
3. Make it easy to know when help is needed.
4. There’s no standard board layout. We’ll teach our leaders how to read the boards and support your efforts.
Within four weeks, all Value Stream teams redesigned their boards and huddles and started to use them. None of them looked alike. Over the next months and years, Value Stream teams redesigned their boards and huddles many times, based on what they believed was an improvement. The information they shared became more relevant, urgent, and beneficial to their employees, the overall Global Technology group, and their customers.
From time to time, other organizations benchmarked Global Technology due to our impressive results. Most people who visited with us asked why our boards looked different by Value Stream. They thought all boards should be standardized, allowing anyone to read and understand any of the boards without training.
The Value Stream teams came first, I told them. The teams did what was right for the business. We successfully taught our leaders how to read the boards and support the teams. Those who challenged my thinking didn’t always like my answer about standardization. I knew we were giving our employees all the tools they needed to make the best possible decisions for themselves, their customers, and the business.
From Tool Boxes to Tool Stations
In 2011, I was asked to facilitate a changeover reduction Kaizen event at a ceiling tile plant in Florida. Most changeover reduction events have a goal of reducing time by 50%, while maintaining or improving quality and safety. In this case, the team was asked to reduce changeover time by 90%. This would be a challenge for the team and my ability to facilitate them to a solution.
In 2011, I was asked to facilitate a changeover reduction Kaizen event at a ceiling tile plant in Florida. Most changeover reduction events have a goal of reducing time by 50%, while maintaining or improving quality and safety. In this case, the team was asked to reduce changeover time by 90%. This would be a challenge for the team and my ability to facilitate them to a solution.
The area chosen was the edge finishing line. The line cut and painted edges on the ceiling tiles before sending them on to the packaging line. Using a panel saw called an equalizer, tiles were cut to a rough size. Four tenoners cut and painted the edges of the tiles to achieve precise outer dimensions and edge finish. The tiles were designed to fit snugly into ceiling grid. A portion of the tile hung below the surface of the grid, creating a three-dimensional visual.
The tenoners had dozens of adjustment points, requiring wrenches and other tools to meet the strict dimensional tolerances. All technicians had their own personal toolbox, which they stored far away from the line. When it was time to adjust or set up the tenoners, they gathered their personal tools and brought them over to the tenoner they were adjusting at the moment.
After training the team in Lean principles and Single Minute Exchange of Die (a changeover reduction approach) we watched a changeover conducted by the crew on shift. What we saw was a tremendous amount of movement by the technicians conducting the changeover. Most of the movement was due to each technician gathering and moving tools back and forth between the line and their personal toolboxes which were stored thirty yards from the tenoners.
The changeover took ninety minutes. Our goal was to achieve a consistent nine-minute changeover. I wasn’t sure it was possible, but there appeared to be a tremendous amount of opportunity, especially in the area of tool use and placement.
After brainstorming overall improvement ideas, I facilitated the team to focus on ways to eliminate the huge amount of movement we observed. The plant was built in the 1940’s. Most technician habits developed over many decades of production. I wasn’t sure people would be willing to change their approach and give up their personal toolboxes.
They weren’t willing to, but it didn’t matter. The team realized their toolboxes should be set up to do unscheduled repairs and adjustments. Placing tools right at the place they were needed, would save a huge amount of time during changeover.
We identified three tools used to set the tenoner saws and edge paint sprayers precisely. They were needed in eight separate locations. Were we willing to replicate those three tools eight times?
If we wanted to cut the time by ninety percent, we had to be willing to try extreme measures. I went to the hardware store and bought eight sets of tools. The team mounted them exactly where they were needed for the changeover.
In addition to the tools, we created visuals to show the steps and installed a large digital clock on a post. It displayed the changeover elapsed time. We tested our new procedure with all of the improvements and were able to complete the changeover in fifteen minutes by the end of the Kaizen event.
Although we didn’t meet our goal, changeover time was reduced by 83%. The team felt like they had won and the plant reaped the benefits of a safer and quicker changeover for many years thereafter.
This Stuff Works
At a gummy vitamin manufacturer in Pennsylvania, I was asked to facilitate a team of mechanics responsible for supporting and maintaining the manufacturing operation. They had difficulty keeping their maintenance area compliant with strict food production regulations. Our goal was to develop a system to guarantee compliance, while improving their ability to service their customers.
At a gummy vitamin manufacturer in Pennsylvania, I was asked to facilitate a team of mechanics responsible for supporting and maintaining the manufacturing operation. They had difficulty keeping their maintenance area compliant with strict food production regulations. Our goal was to develop a system to guarantee compliance, while improving their ability to service their customers.
On the morning of the first day of the Kaizen event, I taught Lean principles and how 5S is used to optimize safety and productivity in a space. It all sounds good in a classroom. The team wondered how it applied to their situation. After training, we took a Gemba walk through their workspace. They thought they were in pretty good shape. The space was cluttered and lacked any hint of organization. They had nothing to compare to and hadn’t been exposed to other examples of 5S in the facility. After generating ideas in their work area, I took them to two locations in the plant that had used 5S: a production line and the Weld shop.
Our first stop was the production line. I asked one of the technicians operating the line to give the team a tour and point out what they had done and the benefits he had seen. He obliged and described 5S and its benefits as best he could. Team members were paying attention to what he was saying, but asked few questions and wrote fewer notes. I thanked the technician and took the team to the Weld shop.
On our way to the Weld shop, I asked team members what they thought of the production line. Feedback fell into two categories:
1. It looks pretty good.
2. I can’t see how it applies to our area.
I knew the next tour stop would be more inspiring. I was intimately familiar with what was done in the area. I could provide a more compelling review for the team.
When we got to the Weld shop, I noticed Jimmy working on a project. He was the team leader when we applied 5S to the Weld shop.
Jimmy: “What are you doing here?”
Me: “This is the Kaizen team from the gummy vitamin maintenance area. I’m giving them a tour of the Weld shop and showing them what your team accomplished.”
Jimmy: “Okay, just don’t get in the way. I’ve got lots of work to do.”
Me: “Thanks Jimmy. If you want to give the tour or share your thoughts, please do.”
Jimmy: “That’s fine. You can give the tour.”
Jimmy is not someone who likes to speak in front of groups or work with teams. Jimmy is also one of those folks who isn’t a fan of management or consultants. But, if he believes in something, it’s useful and helpful to him and others. He doesn’t give out compliments often (ever?) and doesn’t fall in line and do whatever he’s told.
I started the tour pointing out various ideas and improvements the Weld shop Kaizen team made six months earlier. Jimmy was paying attention to what we were doing, but didn’t say a word. I think he was interested to see how I’d describe the work of the Weld shop team. I did my best to represent their efforts and as I did, you could see the pride grow in Jimmy’s face.
My next stop on the tour was at the tool board created by the team during the Kaizen event. As I started describing and demonstrating the use of the tool board to the team, Jimmy got more and more interested. My new team was asking many questions and taking notes on my responses and their observations.
Rob (team leader): “This looks good and all. Does it really stay this way?”
Me: “I don’t think they cleaned up for us.”
Ben (team member): “Does this really work?”
Jimmy: “Look, this may sound silly and it may sound stupid. This $#*% works!”
This was the moment of clarity and credibility for the team. If Jimmy thought so, it must be so. I stopped the tour. The team had seen everything they needed.
I thanked Jimmy and took the team back to the meeting room to review their observations and ideas. On the way back, I challenged them to beat the results of the production line and the Weld shop. They told me they were up for the challenge.
The rest of the week, the team did amazing work, identifying the critical tools needed (All Tools Available), giving them the most visible and logical homes (Visible Evidence) and even telling the leadership team what they needed them to do to sustain the efforts from now on (Layered Audits and Accountability). I am not sure their area was any nicer or better thought out than the Weld shop or the production line, but they thought so, and that’s all that matters.
You’re Never as Good as You Think You Are
Of all the Kaizen events I have facilitated, there is nothing like 3P. It’s the most exciting, energizing, and exhausting way to create breakthroughs with a team. 3P stands for Production Preparation Process. The idea is to design a new product or process with the least amount of waste possible.
Of all the Kaizen events I have facilitated, there is nothing like 3P. It’s the most exciting, energizing, and exhausting way to create breakthroughs with a team. 3P stands for Production Preparation Process. The idea is to design a new product or process with the least amount of waste possible.
Production Preparation Process uses an eleven-step method to open people’s minds to what’s possible and make them as creative as their 8-year old selves. The technique was invented by Chihiro Nakao, a legend in the Lean community.
I was first exposed to 3P by consultants in 2010. We used the technique to design a new product in half the time it would have taken us to using our standard product development methods. I had the opportunity to facilitate half a dozen 3P events and was able to achieve similar breakthroughs with other teams.
I was always curious about the thinking behind 3P and had the opportunity to participate in a 3P competition, run by Sensei Nakao’s company, Shingijutsu, in 2013. During the week, I was able to pick up the nuances and deeper thinking behind 3P. I realized I had been taking shortcuts during the events I facilitated and because of that, we were diminishing our breakthroughs and results. I didn’t get to meet Sensei Nakao at the competition, but gained a deeper respect for the man and his thinking. I decided I would have to meet him one day, if the opportunity arose.
Meeting the Sensei
In 2016, I found out there was an opportunity to meet Sensei Nakao, as Shingijutsu was running another 3P workshop at a plant in Connecticut. He was the overall sensei for the week. I convinced three other coworkers to register for the workshop and we drove up to Connecticut together. During the drive, we discussed our expectations for the session. I wanted to learn from the master, but I also decided I had to have the ultimate tourist experience: be scolded in Japanese by Sensei Nakao.
The host plant made parts for the aircraft industry. More than sixty people signed up for the workshop. We were divided into eight teams, each having a part of the process to improve using 3P. After some initial training in Japanese (with English translation) by Sensei Nakao, teams were assigned a sensei (facilitator) and toured their area of responsibility.
I had met my sensei at the 2013 competition. He chose me to be on his team for that reason. He also knew I had some experience in 3P and its facilitation, so he gave me more responsibility than the rest of the team.
We took a tour of the operation and spent many hours on the factory floor, engaging with the technicians and gaining deeper understanding of the process. By the end of a very long first day, I was exhausted and glad when the team dinner was over. I knew I would need a good amount of sleep to prepare me for the next day’s activities. I felt confident, having much experience with 3P. What could they throw at me that I hadn’t seen before, I wondered?
Go to Gemba
The next day, after a quick review, the team went back out to the factory floor to gather more data and test ideas. I was asking an operator some questions when our sensei motioned to me. He asked me to join him away from the line. He was working with another team member and wanted me to help facilitate the next step of the eleven-step method. They were drawing some pictures on a large piece of paper taped to a wall, just fifteen feet from the production line.
As I was helping my teammate at the wall, I felt a tap on my shoulder. I looked up and it was Sensei Nakao. He didn’t look happy. I got my wish. I was being scolded in Japanese! I only understood one word: Gemba. The interpreter told me that I should be spending more time in Gemba and not away from it at a wall. All learning was to be done in Gemba. There was nothing I could say, but I could see my sensei looked uneasy.
Achieving My Goal
My sensei must have said something to Sensei Nakao, as he was taken aside and spoken to in Japanese. He looked like a beaten puppy. When Sensei Nakao finished with him, he left and went to visit with the next team. I waited a few minutes and then said to my sensei, “You got scolded, didn’t you?” He looked at me sheepishly and finally admitted he had. We both laughed. I had realized my tourist objective.
The rest of the week was a blur. We were able to solve the problem we had been assigned. I learned deeper meanings of 3P and was able to bring back refined skills to my company. I continue to learn more about 3P. No matter how many 3P experiences I have, I can always do better. Sensei Nakao’s scolding reaffirmed it.
It’s Better to Beg Forgiveness than Ask Permission
In 1998, I was invited to Hoogezand, the Netherlands, to help a team make improvements to their ceiling tile production line. Little did I know it would be the longest Kaizen event in my life. I had been to the plant three months before and identified significant changeover time reduction potential. It was time to put my money where my mouth was. In advance of the trip, we identified members of the team and the need for an interpreter. I didn’t speak Dutch and still don’t. We’d have two weeks to work on the line and were to coordinate with the Production Manager any time we needed to shut the line down to work on or test the equipment.
In 1998, I was invited to Hoogezand, the Netherlands, to help a team make improvements to their ceiling tile production line. Little did I know it would be the longest Kaizen event in my life. I had been to the plant three months before and identified significant changeover time reduction potential. It was time to put my money where my mouth was. In advance of the trip, we identified members of the team and the need for an interpreter. I didn’t speak Dutch and still don’t. We’d have two weeks to work on the line and were to coordinate with the Production Manager any time we needed to shut the line down to work on or test the equipment.
I arrived in the Netherlands on Sunday and met with the team in a conference room on Monday morning. After introducing myself, getting to know each of the team members, and providing some Lean and changeover reduction training, we took a tour of the line to identify the highest priority areas to improve and also to get a sense for the team’s interests.
The line wasn’t running very well and I was informed this was typical. Most of the equipment was in need of repair and the maintenance department wasn’t in tune with the needs of the production organization. I told the team I wanted to meet the Maintenance Manager. They looked at me like I had asked for something outrageous. When he came out to the line, I could see why they were a bit apprehensive.
Progress vs. Paperwork
Ullrich was a very tall German man, perhaps six foot eight (I am five foot seven on a good day). With a shaved head, hands twice the size of mine, and a very low and stern voice, he introduced himself by grabbing my hand and saying, “You vill not touch or modify any equipment without filling out the proper paperwork!” Taking my hand back before it was crushed, I assured him we would follow the rules. Although he didn’t seem satisfied, he left to go to the maintenance office.
Realizing we couldn’t fill out paperwork while we were making our improvements, I promised the team I would fill out the forms at the end of each day. The team didn’t look like they believed me, but knew I didn’t want any broken fingers. There were so many problems on the line. Two weeks weren’t enough time to fix everything. With focus, dedication, and proper prioritization, I was sure we’d make significant progress.
The top priority of the team was to improve the reliability of the equalizer, which cut the ceiling boards into finished tile dimensions. Operators had a difficult time setting up the proper cutting sizes. It took hours for them to get the proper cuts. We asked the Lead Operator to shut down the line, to allow us to assess the situation and find out why it was so difficult to set up to the proper size.
Five minutes later, the Production Manager came by to find out why the line was shut down. We told him we were trying to figure out what was keeping the equalizer from being set up consistently. He reminded us we were supposed to let him know any time we were going to shut down the line. I apologized and said it wouldn’t happen again. Knowing it probably would happen again; I advised the team to remind me to let the Production Manager know our intentions before shutting the line down. They promised they would. I wasn’t so sure.
Asking the Right Questions
The equalizer used precision screws to guide the saws to their final positions on the cutting bed. Operators turned a handle to move the saws on the screws. Watching the saws move as the handle was turned, I could see the saws weren’t moving consistently. With the first full turn of the handle, it appeared the saw moved twice as far as it did with the second full turn of the handle. This situation had to be resolved. First, we had to figure out why things were acting in this way.
We tracked down a dial indicator with a magnetic base. We wanted to see how much variation was occurring when we tried to move the saws. On our first test, the handle was turned one full revolution and the saw traveled 0.020”. We turned it one full turn in the opposite direction and the traveled just 0.005”.
The team was convinced the precision screw had worn down, causing variation in movement. Thinking about this, I knew this should not be the case, but I also know what my eye had seen. Then I asked the question, “What is riding on the precision screw?” It turns out it was a brass bushing. My next question was, “Which component is more likely to wear down, the brass bushing or the hardened steel precision screw?” It had to be the brass bushing. My next question was, “When was the last time the brass bushings were replaced?” No one remembered it ever happening.
We tracked down Ullrich, explained the situation and found enough brass bushings to replace all of the assemblies on the equalizer. Four hours later, we had replaced bushings worn down to the nub with brand new brass bushings. After, we tested out changes and now had saws able to repeat their locations within 0.001”. Ullrich reminded me to fill out the proper paperwork, but was impressed enough to shake my hand. This time, he didn’t crush it.
Making Progress and Earning Trust
Over the rest of the first week, we made similar improvements to all areas of the line. We never filled out the paperwork in advance, but our earlier success at the equalizer reduced the pressure on me, the team, and my hands. We also made a game of shutting down the line and then betting on how long it would take the Production Manager to show up to see what we were doing. We were improving so many things so quickly he also gave us the leeway to shut the line down without approvals, but kept playfully reminding us to follow the rules.
The team enjoyed the work so much they decided to work on Saturday and then take Sunday off. I took Sunday to go sightseeing and got lost in the village of Makkum, 80 miles to the west, known for their ceramic tile craftsmen. That’s a story for another time.
Monday, the team was ready to make more improvements to the line. We improved almost every part of the production line by Friday morning. Our report out was scheduled for Friday afternoon. The entire plant staff showed up at the production line and listened to the team explain and show their improvements in Dutch. At the end of the report out the team said, “Adam leerde ons dat het beter is om vergeving te smeken dan om toestemming te vragen!” After much laughter and clapping by the staff, Ullrich, and Production Manager, I was told the translation was: “Adam taught us that it is better to beg forgiveness than ask permission!”