
Kaizen Success Stories
Real Manufacturing Results. One Kaizen at a Time
Explore real-world Kaizen success stories showing how manufacturing teams solved critical problems, improved performance, and created sustainable results.
With Persistence and Desire, Anything is Possible
I started working for Thomasville Furniture out of college as an Industrial Engineer. Born and raised in Maryland and working in North Carolina, I was called “Yankee,” and I had to prove myself worthy every day. I felt like I was up for the challenge. My mother reminded me I was born south of the Mason Dixon line, but it didn’t seem to matter to North Carolina natives.
I started working for Thomasville Furniture out of college as an Industrial Engineer. Born and raised in Maryland and working in North Carolina, I was called “Yankee,” and I had to prove myself worthy every day. I felt like I was up for the challenge. My mother reminded me I was born south of the Mason Dixon line, but it didn’t seem to matter to North Carolina natives.
My first assignment was in Thomasville’s veneer plant. At this plant, many types of veneers were brought together to make beautiful panels used in expensive furniture, more expensive than I could afford. I was fascinated by the labor-intensive process of veneer making, and spent many hours in the plant observing what was going on and asking lots of questions of the workers. They seemed amused by the Yankee who was willing to listen to them.
An Expensive and Inefficient Process
One afternoon, I was in the basement of the plant and watched workers put materials into and out of a hot press. This press was a large, multi-opening machine used to cure and remove moisture from some of the most expensive veneers bought by Thomasville. The machine looked like a large pizza-oven, and had eight openings, one above the other.
I watched a crew of six workers place a large metal plate on a table. After that, they took a “book” of burl veneer – 14 slices from the same log that look generally the same, and spread out each slice on the metal plate. Then, they put another metal plate on top of all of the slices, creating a metal and veneer sandwich. This sandwich fit into an opening of the press. When all eight press openings were filled, a button was pushed, and the press closed on all of the sandwiches. 36 hours later, the sandwiches were removed, all extremely hot, by the same six workers. Now, the workers had to remove the metal plates without burning themselves or damaging the veneer. Heat and pressure had created a vacuum inside the veneer sandwiches, so when the plates were removed, the veneer would fly around and break, as it had become drier and more brittle.
This was the most expensive material used in the furniture and the plant was losing much of it in the course of the curing process. It really bothered me, so one afternoon I decided to talk with the plant manager to see if there was something that could be done.
Avis Tobin worked for Thomasville for many years. He was short, very round, kept a cigar in his mouth at all times, and had the type of loud, gravelly voice that would frighten small children away. I asked him if the “books” of burl veneer could be cured without separating them into single pieces. He responded, “Son, you just don’t know anything about the veneer business. It can’t be done. The veneer would stick together and we’d lose everything.” I wasn’t satisfied with his answer, but it was the most he had ever said to me during my time in the plant.
Opportunity for Change
Six months later, Avis retired and was replaced by a younger plant manager named Bob Ashley. Bob and I developed a strong working relationship over the next few months, as I was able to complete many projects he requested of me. One day, while sitting in his office, I brought up my idea of curing the burl veneer in stacks, rather than pieces. I thought there might be a better way to do it. Bob thought a minute or two, looked intrigued, and placed a call to the veneer buyer at the plant. “Do you have any contacts who cure veneer in the general area?” he asked. The buyer had one in Beaufort North Carolina, which was about four hours from the plant in Thomasville, on the East coast of the state.
Two weeks later, four of us, the plant manager, veneer buyer, truck driver, and me took a truck load of burl veneer to Beaufort to see if we could cure it without de-stacking it. When we arrived at the plant, we saw a piece of equipment we had never seen before: a combination hot press and cold press. The Beaufort plant cured straight grain veneer in this combination press with two people, one loading a conveyer in front of the hot press, the other unloading a conveyer at the back end of the cold press. The stacks of grain veneer would be conveyed into the hot press, pressed for a few minutes, conveyed out of the hot press to the cold press, pressed for a few more minutes, and then conveyed out of the press to the operator.
The stacks of straight grain veneer came out of the end fully cured, with no pieces sticking to each other. Would our burl veneer do the same? We were invited to put a few stacks of burl veneer into the combination press and try it out. We did, and when the stacks came out the other end, most of the pieces of veneer were stuck to each other. We were disappointed. The operations manager for the plant said, “Oh, I forgot to change the heat and dwell time for the burl veneer. It has more moisture in it, so I need to adjust the settings for that.” After he made the change, we tried a few more stacks of burl. Lo and behold, most of the veneer was cured and hadn’t stuck to any other pieces. Approximately 20 percent was still stuck.
A Valuable Lesson
We decided that was all we needed to see. We felt like we would be able to identify the settings required to eliminate the sticking completely. We drove the four hours back to Thomasville with grand plans to change the way we would cure veneer forever. I wrote an appropriation request for approximately $250,000 and bought Thomasville’s first combination cold and hot press. Six months later, it was fully operational. Manned by two operators, we found the proper settings cured burl veneer in one tenth the time of the prior process, with much less scrap and zero risk of being burned. After that, I realized the only limitation to solving difficult problems was preconceived notions of what was possible. If you are willing to take a risk, you may get a breakthrough. I still use this thinking today, as I help Kaizen teams of all sizes and structures worldwide.
Overcoming Resistance to Change
Process Improvement Partners was brought in to help a consumer goods manufacturer cut their changeover time (the time it takes to switch tooling and equipment over from one product to another) in half. By doing so, they would be able to reduce inventory and improve process performance.
Process Improvement Partners was brought in to help a consumer goods manufacturer cut their changeover time (the time it takes to switch tooling and equipment over from one product to another) in half. By doing so, they would be able to reduce inventory and improve process performance.
The company has five different shifts operating 24 hours a day, 7 days a week. Each crew believed it had the best approach to changeovers, but the results didn’t show it. There was major variation between and within shifts and none of the crews were able to start up their lines consistently and effectively coming out of a changeover.
The Path to Improvement
Process Improvement Partners recommended a 4 ½ day changeover reduction event, or SMED (Single Minute Exchange of Die) Kaizen, using representation from each of the crews. By doing this, we could identify best practices across all of the crews and teach changeover reduction techniques to be shared once the Kaizen was over. The leadership team agreed, and we began preparations for this critical event.
Our leader, the Operations Manager for the production line, picked a team of “All Stars” to participate in the Kaizen. He felt their experience, creativity, and enthusiasm would lead us to a win.
This was the first changeover reduction Kaizen in the history of the plant, and the team was skeptical when we stated our objective: cut the existing changeover time in half, without increasing safety risk to the crew or quality risk to their customers. The team members assumed this meant they would have to rush around, with intense pressure to meet the new target time. The truth was using SMED techniques, we would be able to reduce enough waste in the existing changeover process to take significant time out and reduce safety and quality risk. Then, using the Wheel of Sustainability, we would be able to continue to get great results for years to come.
Turning Skepticism into Excitement
The first day of the Kaizen, we taught the four step SMED methodology (with a little spin from Process Improvement Partners):
1. Assess the current changeover and identify steps that must be done while the line is shut down (internal steps) and steps that are done while the line is still running (external steps)
2. Convert any internal steps to external steps
3. Streamline any remaining internal steps and then any external steps
4. Eliminate any adjustments and put in all aspects of the Wheel of Sustainability
For step one, we videotaped the changeover, did some motion analysis, and made numerous observations of waste. The team was excited to see opportunity they hadn’t realized existed. They never had stepped back and watched what was happening, as they always had to participate in the changeovers.
As we entered step two, the team prioritized the steps they thought could be converted from internal to external. Their creativity helped them invent and build a number of jigs and fixtures that allowed work to be done in preparation for the changeover, while the line was still running. By the morning of the third day, the team tested their efforts and found the time required to change the line over had already been reduced by 50%. They weren’t satisfied, there was much more they felt they could do.
For the rest of the third day and part of the fourth day, the team worked on improvements to streamline remaining internal steps, found ways to eliminate adjustments, and created visuals to help all team members do the changeover the same way every time. Now it was time to give the changes the ultimate test: let another crew try the new changeover procedure.
Working Through Opposition
Each team member was assigned a crew member who wasn’t on the team. They were assigned to review and teach them the new method and answer any questions or concerns. They were sent out onto the factory floor and had approximately 1 ½ hours to teach and discuss the new methods and approach one on one. After a while, one of the team members came into the meeting room and asked for my help. Her assigned crew member was not interested in participating in the test of our new changeover procedure. I came out on the floor to find out if I could help the situation.
The crew member, let’s call him Roy, was visibly upset, so I asked him what was bothering him. He started yelling at me, saying we hadn’t listened to him or anyone else on his crew, didn’t videotape their changeover, and generally didn’t care what they thought. I told him the team had representation from every crew and had done their best to use the best practices from each shift as we worked during the week. He was having none of it. I let him know that we needed to let someone other than the team try out the new method, so we could get feedback and make improvements to it, before locking in all of our changes. His anger grew. I knew I needed to do something extreme, or he would be lost and we wouldn’t learn what was needed to finalize our new procedure.
I asked, “Are you telling me you’re unwilling to try the new procedure?” Roy realized he was being asked if he was being insubordinate, which is a disciplined offense in most companies. He answered he was willing to try the new procedure, but just wanted to voice his protest about the lack on inclusion. I told him I respected his opinion and thanked him for his willingness to try the new approach.
Testing the New System
At 4:30 pm, we gathered all crew members to explain the new procedure, set the expectations for them to follow it to the letter, and would give them the opportunity to provide feedback once the changeover was complete. We would also pair a team member from the Kaizen team with each crew member, so they could be coached during the changeover, just in case they didn’t remember or understand the new steps or approach. All crew members affirmed their commitment to try the new procedure, and we started the new changeover at approximately 4:40 pm.
Three minutes into the changeover something didn’t look right. One of our Kaizen team members, let’s call her Julia, looked extremely uncomfortable. I took her a few feet away from her assigned crew member and asked her if her assigned crew member wasn’t following the new procedure. She nodded and I called the Kaizen team leader over, to talk about what was happening. He wasn’t happy and we agreed to stop the changeover immediately.
We gathered the crew back together, explained what was wrong, why it wasn’t ok to try their own procedure as we wouldn’t learn anything if they did. We then instructed them to put the line back to its original condition before the changeover. After that, we would start the changeover again. There was tension in the air.
At approximately 5:00 pm, we started the changeover for the second time. In two minutes, one of the Kaizen team members, let’s call him Jack, came over and informed me his assigned crew member wasn’t following the new procedure. We stopped the changeover again, gathered the crew, and in an impassioned way, did our best to convince them to try it the right way, or we would do this all night. Would things work out on the third try?
We started out third attempt at 5:10 pm and this time everyone followed the new procedure to the letter. You could see the tension fade away from the Kaizen team members. Now, something else was creeping in. The team had been working since 6:30 am and they were getting tired. 65 minutes later, the changeover was complete. Now it was time to bring the crew into the meeting room and get their feedback and reaction to the new procedure. I was wondering how Roy and his crew mates would respond to the new procedure and the two stoppages we imposed on them when they tried to go “rogue”.
A Surprising Conclusion
In the meeting room, I set up a flip chart and gathered all crew members around a table. I asked each of them to tell us, one at a time, what they thought, identifying out the things they liked and the things we could improve for them. As they spoke, I would write their comments on a flip chart for everyone to see.
Roy started out the feedback session by telling us he “loved” four very specific improvements the team had made. He also offered some constructive feedback on some simple things we could improve. Others had the opportunity to share their feedback, and all of them had positive and constructive things to say. I have to admit I was a bit shocked at the change in the tone in the room. I had figured the crew would save up all of their anger for the meeting room. Instead, they were appreciative for all of the Kaizen team’s efforts. They had realized our Kaizen team was doing their best for everyone in the crew, and the test proved it to them.
We thanked the crew and the Kaizen team, and sent everyone back to the line or home. There were many handshakes and high-fives before they left.
At the report out to leadership, the team remarked how important it was to get everyone’s input and also to test out new ideas with a group that wasn’t involved in the changes. It illustrated how difficult change can be, as most people tend to expect the worst and hope for the best. Since then, the line has been able to sustain the reduced changeover time and has many more believers in changeover reduction and Kaizen.
Speaking Up Takes Courage
In 2011, I was asked to assist a team in Pensacola, FL who wanted to improve processes in their distribution center. We were given four days to accomplish our task – reduce shipping damage by 50%. This was a tall order, but the team was up for the challenge.
In 2011, I was asked to assist a team in Pensacola, Florida who wanted to improve processes in their distribution center. We were given four days to accomplish our task – reduce shipping damage by 50%. This was a tall order, but the team was up for the challenge.
After a half-day of training on Lean tools and techniques, the team took a walk in the distribution center and supplying processes and identified many ideas they thought would improve the situation for everyone who worked there.
All of the ideas were shared and the team prioritized the ideas they wanted to implement first. Breaking the team into smaller sub-teams, we picked the top three projects to work on. Each sub-team developed their solutions and began to implement them. At times during the day, we would come back as a full team and review each sub-team’s progress. Things were getting done, but it wasn’t clear that any of the projects would significantly reduce shipping damage.
On the morning of the third day, I asked the team if they had any feedback or ideas to help us make better progress against our goals. The room was silent. One of the team members, let’s call her Ruth, had an uncomfortable look on her face. I didn’t want to put her on the spot, so I asked each team member, one at a time, to give one suggestion they thought would make the day better for everyone. Most people said things like, “Let’s work better as a team,” or “We should try to get more done.”
When I got to Ruth, she blurted out, “I don’t think we’re working on the right things.” This took me by surprise. I wanted to know more. She then explained we weren’t focusing on the root cause of the shipping damage. She thought we were just working on things that were easy to implement, not directly impacting the causes of shipping damage.
I felt a sense of panic – we were in the third day and would be reporting our results at the end of the fourth day. There was little time to spare, but we had to resolve this issue or else we would fail. We were a team and the members started to share their thoughts with Ruth about the problem we were trying to solve. They realized Ruth was right. We were avoiding the real issues causing shipping damage. We brainstormed again and prioritized efforts based on the right things to do, not the easiest things to do. Relief started to wash over me as I realized the team was determined not to fail.
Once we finished prioritization, the team split into four sub-teams. Each sub-team had a sense of urgency and purpose and worked on their projects with energy and a “refuse to lose” spirit. If they had a question, or got stuck, they went to find help. Nothing got in their way. Almost all team members stayed late and everyone agreed to come in two hours early the next day to ensure their work would be done.
We decided to abandon the standard Power Point presentation of our findings and changes and worked right up to the time of the report out. When the leadership team came to see what we had done, we gave a tour of the changes we implemented to reduce shipping damage. They were impressed and believed we had accomplished our goal of 50% reduction.
I learned a valuable lesson from Ruth, and it’s one I share with all of the teams I work with. Understand the problem you are trying to solve. Once understood, focus on the thing(s) that will solve the problem, no matter how difficult they may seem. If you’re veering off course, have the courage of your conviction to steer people back on course. Never be afraid to speak up.
I now give all of my teams many opportunities to speak up and share their concerns. I also do it as soon as possible in every Kaizen event I lead or facilitate. It’s better to change course than end up in the wrong destination. Thanks to Ruth for being brave enough to steer us back on course.
Even the Most Organized Person Can Improve
A global ceilings manufacturer wanted to improve the safety and productivity of its testing facility. Over the years, many capabilities had been added to the facility without regard to the needs of the technicians who worked there. Because of this and the lack of a managing system to ensure the organization and productivity of the facility, the technicians took it upon themselves to hold an annual “cleanup week” at the end of the year. All technicians would stop their project work and devote their time to go through equipment, materials, and spaces and clean out any clutter they felt they could get rid of.
A global ceilings manufacturer wanted to improve the safety and productivity of its testing facility. Over the years, many capabilities had been added to the facility without regard to the needs of the technicians who worked there. Because of this and the lack of a managing system to ensure the organization and productivity of the facility, the technicians took it upon themselves to hold an annual “cleanup week” at the end of the year. All technicians would stop their project work and devote their time to go through equipment, materials, and spaces and clean out any clutter they felt they could get rid of.
Three weeks after “cleanup week,” conditions had reverted back and it didn’t look as if any effort had been exerted. This happened annually, and the technicians were extremely frustrated. The lead technician of the testing facility wanted to do something different and sought me out for advice. After walking through the facility with him and listening to his concerns, I suggested we meet with his manager, who was responsible for the testing facility. We took a walk together and discussed the problems created by the clutter and lack of organization in the facility. After about an hour of discussion, we agreed we should use an improvement approach called 5S (Sort, Set in Order, Shine, Standardize, and Sustain) in a targeted area to see if we could make sustainable improvements that could be replicated in other areas of the facility. But, where should we start?
We decided to pick an area known for its organization and strong ownership. We also wanted to pick an area small enough to do proper 5S on in a week or less. We had just the area – the manual paint spraying area. This area was used by many of the scientists, technicians, and project team members. It had a very strong area owner, let’s call her Regina. Regina was known for her tenacity and ability to hold people accountable to follow her rules for the area. This was the area owner we needed. The area was fairly well organized and small enough to demonstrate the value of 5S in a week or less.
We approached Regina and asked her if she would be willing to lead the first 5S team in the testing facility. She agreed, but wasn’t sure what improvements we could make. She was proud of what she had been able to accomplish and had every right to be. She didn’t realize what was possible with 5S and proper sustaining systems. I gave her a quick overview of what I thought might be possible and advised her to pick the team she wanted to help her do the best job possible. Over the next few weeks, she visited with team members to encourage them to participate and share a vision of what was going to happen. She even convinced the manager of the testing facility to participate. He showed his leadership commitment to the effort and raised quite a few eyebrows in his peer group.
The first day of the Kaizen was “Sort” Day. On this day, the team goes through all of the materials, parts, and equipment and makes tough decisions about what to keep and what to remove or throw away. They removed at least 50% of what was in the area. This was shocking to Regina, as she thought he had been diligent to keep unused things out of the area. What she didn’t realize was she was being conservative in her decision making and those using the materials knew some of them would never be used again. We removed so much clutter and materials, the team was able to remove the top shelves in the area, allowing everyone to reach any materials without getting on a step stool or even reaching over their heads. We then added signage to show everyone it was unacceptable to store anything above their heads.
The second day of the Kaizen was “Set in order” Day. On this day, the team took all remaining materials, parts, and equipment and identified the best locations to place them in. After doing so, they labeled the locations, painted outlines, and generally made it impossible to put things in the wrong location. During this effort, I noticed a few of the technicians talking about repair parts for paint guns. Apparently, each one had his or her own repair parts, because they didn’t trust they would be able to find them when they were needed. I asked this question, “If we always knew where the repair parts were and they were immediately available, would you need to squirrel away repair parts?” They all agreed they wouldn’t, but didn’t trust 5S would keep parts from being lost, stolen, or just walking away. I asked them to trust me and with their help, we designed the most visible system possible for the repair parts. I agreed to let them keep their own stash of parts for a few months as a backup plan, but asked them to try the new system first and hold others accountable to do so as well. They grudgingly agreed and were extremely skeptical. Understandable, but I told them we were going to create the new system and rules for it and they could be the ones to help make it work and also enforce them, with the help and support of the leadership team. We would have to teach the leadership team the proper way to support the new system, and we would use our report out to start the process. I would also work separately to coach and teach the leadership team how they should behave.
After “Sort” and “Set in order” days, we worked on Shine, which means to clean and inspect and assure every piece of equipment, tool, and material is in the best condition possible. All of the team enjoyed the day, as they were able to repair and replace things that had been working at less than optimal levels for many years. All repairs and replacements were done on the spot and at very little cost to the company. It helped the team realize they would be empowered to keep things in top operating condition at all times.
On the last days of the Kaizen, we worked on the sustaining systems to ensure all of the team’s efforts would live on. This included responsibilities for those using the area, those maintaining the area, audits of the area, and visits to the area by leadership.
On the final day of the Kaizen, the team presented their results to a packed meeting room. There was a lot of excitement, but nothing like what happened when they gave a tour of the “new” area. People were amazed at what the team had accomplished and the quality of the sustaining systems they had built. They were even more amazed when Regina talked about the difference of having the repair parts out in the open and not squirreled away by each technician. She related a story of how she had lost over 2 hours looking for a specific repair part a technician had locked in his desk. Because she didn’t have the part in her stash, she had to track the technician down, wait for a meeting he was attending to end, and then get the key for the locked desk drawer. This was a typical story, not an exception. Now, because of the team’s efforts, she could get to any repair part in less than 10 seconds. This was an immediate improvement to safety and productivity.
When the tour was over, there was much clapping and recognition for the team. Many in the audience stayed to talk to team members about their perspective on what had happened. They relayed the same thought they had before the Kaizen, “Regina’s area is so organized. What improvement can we make?” Now they knew. In the following months and years, more the two dozen other areas in the testing facility used 5S and installed the same sustaining systems.
These simple tools helped the facility reduce their customer response time by more than 50%, doubled productivity, and greatly reduced safety risks throughout the facility. It also opened their eyes to the idea that no matter how good you think you are, you can always get better.
Top 5 Continuous Improvement Books
I have read many books on Lean, Six Sigma, and other Continuous Improvement methods over the years. Some inspired me, some frustrated me, and all made me think. The following 5 (and two honorable mentions) are my all-time favorites.
I have read many books on Lean, Six Sigma, and other Continuous Improvement methods over the years. Some inspired me, some frustrated me, and all made me think. The following 5 (and two honorable mentions) are my all-time favorites.
Number 5: The Toyota Way – Jeffrey Liker
This is an easy read and talks about the principles behind the Toyota Production System. It is the first book that I recommend to anyone who wants to know what “Lean” is.
Number 4: The Goal – Eliyahu Goldratt
All about the Theory of Constraints, this book reads like a novel. I wanted to see if they save the factory and live happily ever after. There’s a great story in it about a camping trip that really brings manufacturing issues to life. I have shared this book with others to give them insight into the world of manufacturing.
Number 3: Key Strategies for Plant Improvement – Shigeo Shingo
Written by the all-time greatest Industrial Engineer (my opinion, of course), this book provides quick ideas and ways of thinking that opened my eyes to possibilities. Many of the ideas can be implemented immediately, without any investment.
Number 2: A Revolution in Manufacturing: The SMED System – Shigeo Shingo
The first continuous improvement book I ever read. It probably influenced me more than any other. I was able to immediately implement SMED in the little factory I worked in and saw amazing results. I found it on the bookshelf of another supervisor, who gave it to me without reading it! There’s a great explanation of how Shingo’s feet blistered while playing golf and how it led him to a breakthrough in changeover reduction.
Number 1: Toyota Production System – Taiichi Ohno
Written by the man who was essentially responsible for Toyota’s vast success over many decades. This book explains what Toyota did, why they did it, and the results they were able to achieve. All the other “Lean” books just interpret what Ohno did and why he did it. He didn’t want to write a book, but thank goodness he did!
Honorable mention 1: The Innovator’s Dilemma – Clayton Christiansen
This book explains the impact of disruptive technologies on the world. It not only gives many case studies, but also explains what companies should do to become disruptive in their industries.
Honorable mention 2: Today and Tomorrow – Henry Ford
Written almost 100 years ago, the very elements of Lean are described by the man who put a car in everyone’s driveway. Taiichi Ohno was inspired by Henry Ford and so was I.
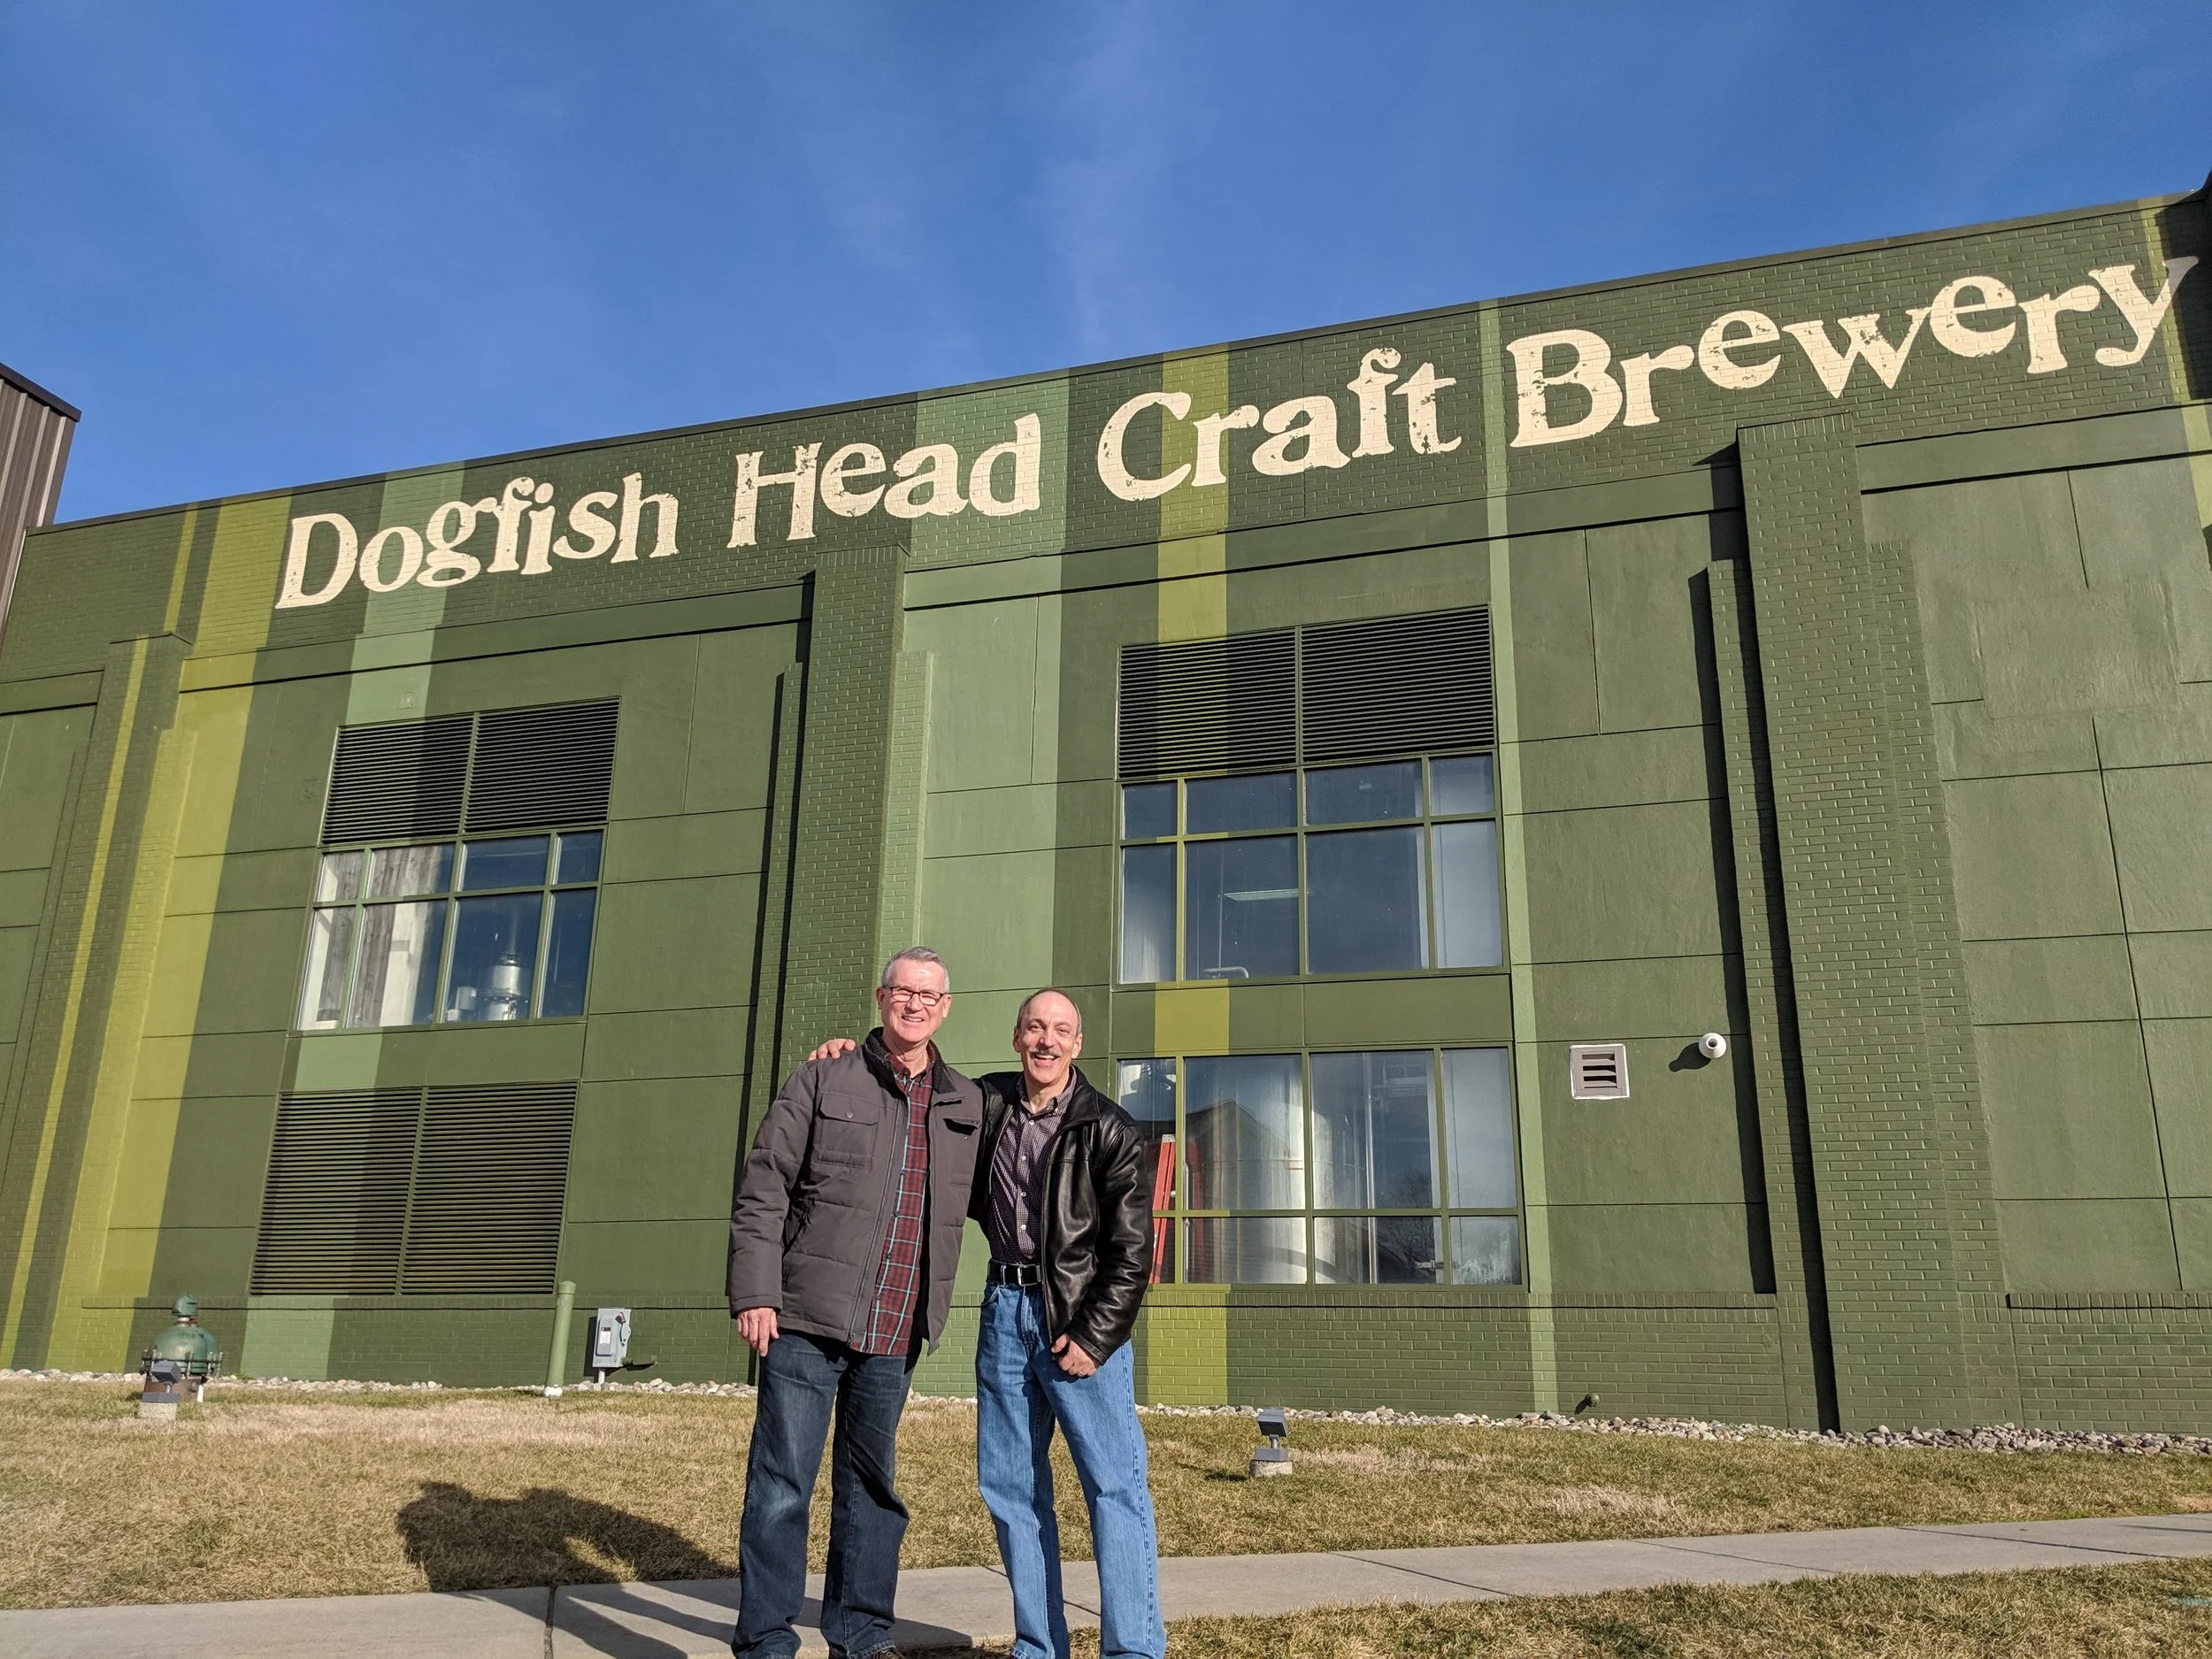
PIP Visits Dogfish Head Brewery
One of the benefits of being in business for yourself is to decide what’s most important to you and then prioritize your time to let you do what you are most passionate about.
One of the benefits of being in business for yourself is to decide what’s most important to you and then prioritize your time to let you do what you are most passionate about.
Recently, I had the opportunity to visit with Gordon Zavilla. Gordon and I worked together at Armstrong a few years ago and he was interested in accelerating Dogfish Head Brewery’s continuous improvement journey. Gordon invited his boss, Brian Hollinger to join us during the visit. We took a walk of the processes and shared ideas of ways to immediately improve safety, productivity, and customer service. We also discussed a strategic approach to the improvements they want to make. Their culture of employee engagement and creativity is a great foundation from which to build on.
One of the most creative tool boards I have seen was in their maintenance shop. Notice how there are actually three boards in one. No searching for anything in traditional tool boxes.
Thanks to Gordon and the great folks at Dogfish Head who taught me what it means to be “Dogfishy”.
Listen To Your People, People
A Research and Development team wanted to create a three-year strategic plan. Their goal was to reduce the time it takes from a new product idea to launch of the new product. Many of the team members believed “you can’t schedule invention.” Working with the team leader, the Research and Development Director, we decided to focus on the work leading up to and supporting the invention, even if we couldn’t specify when an invention would occur. We agreed to use Value Stream Mapping as the approach to help the team accomplish their goals.
A Research and Development team wanted to create a three-year strategic plan. Their goal was to reduce the time it takes from a new product idea to launch of the new product. Many of the team members believed “you can’t schedule invention.” Working with the team leader, the Research and Development Director, we decided to focus on the work leading up to and supporting the invention, even if we couldn’t specify when an invention would occur. We agreed to use Value Stream Mapping as the approach to help the team accomplish their goals.
On the first day of a Value Stream Mapping event, the team learned about Lean tools and techniques, and then quickly went to Gemba (the place where the work is done) to see what was actually happening in their current process, the Current State. Most people who haven’t participated in a Value Stream Mapping event don’t appreciate the time and effort put into understanding the Current State of their process. They want to work on the Future State, thinking they already know the issues, pain, and problems in their current process. But, as Lean practitioners know, there are always breakthroughs and “A-Ha” moments that occur during the Current State review that lead to a much stronger plan for the Future State.
The team wondered how they could walk their Current State, as much of their work was on their computers, at their desks, in labs, and other testing facilities located in the building. Ever the optimist, I encouraged the team to walk the process, regardless of where the work got done to uncover something that would help them on their journey to the Future State. Although they were skeptical, they agreed to follow my lead. We walked around the offices first.
We saw different people working at their desks and asked them questions about what they were doing. They did their best to explain things, but I noticed most people weren’t taking notes or asking many questions.
Our next stop on our walk was at a large wall containing a wide variety of graphs, charts, and documents. The R&D Director stopped there and told us proudly about how much information he shared with his people and how much they used the information on the wall. The team seemed satisfied with the explanation, but to me, it looked like a bunch of clutter. There were so many charts and graphs, it was unclear what was important, relevant, and critical to the work of the R&D employees.
I walked over to a Scientist who was working at his desk and asked him if he could join us at the board. I asked him what he thought of all of the information that was posted on the wall. He told the group that he didn’t know, he never looked at it. The team, including the R&D Director was shocked. Was this scientist the only one who didn’t use the information or were there others? As it turned out, there were others working in the area who confirmed they didn’t use the information on the board either. I didn’t want to insult our leader, so we continued our walk through the process, taking note of other issues as we saw them. The team started opening up and asking tougher questions as we went further into the process.
After we completed our walk, the team listed all of the steps in the current process and the issues and problems that existed. One of the biggest problems identified was the lack of communication of relevant information to the scientists. It was just as our brave Scientist had said during the Gemba Walk. Now, the team knew what it had to do in the Future State: Provide visible, relevant, and timely information to the scientists in a way that would help them do their work every day. Over the rest of the three days, the team built a path to the Future State that reduced time from new product idea to launch significantly. Much of the effort centered around providing the proper information to the people who needed it. Instead of assuming what was needed, they included the scientists and technicians in the development of the communication of highest value.
Over time, this communication was developed. In addition, the team created feedback loops to verify the communication was helping R&D employees do their work. Ultimately, the time from new product idea to launch was reduced significantly. More importantly, the team realized how important it is to include people in the design of systems that will be used for their benefit. One properly posed question can save months of effort.
350 Business Owners
An engineered flooring plant in Kentucky was losing money. They knew their product yields were deteriorating and didn’t know what to do about it. Process Improvement Partners was invited for a site visit. After reviewing performance and discussing the issues with plant leaders in a meeting room, we took a Gemba Walk to see what was actually happening.
An engineered flooring plant in Kentucky was losing money. They knew their product yields were deteriorating and didn’t know what to do about it. Process Improvement Partners was invited for a site visit. After reviewing performance and discussing the issues with plant leaders in a meeting room, we took a Gemba Walk to see what was actually happening.
As we walked around the plant, it was obvious that safety was the top priority in the plant. There was signage and effective placement of supporting tools and materials. Most importantly, all leaders in the plant were demonstrating their commitment to safety. It was clear production was the next priority. There were hour by hour production boards, and all kinds of measures of productivity posted around the lines and in the offices. There was no sign of the importance of quality or yield to be found. We searched all over the plant, but there was nothing that showed people what to do to reduce defects or improve yields.
We suggested a three-day Kaizen to develop managing systems to shift the plant from a culture of productivity to one of quality and yield. The Plant Manager was unsure how we would do that, but was open to the possibility of using a Kaizen for such a significant effort. We agreed the team would be made up of all of the members of the plant leadership team, with a few extra guests added to provide outside perspective. We also suggested a few highly trusted production operators be included on the team, as they would provide an unfiltered view of what they would need in support of their efforts to improve yield and quality.
The Plant Manager was not comfortable with the production operators participating in the entire Kaizen, but did agree they should participate in part of the agenda to provide their perspective on efforts to improve yield and quality. Their part would be on the agenda on the first day, representing the Voice of the Customer.
The Kaizen started with a kick-off from the Plant Manager. It was clear most of the team wasn’t sure anything important was going to happen during the three scheduled days and were wondering why they weren’t in the plant running operations. After introductions, we reviewed some Lean managing systems and had a discussion about the current mind-set and culture of the plant. It was apparent all team members valued safety above all and then production. They were not sure quality and yield was well emphasized or even highlighted.
At about 10:30am, a group of six production operators and two production supervisors entered the room. They took their seats with the rest of the team and waited uncomfortably to see what would happen next. It seemed as though nobody had explained to them why they were there and they hadn’t interacted with the leadership team in this type of setting before.
I thanked them for joining us and explained the purpose of the three-day Kaizen and their role in this part of the agenda. They were our Customers. They were not impressed. Next, I told them we wanted to get their honest feedback about how the plant was run. Still not impressed or even believing we would listen to and use their feedback, it seemed likely they wouldn’t offer anything of value unless I could get them to relax and open up.
I asked a series of open-ended questions, such as “What is the message you currently receive about the importance of quality and yield vs. productivity? Is it clear or confusing? How do you decide to prioritize productivity vs. quality and yield vs. safety when you are in the middle of a production run?” A few gave some short, terse answers, and a few of the leadership team members asked follow-up questions to show they were listening. Still, nothing of high value was being shared.
After about 30 minutes of questioning and terse answering, I asked this question, “If you could change one thing about how the plant is run, what would it be?” One of the production operators, let’s call her Sally, blurted out, “If these SUMBICHES would just care enough to come to work every day, things would be better!” Blushing, she put her face in her hands. The room roared and clapped with approval. The Plant Manager thanked her for being so open and honest and said he wanted to know more about what she meant by her statement.
All of the sudden, the Customers opened up and told the team exactly what they thought. They talked about the leadership approach and the message that was being sent to the production operation about the value of quality and yield. People were now sharing their thoughts, feelings, and ideas, and leadership was listening. We were getting somewhere. After another hour or so, we had exhausted all topics and thanked our Customers for joining us. There were handshakes, high fives, and hugs and everyone left feeling like they had contributed to something important. It was clear that the production operators and supervisors truly cared about the company and its impact on their families and the community.
The team now knew they had important work to do, and the next step was to create a vision for the plant emphasizing what their customers needed to do their job in the best possible way. It didn’t take long, and they came up with this vision statement:
“350 business owners with a yield-first mindset making every plank matter. Close is not good enough – stop until the customer will be delighted. Encourage everyone to take the time to make it right the first time.”
The rest of the Kaizen was spent developing strategy and tactics to support and emphasize the new vision. There was energy and excitement, and by the end of the Kaizen, you could see and feel the difference in the plant. The initial results were promising, as quality and yield performance improved. More than that, 350 people were aligned around what’s most important to them, their families, and their community.
Owning Their Solution in the Weld Shop
I have conducted many workplace organization Kaizens (5S) over the years. The results have always been dramatic. All of the teams were made up of production operators or office workers, with some mechanics assisting the team. The production operators or office workers owned the areas needing organization and the mechanics were able to do some of the more complex tasks needed during the Kaizen. All of the teams, that is, until I met my Weld Shop team. Five mechanics and an engineer, who underestimated what we could accomplish.
I have conducted many workplace organization Kaizens (5S) over the years. The results have always been dramatic. All of the teams were made up of production operators or office workers, with some mechanics assisting the team. The production operators or office workers owned the areas needing organization and the mechanics were able to do some of the more complex tasks needed during the Kaizen. All of the teams, that is, until I met my Weld Shop team. Five mechanics and an engineer, who underestimated what we could accomplish.
Let me tell you about a typical mechanic on a Kaizen team. He or she is there to support the team, but not usually vested in the improvement process. Most of the time, they participate in the Kaizen and do great work, but sometimes they aren’t interested in being there, and would rather be doing their “normal” job. Facilitating a Kaizen with a team where some of the members were this way was not new for me, but having the entire team this way was. The good news was the area we were going to be working on would directly impact their safety and productivity. The better news was they had a supervisor, acting as the team leader, who was extremely excited about the possibility of improving the weld shop. And the best news was I could leverage their pride and competitive nature to turn their existing Weld Shop into a show place for all the world to see. Only if I could get them to own the improvements, of course.
When I run a 5S Kaizen, I do it step by step. On the first day of the Kaizen, after training the team in all of the S’s, we took a walk in the space we were going to organize. I asked the team to identify things we could remove first – the clutter. This is the first S. I asked many questions and they identified the items to be removed while I took photos. Then, after removing all of the clutter, we decided on the best locations for anything remaining in the space. We did this in an organized fashion and I had team members demonstrate how each new location would be safer and more productive than the old location. This is the second S – Set in Order. Following this, we made sure that everything left in the shop was in the best possible shape. We did this by cleaning and inspecting all tools, equipment, materials, and storage spaces. If we found something in disrepair, we either fixed it or replaced it. We relied on everything in the area to work, so we took great care. This is the third S – Shine.
The first three S’s, Sort, Set in Order, and Shine, are the most physical, dramatic, and fun parts of the Kaizen. By the time we got to the fourth and fifth S, the team was extremely energized and the area looked dramatically different from where we started. Here’s an example: Before we started the Kaizen, you had to enter the Weld Shop and walk about 30 feet to turn on the lights. To get to the light switch, you had to navigate in the dark through all of the clutter in the hopes of finding the switch without running into something. In some of the initial “before” photos, you couldn’t tell there was a light switch on the wall at all. During the evening of the second day of the Kaizen, we relocated the light switch to the entrance of the Weld Shop, on an outside wall. Lights could now be turned on before entering the shop, eliminating the safety risk of navigating in the dark to the switch.
The fourth S is Standardize. For this step, the team was tasked to create a managing system to ensure the improvements they made would continue to live on, be supported and requirements followed by everyone using Weld Shop in the future. This was not a physical exercise. It was a mental and paper exercise. Teams typically create checklists, sign-off sheets, signs, and audits that must be followed by anyone using the area. To mechanics, this is “paperwork”, and although it has more than four letters, it might as well be a four-letter word. This is the last thing they wanted to work on, and I knew that. I also knew that this was the most important step, as their improvements would deteriorate back to the “before” condition if not done properly and completely. The real trick would be for the team to own their solution and not just go through the motions. I had a plan, but it was risky. I needed to facilitate an emotional event, so the team would create and own their managing system.
On the morning of the third day of the Kaizen, after congratulating the team on the improvements of the first two days, I explained this would be “Standardize and Sustain Day”. They looked at me with grumpy faces as I showed them examples of checklists and audits other teams had developed. They were not impressed, to say the least. In fact, they didn’t believe simple pieces of paper would keep people from messing up all of their good work. I showed them examples of how teams made these documents visible and established responsibility all the way up to plant leadership. They were still not buying it. I needed to push them further.
I showed a slide of a checklist, going line by line over each requirement. I could see the discomfort and frustration in their faces. I was on line eight of the checklist when one of the mechanics, whose face was beet red said, “Adam, we’ve had enough of your paperwork. We’re going to the smoke shack. You can’t come with us. We’ll figure it out and then we’ll tell you what we’re going to do.” All of the team members stormed off and left me in the meeting room by myself. I had facilitated the significant emotional event. I didn’t really know if they would ever come back, and if they did, what would they come back with?
It felt like two hours, but it was only twenty minutes when all of the team members returned to the meeting room. They looked pretty proud of themselves as one of them declared, “Adam, we’re going to tell you what we’re going to do. We’ll talk and you type.” They listed eleven things they wanted on “their” checklist. They were similar to what I had presented, but it was in their words and it was their ideas, and that’s all that mattered. I thanked them for coming up with such a well-thought out checklist and then challenged them to develop the system to ensure everyone would use it properly and not “pencil-whip” it. This is the fifth S, Sustain. Enthusiastic and full of pride, the team developed a visual Area Owner board, with all of the required documents easy to find and to use. Then they set up daily and weekly requirements for the area users, the Area Owner, and members of the plant leadership team.
On the final day of the Kaizen, the team shared their results with the plant leadership team and some executives visiting from their corporate office. It’s not unusual for mechanics to shy away from presenting in front of an audience. In this case, all team members spoke from their hearts and explained how important it would be to support and sustain all of their good work, which was improving safety and productivity for them and the rest of the plant. They even asked the executives to hold the team and plant leadership accountable to keep this good thing going and spread this effort to other areas of the plant.
After the presentation was over, I spent a few minutes with the team, getting their final thoughts about the Kaizen. Happy with the results and most aspects of the Kaizen, they told me they wished I had been more assertive with them during the week. We laughed as I told them I wasn’t sure they were coming back to the meeting room after storming out on Standardize and Sustain Day. They told me it was just the motivation they needed to get to their solution.
Breaking Through - The Edge
In 2005, I was asked to help a team reduce the changeover time of a painting operation at a ceiling tile manufacturing plant in Oregon. The approach I used was SMED – Single Minute Exchange of Die. The goal was to reduce the existing changeover time by 50% or more, while improving the safety of the work.
In 2005, I was asked to help a team reduce the changeover time of a painting operation at a ceiling tile manufacturing plant in Oregon. The approach I used was SMED – Single Minute Exchange of Die. The goal was to reduce the existing changeover time by 50% or more, while improving the safety of the work.
After training the team, we took a walk on the factory floor to observe a changeover in progress and see if we could generate any improvement ideas. As with most SMED events, we saw a ton of improvement opportunities related to the existing changeover and the team was excited they would be able to help everyone in the process.
Towards the end of the walk, we stopped at the quality testing station and saw something that didn’t look right to us. The Quality Technician was using a box knife to cut four 2-foot edges of the ceiling tile off by hand. It looked difficult, unsafe, and extremely inefficient. When we asked her more about it, she told us she was required to measure the color of the face and edges of the ceiling tiles. The only way to get the colorimeter to read the edge of the ceiling tile was to make these cuts, allowing the tester to be placed directly on the edges. She also told us it made her wrists hurt. On a break, I verified with plant leadership they were also very concerned about this requirement. It was their number one safety concern in the facility and a number of engineers had studied the issue with no practical solution.
Following the walk, the team went back to their meeting room and listed all of the improvement ideas they had. They then prioritized the ones they wanted to work on to reduce changeover time. During the next two days, many of the highest priority ideas were implemented and the team was extremely excited about the improvements they were able to make.
At a break, a mechanic on the team came up to me and asked if it would be ok for him to work on something outside of the prioritized list of improvements the team had identified. I could tell something was bothering him, so I asked him to tell me more about what he was thinking. “Adam, I can’t get that edge cutting process out of my mind. It’s not right that we are putting our people at risk. I think I have a solution, and if you give me an hour to work on it, I can come right back to the team to help out with the other efforts.”
Kaizen is a team sport, and the team needs to be aligned around what everyone is doing. I asked the team what they thought. They enthusiastically supported the mechanic’s efforts. So much so that one of the operators volunteered to help him work on his idea. We couldn’t wait to see what they would come up with.
About an hour and half later, both team members came back with grins a mile wide. They brought a contraption that looked like a standard vise with a two-foot wide angle iron attached to each jaw. Curious, we stopped our other work to watch a demonstration of their invention. They put a 2-foot ceiling tile into the vise vertically, with the edge of the tile in the jaws and closed the vise carefully. Then, with a swift tap, the ceiling tile broke off cleanly at the edge, across the entire 2-foot length. We were stunned. One of our team members stepped up and tried the next of the four edges, and it broke off just as cleanly. One by one, we all tried it and saw how quick and easy it was to break off the edges. Now, we gave it the ultimate test – we brought it to the Quality Technician and showed her how to use it. She easily broke off the edge and immediately gave the mechanic a hug in a show of gratitude. It was probably the only hug the mechanic ever got at the plant!
We were so proud, but knew we had to finish our other work and gain alignment from plant leadership that our new method would meet the quality testing requirements. During the rest of the Kaizen, we implemented as many of our improvement ideas as possible, then created an overall changeover procedure that we verified, practiced, and used to train the rest of the operators on the line. The changeover time had been reduced significantly, but we wouldn’t feel like we had won until we implemented the new edge breaking process. So, we decided to build a final report to win over the plant leadership.
We invited plant leadership to see the new changeover procedure, which the team demonstrated for them. Some of the leadership team even participated, to see for themselves how much easier and safer it had become. They were extremely pleased, but we had saved the best for last.
Our creative mechanic invited the Quality Technician to join him in front of the group of plant leaders. Then, another team member brought out the vise and handed a ceiling tile to the Quality Technician. She put it in the vise, gave it a tap, and the edge broke right off, as clean as could be. In my life, I have never seen a collective group of people’s jaws drop at the same time, but it happened right then. After they got over their initial shock, the Operations Manager said, “Let me try that.” He did, and got the same result.
Everyone wanted a turn, and when it was over, the Safety Manager said, “This has been our number one safety risk. We have spent over 6 months trying to solve it the conventional way and haven’t been able to do so. Your team worked together and solved it so quickly. We need more teams to help us solve our problems in this way. Thank you!” Then, she gave the mechanic the second hug he had ever received in the plant. After blushing, he admitted to the group that in all of his years working at the plant, he had never done anything as impactful as this. He also reminded everyone that this was a prototype, so there may be an improved way of doing the work. Many years later, the original vise was being used in the plant without a complaint.
Improving Changeover Time in 4 Simple Steps
Have you ever watched an auto race? If so, you probably noticed what happens when a car enters Pit Row and is tended to by a whole team of people trying to get it back on the track as fast as possible. If you wondered how they knew what to do and how they didn’t get in each other’s way, the answer is SMED.
Have you ever watched an auto race? If so, you probably noticed what happens when a car enters Pit Row and is tended to by a whole team of people trying to get it back on the track as fast as possible. If you wondered how they knew what to do and how they didn’t get in each other’s way, the answer is SMED.
SMED stands for Single Minute Exchange of Die. It was developed by Dr. Shigeo Shingo in the 1960’s and 1970’s on behalf of Toyota. Dr. Shingo was interested in reducing the time and effort that it took to change a production line from one product to the next. By intense study and trial and error, he developed a 4-step method to drive all changeovers down to less than 10 minutes, thus coining the term single minute exchange of die. For auto racers, they use SMED to improve their auto changeover times and have achieved times below 15 seconds.
Changeover reduction is a team sport, just like in NASCAR, so picking the right team is critical. Bring people together who have had experience with the changeover being studied, use their differing opinions and techniques and encourage sharing and learning. By doing this and applying SMED, you should be able to reduce changeover time by more than 50%. You should also be able to improve the safety of the changeover for everyone.
STEP 1 – Identify All Elements of the Existing Changeover
The first step in SMED is to identify all elements of the existing changeover. This is done by observing the changeover as it occurs. Use a changeover that is typical for the process. Teams use tools such as a stop watch, video, and spaghetti diagram to truly understand everything that is happening during the changeover. Rather than just discussing things, they observe the changeover and then discuss it to better understand the current situation. It is also not unusual for team members to mimic the steps of the changeover so they can see the impact and difficulty of the changeover for themselves.
The spaghetti diagram is a paper exercise that shows everywhere a person travels during the changeover, whether it is to get tools, information, or do work on equipment. To use it, you should have a general layout of the area being worked on, then place a pen or pencil on the layout, moving it to the places that the worker moves during the changeover. Don’t lift the pen or pencil. If there is more than one worker performing the changeover, there should be more people creating the spaghetti diagram. At the end of that exercise, the lines on the page tend to look like spaghetti and people are amazed at the amount of travel required to complete the changeover.
STEP 2 – Separate All Elements into External and Internal
The next step in SMED is to identify what steps or elements can be performed while the line is running (External elements) and what steps must be performed while the line is down and waiting (Internal elements). Process Improvement Partners saw an example of this in one of our sessions. After a production run was completed, the press was shut off, a die was removed, the die was returned to storage, and the new die was brought back to the press from the storage area. At that point, every step was Internal, meaning that the line was not running while each step was completed. However, the team soon realized that the retrieving of the new die could have been done in advance of the changeover and the storage of the other die could be done after the line was back up and running. The team identified all of the elements that were external, and this step saved more than 25% of the changeover time.
STEP 3 – Convert Internal Elements to External Elements
The third step challenges the team’s creativity and they start to devise ways of doing some of the changeover steps that originally had to be done while the line is down and finding ways of completing them while the line is still running. A team we worked with created a fixture that allowed parts to be positioned for installation prior to the line stopping. This saved a significant amount of time and the fixture was built with existing materials, so no money was spent. Another example is to connect a tool to the equipment, so that it is immediately accessible to do the work once the line has been stopped. There are so many examples of this that teams can do research through the internet to get ideas, or they can visit other manufacturers to see the ideas in action.
STEP 4 – Streamline All Elements
In this step, the team thinks of ways of shortening time and effort required to do any remaining elements. They prioritize and work on the internal elements first, and then work on any of the external elements that have opportunity for improvement. This is a great time to look at the video and the spaghetti diagram again and see if the amount of travel can be reduced by the repositioning of tools, materials, and equipment, or if another sequence would be more efficient. Trial the new procedure, redraw the spaghetti diagram, and get the input of all team members to ensure that the new steps are truly better for them.
Once all steps of SMED have been completed, the team should observe the new changeover procedure and verify that it is truly an improvement. Time is one measurement, but effort, travel, and the anecdotal input of those performing the new changeover procedure are also important. People need to feel that the new way is better than what they had been doing personally. Because change is difficult, the team needs to develop methods to sustain the improvements that they created. Once they do so, they will realize the benefits of their efforts.
A Simple Way to Think about a Problem You Want to Solve
Many years ago, I was having difficulty getting my mind straight about a problem that I wanted to solve. A co-worker of mine introduced me to a thing he called a “Task Cycle”. Once I understood it, I had a simple way to go about solving problems and executing tasks.
Many years ago, I was having difficulty getting my mind straight about a problem that I wanted to solve. A co-worker of mine introduced me to a thing he called a “Task Cycle”. Once I understood it, I had a simple way to go about solving problems and executing tasks.
The Task Cycle was developed in the early 1990’s by Paul Boulian and revised by Marlyn Rabenold eight years later. I had the good fortune of meeting Marlyn and was amazed at the simplicity of thinking that can be used to help solve the most complex problems. Now, I want to share it with you.
The Task Cycle has 4 components: Purpose, Products, Process, and Functional Capabilities. It is truly a cycle and can be visualized in this way:

When you are planning a task (or planning to solve a problem), you follow the cycle counter-clockwise, from Purpose to Products, Process, and then Functional Capabilities. When Executing a task, you follow the cycle clockwise and start at the Functional Capabilities and end at Purpose.
Purpose
This is the reason that we are trying to do something, or the problem that we are trying to solve. That seems simple, and it is, but building a clear purpose statement is critical, and should not be taken lightly. As is said, the first step in solving a problem is know that you have one in the first place. When building a clear Purpose statement, consider and communicate why you want to do something, as much or more than what the specific task is. Consider these components of the Purpose statement with this recommended format:
“TO” – describe the task to be done or the problem to be solved
“IN A WAY THAT” – describe the benefit to be realized by the accomplishment of the task. Think in terms of the customer of the task.
“SO THAT” – describe the impact or result the task will have on the organization
Using the experience of writing this article, here’s an example of a Purpose statement:
To write a description of the Task Cycle, in a way that:
- Exposes the reader to a new way of thinking about a task
- Provides a simple construct for dealing with a complex problem or effort
- Engages the reader’s interest
So that this knowledge will help readers in their efforts to solve problems in the future.
Clarity of purpose helps us gain alignment and support from those who will either help us with our task or those who have assigned the task to us.
Now that Purpose has been established, it’s time to move on to Products.
Products
Products are the output or results that we are trying to create when we accomplish the task or solve the problem. A good question to ask is, “If we accomplish the task or solve the problem, what would we see or know that reinforces that the task is complete or the problem is solved?” We aren’t always looking for a physical product, but also non-physical or virtual products. These can be timing, a new way of doing things, or other similar results. Products of the prior example could be:
1. Ten or more responses or inquiries about the article
2. Three shares of the article
3. A phone call to discuss more in detail about the article
Now that the Purpose and Products have been identified, it’s time to move on to Process.
Process
How are we going to get the products that tell us that we have achieved our purpose? What is the methodology or approach that we will use to do this? We can now design a process to specifically accomplish the purpose and deliver the products as stated. Whether we use existing tools and methodologies that we are familiar with, or do research and ask others for their input, we can now test our thinking and approach and see if it delivers the desired results. We want to think through the series of steps and actions that we will take in order to get where we want to go. Because we are clear on purpose and products, we can now design process in a way that has the least amount of effort and waste associated with it.
For the prior example, the process being used is to research the original thinking and documentation on the Task Cycle, consider my personal experiences with it, and try to describe it in a way that the reader can utilize practically. Time will tell if my process was properly thought out.
Functional Capabilities
Do you need people to help you accomplish your task or solve the problem? Do you need tools for this? Are there skills that need to be acquired? What else do you need to solve the problem or complete the task? These are the questions that should be answered in order to identify the functional capabilities needed.
When all four components of the Task Cycle are put together, they should be the foundation for the effort. You should share your thinking with others to see if you have missed any vital elements, always improving as you go. You might even need funding, and that is why it is critical to have alignment around your task cycle.
Earlier in the article, I stated that when you are executing a task or solving a problem, you now go through the task cycle in the opposite direction. What I mean is that you use the functional capabilities to follow the process, which delivers the products and ultimately achieves the purpose.
Although this is not new thinking, I believe that many have forgotten about the Task Cycle and are missing out on this simple way of solving problems and accomplishing critical tasks. I will be interested to see if I accomplished my task in providing you with information that you can use. Your feedback will let me know if I have done so.
Who is Your Customer?
We are all customers. We want what we want, when we want it, at the level of quality we expect, in the proper quantity. We are the final say as to whether a business will thrive, survive, flounder, or die. The business must deliver to our expectations, or we will not continue to purchase products or services that they offer.
We are all customers. We want what we want, when we want it, at the level of quality we expect, in the proper quantity. We are the final say as to whether a business will thrive, survive, flounder, or die. The business must deliver to our expectations, or we will not continue to purchase products or services that they offer.
It’s surprising how many businesses wrongly believe shareholders are their customer, rather than those who actually derive benefit from what they offer.
A key principle of Lean is that everything should be optimized to the benefit of the customer, and anything that doesn’t deliver value is considered waste and should be eliminated.
It is therefore critical that you understand who your customer is, what is most important to them, and what they perceive as value.
Identify Your Customer
Questions to consider to identify your customer(s):
Do they pay for your product or service?
Do they provide feedback about your product or service, and how it affects them directly?
Do your actions directly influence their behaviors?
Do they depend on you for the product or service that you deliver?
Sometimes, we need to look internally to identify our customer(s). For example, in a manufacturing plant, one department receives a product from another department. The receiving department is the customer of the delivering department, and requires the product to be the proper quantity, quality, and to arrive on schedule. Anything that deviates from this is waste and should be eliminated.
Likewise, the workers in the same manufacturing plant are the customers of the Leadership Team, who makes decisions on their behalf. Their families are also customers as strong business decisions keep paychecks rolling in.
What is Most Important to Your Customer
Once you have identified your customer(s), you then need to understand what they truly want from you or another provider. To find out, you can analyze market trends, speak to your Sales and Marketing departments, host focus groups, and/or go directly to your customers and find out. Oftentimes, customers may not be able to directly identify everything that they want, but with the proper questions, you should be able to get the heart of their issues. Consider these questions:
What do you like about the product or service that we provide?
What don’t you like about the product or service that we provide?
What issue or need are you trying to solve with the product or service that we provide?
What are we not providing that you wish we would provide?
What changes would you make to our product or service that would make things better for you?
What do you wish you could say to our CEO about the product or service that we provide?
It’s surprising how effective face to face communication can be with customers. It’s also surprising how few of us use this method to extract critical information from them. Most people appreciate the opportunity to have these conversations. Now let’s talk about value.
A Question of Value
If you have identified your customer and reviewed what’s most important to them, you should be close to answer how they define value. Value isn’t necessarily a monetary thing, but can be thought of as something that enhances the customer experience. Some examples include:
Reduces time and/or effort
Simplifies a task
Enhances quality of life
Makes them happy
Keeps them safe and secure
And the list goes on
Once you have identified your customer, what is most important to them, and how they define value, you are ready to attack and eliminate waste in your business. To understand more about waste, read the blog entitled, “The Eight Deadly Wastes.”

Use Standardized Work to Unleash Creativity
Most people don’t like being told what to do. They definitely don’t want to be told how to do it. But, with proper standardized work, we can show people the right way to do things and free their minds to work on more complex problems that they face.
Most people don’t like being told what to do. They definitely don’t want to be told how to do it. But, with proper standardized work, we can show people the right way to do things and free their minds to work on more complex problems that they face. The key is to develop standardized work that engages people, speaks to them at the appropriate level, and captures the routine aspects of a task in a way that ensures everyone follows it properly and easily. Once that occurs, they can concentrate on solving problems that aren’t covered by the standardized work.
When I was very young, I was told, “Don’t touch the stove top. It’s hot!” Naturally, that sparked my curiosity. I wanted to know how hot, so I had to touch it. Unfortunately, I got burned and learned a lesson. I should have asked “How hot?” or, “What happens if I touch it?” If I understood what and why and the implications, I may not have received a boo-boo. This was a valuable personal lesson, but it also provides a good structure for standardized work. Now that I didn’t have to touch the stove anymore, I was freed up to use my creativity to create other mischief.
How to Engage Your People to Develop Standardized Work
People tend to do things the way they are taught, the way they observe, or the way that feels right to them. Unfortunately, they may be doing things improperly, unsafely, or inefficiently. So, it is incumbent on you to help them see the better way to do their work. The best way is to engage them in the development of the work. I have found that you should engage at least three people who are currently doing the work so they can share experiences, approaches, and break the tie, if a final decision on how to proceed is needed. You should set the expectations that work must be accomplished safely and productively, but give them the freedom to use their experiences to guide them in the process.
What To Do
The first part of standardized work is to define what to do and the order in which the work must be done. Once you have engaged people who do the work to participate in this effort, have each one of them demonstrate their approach to the work. Those who are watching should provide feedback and ideas that would make the work safer and more efficient. Once all ideas are shared, help bring the group to consensus around the final procedure. Once they have done this, they should practice the new procedure and see if they have missed any vital elements. Following that, document the procedures with pictures, videos, and/or written process steps. The more visual the better, as you want to be able to explain the procedure to anyone in a short amount of time, and you want them to be able to demonstrate their understanding without much effort. Once they have reached consensus, you must gain agreement that the procedure will be followed the same way by everyone who does the work.
Why To Do It
You can’t guarantee people will follow the new procedure, just because it is safer and more efficient. They may not realize this is the case. Most people are willing to try something different than what they are used to if they understand why it will be a benefit to them. Therefore, the group that develops the new procedure should incorporate the “why” or benefits behind the steps in the new procedure. If they’re unable to do so, it probably means there aren’t real benefits and the procedure needs improvement. Keep working and improving the procedure until you have something that delivers a benefit. Once you have done that, it will be easier to sell the new procedure to others.
The Implications of the Work
The best standardized work results in safety and efficiency gains. These should be clear and measurable. After all, how do you know you’re winning if you’re not keeping score. So, the team should be able to identify and incorporate clear measures of the standardized work. For example, the procedure now takes six steps and 30 minutes, while in the past it took 12 steps and 48 minutes. Another example is the new procedure results in a higher yield rate than the old procedure. It is not uncommon to reduce the time required to accomplish a task by 30% to 50%, just by gaining alignment and simplifying process steps.
Using these three elements – what to do, why to do it, and the implications of the work should convince people to try this new way of operating. Once they are convinced, they should also see that by following this new process, their minds are freed-up to work on more complex problems, thus unleashing their creativity.
Here’s a real-world example: A production line was shutting down erratically. In the past, people would be blamed for not following procedures. With clear standardized work, the time to troubleshoot was reduced dramatically, as the human variables were eliminated. The team could focus on other reasons and quickly found the root cause of the problem, which was a switch that was shorting out.
We want people to be creative and improve things and solve complex problems. By creating clear standardized work that is consistently followed, we give people the opportunity to use their creative minds and drive positive results.
The 8 Deadly Wastes
The customer defines value for any product or service. If they aren’t willing to pay for something, it has no value to them. In the terminology of Lean, anything that doesn’t directly provide value to the customer is called “waste”. Further, there are eight specific types of waste.
The customer defines value for any product or service. If they aren’t willing to pay for something, it has no value to them. In the terminology of Lean, anything that doesn’t directly provide value to the customer is called “waste”. Further, there are eight specific types of waste. Once you know what they are, you can begin to spot them, and then work diligently to reduce or eliminate them. If you do, the customer experience will be improved and so will your operating results.
These are the eight deadly wastes:
Transportation
The movement of anything from place to place is considered waste, because it adds no value to the product or service being provided. It only adds time, and the potential for loss or damage. It may seem necessary to move things around in a process – putting things in trucks, putting things away on shelves, sending electronic data from one server to the next, but there is no change to the form or function of the thing being produced. The question to ask is, “how can we reduce or eliminate transportation in the process?”
Inventory
Ideally, the only product you should produce is the product that your customer wants; no more, no less. More production creates inventory. Less production creates a shortage. The risk of having too much inventory is that it may spoil, become obsolete, or never leave the shelf. Think about computer chips. Once the new version of computer chip comes out, who is buying the older version? Typically, nobody, or if they do, they are receiving a sizable discount. Another problem with inventory is that the thing you need may get lost behind the thing you don’t need. So, you end up producing more inventory that can hide the next thing, and the cycle continues.
Motion
This waste addresses the effort required to complete a task. If you must reach over your head, or grab something from the ground, you are using extra motion. If you must go away from your area to track something down and retrieve something, you are using extra motion. Ergonomics, which is the study of people’s efficiency in their work environment, is a method to identify and reduce excess motion.
Waiting
Time lost while waiting for an answer, a return email, an earlier process step, booting up your computer, or general waiting around is considered waste. It can be frustrating, time consuming and adds to the overall time in the process, which delays delivery to the customer. The key is to find the things that force you to wait and strive to eliminate them. Empowering people to make decisions is a quick way to drive waiting time down.
Overproduction
Have you ever noticed people who print out every email that they receive? This is an example of overproduction. How about a production line that is running really well and the managers want to keep things running? While the current product gets produced, the next product waits. There is a risk there will be a shortage of the raw materials to make the next product, or that there will be a delay in shipping the next product to the customer.
Overprocessing
This waste refers to the complexity in the process. If there are more steps than needed, or if the product or service is delivering beyond the requirements of the customer, this can be thought of as overprocessing. In the 1930’s, there was a cartoonist named Rube Goldberg, who devised the most complex ways of completing simple tasks. It was entertaining and creative, but not the ideal way of accomplishing work.
Defects
When the product or service doesn’t deliver to the required level of quality, this is considered a defect. When something has to be reworked, this is considered a defect. Many companies try to instill a culture of “Doing it right the first time.” They want to ensure that each process step will continue adding value to the benefit of the customer.
Unused Employee Creativity
The people who do the work generally have ideas to make their work simpler and safer. The best companies listen to their employees to get improvement ideas. Other companies think they know all of the answers and ignore suggestions by their employees. We don’t want people to shut their minds off when they come through the door, or we will be responsible for the worst waste of all.
In order to reduce or eliminate waste, you must be able to identify it. These eight wastes are easy to find in any process, if you are willing to look. If you make it a habit to reduce or eliminate these wastes, your customers will benefit. If your customers benefit, so will you.
What Process Improvement Partners Can Do for Your Team
Process Improvement Partners LLC offers a variety of services that help teams achieve breakthrough results. Some are narrow in scope, while others are strategic in nature. Some are quite simple, and others are extremely complex. In all cases, we strive to apply the right service to our customer’s needs, providing hands-on assistance, where needed.
Process Improvement Partners LLC offers a variety of services that help teams achieve breakthrough results. Some are narrow in scope, while others are strategic in nature. Some are quite simple, and others are extremely complex. In all cases, we strive to apply the right service to our customer’s needs, providing hands-on assistance, where needed. Here is a summary of our services, and when you might want to consider using them:
Site Assessment
If you want to see what opportunities are available to you, or don’t know where to start, take this 5 to 6-hour test drive with us. Everyone learns something new in this session. Together, we will identify the highest value opportunities and develop the plan to realize those opportunities. Some teams decide to take on the work themselves, others choose to engage us. Either way, it’s time well spent.
Cost Reduction Ideation, Prioritization, and Implementation
If you need to drive out costs in your business without negatively impacting your customers, this session is for you. Team members are challenged to come up with new and more efficient ways to do what they do, focusing on the cost impact to the organization. Once they have heard from their customers, they creatively brainstorm cost reduction opportunities, prioritize those opportunities, and then more fully develop and analyze those opportunities for customer and cost impact. At the end of the session, the team has a roadmap to drive significant costs out of the business.
Strategic Planning (VSM)
The first step in any continuous improvement journey. This session opens the eyes of all participants to the wastes and inefficiencies in their current processes and provides a roadmap to improvement that will be a direct benefit to their customers. Often, the team identifies simple and quick changes (6 – 12 months) that will reduce lead time to their customers by more than 50%, free up space, reduce the need for inventory, and improve quality and safety performance. This session also changes how people manage and lead in their processes moving forward. The benefits are felt immediately by those who work in the process, as well as customers of the process.
Workplace Organization (5S)
This session makes an immediate, visible and measurable impact on safety and productivity in a work space. It’s fun and fast paced, as team members learn how removing clutter, organizing items into optimal locations, maintaining resources in top condition, and implementing audits of the area can improve the lives of the people working in the space. Team members may get emotional at the end of the session, as they are positively impacted by the experience.
Breakthrough Creativity (3P)
Based on the proven 11-step Nakao method, this session is designed to drive teams to places they never dreamed possible in a 4 ½ day session. It is extremely challenging and exciting, as team members find solutions to problems that eluded them previously. This session is not for the faint of heart, as team members will work at a rapid pace and for long hours. When the session is over, it’s not unusual to have reduced project time by 6 months or more.
Changeover Reduction (SMED)
If you find that you are constantly expediting orders due to long product changeover times, this is the session you need. Using Single Minute Exchange of Die (SMED) methodology, teams typically reduce changeover times by half or more by the end of the session. Your customers will see the benefits of this session too, as lead times will be reduced as well. Teams will be trained so that they can apply the approach to other areas of their business in the future.
Process Optimization (Standard Work)
This session brings people together to determine the safest, most productive way to accomplish critical tasks. The team is guided through this session to create the new standard work for the improved process and develop the managing systems to ensure that everyone follows it once implemented.
Failure Prevention (FMEA)
An industry standard approach to stopping problems before they happen through the identification, prioritization, development, and implementation of preventative actions. This session stretches team member thinking as they are challenged to identify all of the ways a process could fail, whether the process has been implemented or not. Through a standard scoring system, these failure modes are prioritized for greatest negative impact to employees and customers. Once the session is over, the team will have a strong plan of action to keep these potential problems from occurring.
Plant Reliability Improvement (OEE)
This ongoing effort to drive to World Class Reliability utilizes Standard Work, Visual Management, Changeover Reduction, Shop Floor participation, Best Practice maintenance, and Continuous Improvement events. The team will build a road map of actions and strategies to improve Plant Reliability, and then they will be given assistance with any or all of their identified actions. We step back when the organization is ready to take full ownership of the improvement efforts.
Cultural Transformation
What does it take to drive an organization to a culture of continuous improvement? This ongoing effort utilizes leadership coaching, mentoring, demonstrations, and implementation of the key drivers of cultural transformation. The team starts with their vision and mission, and then designs all of their actions around them. Assistance is provided until the organization has shown that it owns the change that it seeks.
Visual Management and Shop Floor Participation (Gemba Walks)
The people who work in the process know what’s going on and are just waiting for an opportunity to share their ideas for improvement. This session engages the shop floor work force and improves accountability for daily results. The team builds a plan and leadership actions that will drive shop floor performance to higher levels and improve workforce engagement. Once the team implements visual management, there will be alignment and accountability for the most important results.
Best Practice Facilitation
How is that the best facilitators look like they aren’t doing anything at all, while the teams they are working with are making breakthroughs? This ½ day training session will provide the tools, methods, and hands-on practice to improve skills of the participants. The result will be more productive meetings and events.
If you don’t know which of these services to choose, just contact Process Improvement Partners LLC, and we’ll help you determine your best course of action. We are totally committed to your success. These sessions can drive your operating results to new heights.
Value Stream Mapping: The First Step on Your Continuous Improvement Journey
You can’t reach your destination if you don’t know how to get there. Maps, or in our technology-driven world, GPS systems, are critical resources for guiding you from point A to B. The same is true for your continuous improvement journey. Unlike your GPS, however, you must build your map through learning. The best way to build it is with Value Stream Mapping.
You can’t reach your destination if you don’t know how to get there. Maps, or in our technology-driven world, GPS systems, are critical resources for guiding you from point A to B. The same is true for your continuous improvement journey. Unlike your GPS, however, you must build your map through learning. The best way to build it is with Value Stream Mapping.
Value Stream Mapping views everything from the eyes of the customer. Anything that the customer would not pay for is considered Non-Value Added and is waste. The key to Value Stream Mapping is to see the waste in the current process and then develop strategies to remove as much waste as possible, delivering maximum value for the customer.
There are the 8 key components of Value Stream Mapping:
Identify the Value Stream to Map
What is the family of products or services that the customer is willing to pay for? Often, companies will pick a product or service that represents a significant portion of their overall demand or represents most of the process steps. It is better to pick a simpler process the first time Value Stream Mapping is attempted, increasing the complexity of processes to map as experience grows.
Build the Team
The members of the team are critical, as they will learn together and become supporters of the work going forward. The team should be diverse, comprised of people in the process, people who manage the process, customers of the process, and suppliers to the process. It can be beneficial to add a few team members who have no relationship with the process, as they provide “outsider” thinking and can challenge the team during the session.
Voice of the Customer
What is most important to the customer, from their point of view? Often, companies will engage Sales and/or Marketing to represent the customer, based on interactions they have had while dealing directly with customers. It is more powerful to invite direct customers to these sessions, but it can also be risky, as they will see some of the waste or inefficiencies in the current process. Most customers appreciate the opportunity to participate in these sessions, and the rewards far outweigh the risks.
Walk the Current State Value Stream
This is typically the most “eye-opening” part of Value Stream Mapping. The team should leave the meeting room and physically walk the process from the last step to the first. If they are mapping a physical product transformation, the team starts at the shipping dock, and then works their way back to the receiving dock. Start with the customer and what they are expecting to be delivered, then work your way back to the beginning of the process. All the while, the team is looking for waste and inefficiencies. They should be taking notes, pictures, and engaging with each other and others working in the process to fully understand what is going on and why things are working or not working as expected. If the process is virtual, the team should be demonstrating the steps of the process as they occur. Do not discuss the process in a meeting room. Go see what’s actually happening.
Gather data for the Current State Value Stream
How long does each process take? How many resources are needed for each step? How much inventory or waiting occurs at each step? How is information communicated to each step? How long does it take to change from one product or service to the next? How much space is required by each step? There is so much data that can be gathered, that you have to be careful not to do too much and miss the simplest and most impactful opportunities in the Current State.
Map the Current State Value Stream
Once the team returns to the meeting room, they map out all steps and interactions between steps of the process. This is a team activity, so don’t let just one person do all of the work. Each team member can take a pack of sticky notes and write down steps, placing them in order on a wall or something similar. Next, the team should measure the total time it takes for the product or service to get through the Value Stream, measuring the value-added time, non-value-added time, and lead time. Don’t use a computer, this is a visual activity, and most “A-ha” moments occur while placing steps on a wall and seeing how inefficient the current process is. Don’t be surprised if less than 10% of the time is value-added. In many manufacturing plants, that number drops below 1%. One key point is to map the process as it is, not how you want it to be.
Build the Future State Map
The team develops a vision of what they want the process to be in the future, for the benefit of the customer. By seeing the waste and inefficiencies in the Current State Map, the team imagines what the process would look like if they minimized or eliminated non-value-added steps, inefficiencies, defects, safety issues, and other waste in the current process. After the map is created, the team recalculates the value-added time, non-value-added time, and lead time in the future state. It is not unusual to drop the overall lead time to the customer by 50% or more. It’s also not unusual to identify quick, simple activities to accomplish this lead time reduction.
Create a Plan to Achieve the Future State
The team builds a roadmap of activities and strategies to make the changes required to drive to the Future State. These activities are typically low-cost and quick to implement, but some activities require an entirely new way of leading and managing the process. The team develops the action plan, with owners, due dates, and the managing systems to ensure that the work gets done.
A typical Value Stream mapping session takes between 3 and 4 days. When it’s over, everyone knows their new destination and how they intend to get there. Now, leadership has identified what is necessary to take the journey. Just like any journey, you must take the first step. Value Stream mapping is that first step.

Why Request a Site Assessment?
When you call Process Improvement Partners LLC for a site assessment, you are making a choice to invite outside perspective for your organization. While there is a fee for this service, there is also a significant investment of your time and resources, so it is good to understand the value of your investment.
When you call Process Improvement Partners LLC for a site assessment, you are making a choice to invite outside perspective for your organization. While there is a fee for this service, there is also a significant investment of your time and resources, so it is good to understand the value of your investment.
By the end of this 5 to 6-hour visit, you will have a greater understanding of where the highest value safety, quality, customer service, and cost opportunities are and how to leverage them. Here’s a typical site assessment agenda:
9:00 am - Team Introductions
A short review of each participant, their role, the company, and Process Improvement Partners LLC. We get to know one another and start the conversation on a personal and business level. It serves as a quick check of the team’s level of commitment, based on who is participating in the assessment and for how much time during the day.
9:15 am - Safety Review
How will we keep each other safe during the assessment? How important is safety to the site team and how strong is the safety culture of the company? During the visit, we will respect all of the safety requirements and expectations set by the team.
9:30 am - Review the Site Team Focus and Priorities
What are the priorities of the site team? What are the current pain points in their view? What do they want to focus on during the assessment? These discussions keep everyone aligned around the purpose of the assessment and make it more meaningful for all involved.
10:00 am - Plant Walk (Gemba Walk)
We walk the process with the site team, visiting all areas, speaking with people in the process, and looking for waste and inefficiencies. The more engagement we have with people in the process, the better. When waste is spotted, we stop and discuss what we see as a team. All team members are encouraged to take notes, so that they document what they see while on the walk.
11:30 am – Review of Findings
What did we observe on the plant walk? What did we learn from those in the process? Does it validate or invalidate our initial thinking? Did we learn something new, just by the way we engaged with others on the walk? Might this be an approach to incorporate into the way we do business moving forward?
12:00 pm - Lunch
Keeping the team together during lunch is critical. Although this seems like a minor detail, it’s an opportunity to relax and discuss things in a less formal way. It also lets the team get a feel for how an ongoing relationship with Process Improvement Partners LLC might look.
12:45 pm - Evaluate and Prioritize Opportunities
Based on everything we saw and discussed, what are the key things that the team wants to work on now and in the future? Using quick facilitation and prioritization techniques, the list of observations and ideas is narrowed to a top 5 to 10 that the team finds most important and impactful.
1:15 pm - Discuss Approaches to Leverage Top Priority Opportunities
We now discuss the tools and techniques available to drive improvement in the top priority opportunities. This is the time to decide whether the team wants to work on these opportunities without outside assistance, or with the help of Process Improvement Partners LLC. We will charter and write proposals for any work that the team feels it needs help with.
1:45 pm - Plan of Action
What are the next steps? Who is responsible? Does the team want Process Improvement Partners LLC to charter and write a proposal for the work? Is there a contact person for the work? We build an action plan that will be followed once the assessment is complete.
2:15 pm - Wrap Up and Feedback
An opportunity to review how the site assessment went for all participants. This is a learning moment for all involved, as we are applying process improvement in real time to the assessment process.
2:30 pm – Additional Time for Discussion or Adjourn
If the team wants more time to discuss the assessment, we always set aside additional time for them. If there is nothing left to discuss, the assessment is complete.
At the end of the site assessment, the team has a roadmap of activities that will help them improve their performance in safety, quality, customer service, and cost. In addition, they have had an opportunity to see how an ongoing relationship with Process Improvement Partners LLC can help them execute their roadmap.
How to Drive Teams to Success with Effective Facilitation
The best facilitators look like they’re doing nothing at all. The team is driving toward a solution, being creative, working together, and having fun. What’s the facilitator doing, just taking credit for the team’s hard work? As it turns out, the easier it looks, the harder it is.
The best facilitators look like they’re doing nothing at all. The team is driving toward a solution, being creative, working together, and having fun. What’s the facilitator doing, just taking credit for the team’s hard work? As it turns out, the easier it looks, the harder it is. But, if you use these techniques, you have a chance to look like you’re doing nothing, and doing it really well!
1. Stick to the charter.
This is the reason the team got together in the first place. Make sure all activities are conducted within the scope of the charter. It’s very easy to get off-track, or work on things that aren’t explicitly in the charter. The team should be reminded and guided back to the charter. An easy way to do this is to share a copy of the charter with every team member and have them read and discuss it at the appropriate time(s). They should be able to recognize if they are veering away from the charter.
2. The team solves the problem, the facilitator guides them to the solution.
Keep the roles separate, as the team will sometimes want the facilitator to give them the solution. This is not a good idea, as the team must own the solution and will not if they didn’t come up with it. The facilitator is responsible to come up with a solution path for the team, not the actual solution. There are times when a facilitator may have to provide direct help, but this should be rare, and only used as a last resort.
3. Everyone participates with an equal voice.
It’s very easy for some team members to dominate conversations, but in doing so, other team members may not have an opportunity to share their ideas. When this happens, there is no true consensus or full support for the solutions developed. Great care must be taken to give every team member an equal voice. One technique to do this is to give everyone a pack of sticky notes and let them write their ideas down, one per sticky note. Then, they share one idea at a time, one person at a time. Place each sticky note on a flip chart for everyone to see. Be careful not to let a team member share more than one idea before another team member gets a chance to share.
4. Keep the team moving.
I mean this both mentally and physically. If team members sit in one place too long or spend too much time on one topic, they will get bored, disengaged, and lose momentum. Get the team members out of their chairs, moving around the room, or out of the room. Break up activities into small chunks, so that there isn’t a chance for complacency or boredom. This tests the facilitator’s creativity, but it is vital for positive momentum and progress.
5. Time is precious. Break down barriers to progress.
Sometimes the team is looking for an answer and the expert is not in the room. A good facilitator will challenge the team to get the answer from someone else, in a different way, or by some quick estimate. In extreme cases, the facilitator will encourage the team to interrupt a meeting to get the answer they need. In even more extreme cases, the facilitator will get the answer for the team by interrupting a meeting or going to a higher-level leader for an answer.
6. The more ideas the better.
When a team is thinking up ideas and alternatives, their first ideas are typically things they are most comfortable with or don’t challenge them. Facilitators should drive the team to think of things that haven’t been tried before. The first step this is to ask team members for more ideas. Most people can come with 3 alternatives for almost anything. Ask for 7 in this case. If the team has stopped writing ideas, ask questions in as many different ways as possible, pulling more ideas out of the team. When we challenge ourselves, we are more often able to deliver breakthroughs.
7. Don’t let best get in the way of better.
We want teams to make improvements. Sometimes team members want things to be perfect before trying their solutions. The problem with this is that nothing is perfect and if we wait to have everything perfect, we will never test our improvement(s). So, the facilitator should encourage team members to try their ideas out before they are fully designed. It’s perfectly acceptable to make mistakes, as long as we learn from them and improve upon them. I tell teams to shoot for 60% confidence. It gives them more opportunities to try things quickly.
8. Use frequent check-ins of progress.
Once team members start working on their improvement projects, it’s easy to assume everything is going as planned and issues are addressed when they arise. However, that’s often far from the case. Team members often get stuck and struggle on their own until time runs out, if left to their own devices. Frequently connect with the team to check on their progress and determine any areas needed support. I have found that 1 ½ hours is about the maximum amount of time that team members should work independently before coming back together to share their progress. This is also a way to integrate efforts of different team members and eliminate duplication of efforts.
9. Teams that are having fun will accomplish more.
People like to win, laugh, have fun, and share in success. As a facilitator, you should be looking for ways to help the team win. Find activities that will make their time spent together engaging and fun. You may even need to develop team activities that help them work together better.
10. Less you, more them.
The reason the team was brought together was to solve a problem. If you had the answer to the problem, you wouldn’t need a team in the first place. A good facilitator will encourage as much participation from the team as possible by asking probing questions and creating a participatory atmosphere. Once the questions are asked, you must allow the team answer to them, not you. Often, they will want an answer from the facilitator, but you must resist the temptation. This is their effort, not the facilitator’s, so it’s best to let them struggle through hard questions.
These 10 facilitation techniques take practice, but they will help you get the best out of the teams you are working with. Take pride in knowing your teams solved their problems and it appeared you did nothing at all to help them!
How to Use Kaizen to Ensure Teams are Invested in Process Improvements
In 2005, I was helping a team improve the safety and productivity of their operating line. During a 4-day span, each of the team members was able to try and implement many different ideas that arose from their creativity.
In 2005, I was helping a team improve the safety and productivity of their operating line. During a 4-day span, each of the team members was able to try and implement many different ideas that arose from their creativity. At first, they didn’t believe that they would be allowed to make changes to the operating line, but after each successive attempt, they grew more and more confident, and the energy, enthusiasm and momentum grew. At the end of the 4 days, each of the team members reflected on their experience. One of the team members was a gruff mechanic who had been skeptical at the beginning of the session. He stood up with tears in his eyes and stated that this had been the most meaningful and impactful experience of his working life. I knew right then that I wanted to bring this joy to as many people as possible.
Kaizen brings people together to solve problems in their area of concern. They have the most understanding, experience, and vested interest in the effort. They also reap the benefits of the improvements moving forward. Kaizen asks us to make things better, not perfect, and go rapidly, without investing anything but the time and energy of the people making the changes. There may be some minimal cost, but because things are going so fast, a significant financial investment isn’t likely. Using the speed of Kaizen and the creativity of the team, I developed 3 approaches to drive the deep and emotional connection to improvement that I was seeking.
1. Idea Gathering and Sharing with Sticky Notes
Each team member takes a pad of sticky notes with them as they tour the area of concern. With guided questioning, the team members write down their personal observations or ideas that come to mind while touring. It is quick, personal, and drives ownership and accountability to come up with ideas for the benefit of the team and the people in the area. I ask each team member to write down one idea per sticky note, so that nothing gets missed and it’s easier to organize ideas as a team once we have reconvened. In the meeting room, I have the team members share all of their ideas, one person at a time, one idea at a time. Each idea is placed on a flip chart or on a wall for everyone to see. If there are 15 team members, I have each person share one idea until the team has heard 15 separate ideas. Then I give them a chance to share their second idea, third idea, and so on, until the team has run out of ideas. This creates an atmosphere where everyone has equal voice, regardless of position, experience, or pay grade.
2. Prioritization with Criteria
Once the ideas have all been shared and posted, the team may choose to group similar ideas together. This gives them the chance to see all of the ideas and remove any redundancy. Following this, each team member is asked to pick his or her top ideas using these criteria:
a. Provides the biggest benefit to our team and our customers
b. I personally want to do this
c. We can do this during the allotted time of the event
Everyone is given an equal number of votes (usually between 3 and 5), so no team member can dominate the conversation or the voting. These criteria are interpreted differently by each team member, but in the end, this approach creates a list of the team’s top priorities. This approach generally takes no more than 10 – 15 minutes.
3. Pick Your Project
We now have a list of things to work on, prioritized by the amount of votes the team has placed on them. I then list the top 3 or 4 projects on a flip chart, depending on the size of the team. Now it becomes personal, as I tell the team, “First come, first served. Place your name on the project you want to work on.” More than a few times, team members rush to the flip chart to put their names on a project. They want to ensure they get the project that matters to them the most. This may sound risky, as a project may not get claimed. I have never seen this happen. Team members have different interests and you can’t always guess what they are, so I have stopped doing that. Also, if there aren’t enough team members on a project, I ask if there’s anyone willing to swap projects. Often, there are a few team members who don’t have a real preference, so they are happy to change projects.
Now that we have personally observed and shared issues, picked our projects, and assigned the work to the people who want to do it the most, we have the foundation for the deep personal connection to the improvements that we seek. Sometimes a team member will find it moving enough to convince others to get involved in future efforts and find the same joy that they did.